
Mold DFM Reports: What a Professional Report Must Contain
Table of Contents
A mold is the last place you want to discover a defect. A sink mark that shows up at first trials means the cavity gets re-cut, polished, and re-tested. That typically adds 1-2 weeks to the schedule. A flash problem on hardened steel can force a weld repair that risks the whole tool. Both failures start the same way: a geometry issue no one flagged before steel was cut.
DFM stands for design for manufacturability. In mold making, it is a structured review of your part against the mold that will produce it. A professional report lists every risk with a number: a wall thickness, a shrinkage value, a tolerance, a cost. A template report repeats the same sentences for every part it sees.
This article walks through every section a professional DFM report must contain. It covers what each section should say about your part, and how to tell analysis from boilerplate. DieStrike runs 120+ machines under IATF 16949 and ISO 9001. We hold ±0.005 mm as standard and ±0.002 mm on precision tools. Our DFM reports go back within 1-3 days, typical, before any mold steel is ordered.
The Snapshot
- Wall thickness targets: 1.5-3 mm typical; below 0.8 mm risks short shots, above 4 mm risks sink and long cycles.
- Shrinkage compensation: 0.3-2.5% typical by material; the report must state the exact value used for cavity sizing.
- Tolerance capability: ±0.005 mm standard and ±0.002 mm precision at DieStrike.
- DFM turnaround: 1-3 days, typical, delivered before any mold steel is ordered.
- Changes at the DFM stage cost roughly 5-10x less than the same change after steel is cut, typical.
What a Professional DFM Report Covers
A DFM report is a pre-production engineering document. It sits between your quote request and the moment mold steel is ordered. Its job is to put every manufacturability issue on the table while changes are still cheap.
The table below shows the six core sections. Each one answers a specific question about your part and your mold.
| Section | What It Contains | Why It Matters |
|---|---|---|
| Part review | Wall thickness, draft angles, ribs, bosses, undercuts | Catches geometry that will not fill, eject, or cool evenly |
| Material assessment | Shrinkage, flow length, gate feasibility | Sets cavity compensation and gate position |
| Mold construction proposal | Cavity count, parting line, gate, ejection, cooling | Defines how the mold is built and how it runs |
| Risk register | Warp, sink, flash, weld line, short shot with likelihood | Puts every defect on the table before steel is cut |
| Tolerance feasibility | Critical dimensions vs mold capability | Separates achievable tolerances from expensive ones |
| Cost and lead time | Estimate with stated assumptions | Links every engineering decision to money and schedule |
← swipe to scroll →
Every section must end with a conclusion the customer can act on. A wall review that says "wall thickness is acceptable" is useless. It must say "the 2.8 mm wall at the boss base is 0.3 mm over the 2.5 mm target , expect a sink mark unless we add a core pin." Specific numbers are the whole point.
Part Geometry Review: Walls, Draft, Ribs, Bosses
Geometry review is the first and heaviest section of a DFM report. The reviewer checks every wall, rib, boss, and undercut against the material and the molding process. Most manufacturability problems live in four features.
Wall Thickness
Uniform walls are the foundation of a moldable part. The typical target band is 1.5-3 mm. Below 0.8 mm, thin-wall short shots and packing problems start. Above 4 mm, sink marks and long cooling times start. Both ends cost money: one in scrap, the other in cycle time.
The report should state your actual wall values, not just the target. If your part runs 2.8 mm nominal with a 5 mm pad under a boss, the report must flag the pad. If walls vary by more than roughly 25% across the part, expect a recommendation for a transition or a redesign.
Wall thickness also sets the cooling time. Cooling time scales with thickness squared. A 3 mm wall takes about 4x longer to cool than a 1.5 mm wall at the same mold temperature, typical. The report should connect wall thickness to your cycle time, not just to fill.
Draft Angles
Every surface parallel to the pull direction needs draft. The typical band is 0.5-2° per side. Textured surfaces need more, about 1° per 0.025 mm of texture depth as a common rule of thumb. Ribs and bosses need a minimum of 0.5-1°.
Zero draft means the ejector system drags the part out of the cavity. That leaves ejector witness marks, scratched surfaces, or a part that sticks and bends. A DFM report lists every zero-draft face and the angle it recommends.
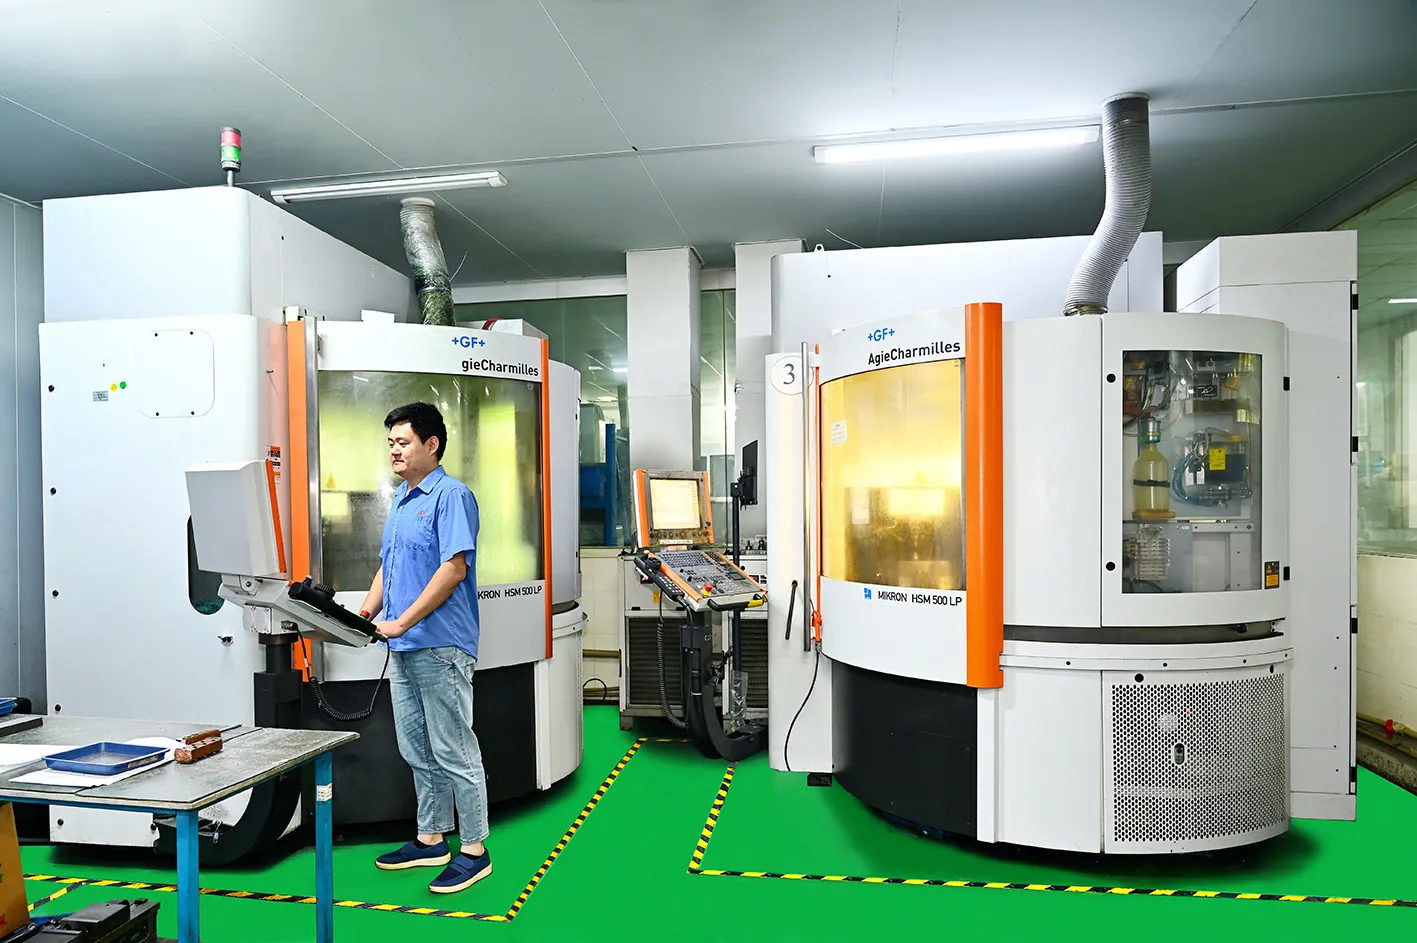
Draft is machined or EDM'd into the cavity steel, not added later. A high-speed CNC finish holds the angle across the whole cavity, which is what makes a clean release possible.
Ribs and Bosses
Ribs stiffen a wall without thickening it. The standard rule is a rib base of 0.5-0.6x the nominal wall. A boss that carries a screw or press-fit holds the same 0.5-0.6x ratio on its outside diameter. Add gussets when the boss is tall.
Undercuts need side actions. Each slider or lifter typically adds 15-25% to mold cost and slows the cycle. The report should list every undercut and propose the action, or a redesign that removes it.
Material Assessment: Shrinkage, Flow, and Gate Feasibility
The material section connects your resin choice to the mold geometry. Three numbers matter most: shrinkage, flow length, and gate position.
Shrinkage and Cavity Compensation
Every plastic shrinks as it cools. Typical shrinkage runs 0.3-2.5% depending on the grade: PP around 1.5-2.5%, ABS around 0.4-0.7%, PC around 0.5-0.7%, POM around 2%. The report must state the exact value used, because the cavity is cut to compensated dimensions.
A wrong shrinkage assumption shifts every dimension on every part. If the mold is cut for 0.6% and the resin shrinks 0.9%, a 100 mm feature comes out 0.3 mm undersize. The DFM report locks the shrinkage value in writing before steel is cut.
Flow Length and Gate Feasibility
Flow length is the distance molten resin travels from gate to last fill point. The ratio of flow length to wall thickness (L/t) has practical limits per material. PC is typically limited around 150:1, PP around 300:1. Exceed the ratio and the part short-shots or packs unevenly.
Gate feasibility covers position and type. A gate near a critical cosmetic surface leaves a vestige. A gate that fills from one side can trap weld lines in a structural area. The report proposes gate type , edge, pinpoint, submarine, or hot runner , and location, and explains the trade-off in your terms.
Gate vestige is part of the spec. A submarine gate typically leaves a 0.3-0.5 mm stub, a pinpoint gate a small dimple, and a hot runner a clean surface with no trimming. The report should state the vestige you will get, because it decides whether the gate area needs post-processing.
Mold Construction Proposal
This section describes the mold itself: cavity count, parting line, gating, ejection, steel, and cooling. Every choice sets a cost and a cycle time.
Cavity Count
Cavity count is driven by annual volume and target cycle time. The math is simple: 500,000 parts per year at a 30-second cycle needs about 4,200 hours of molding time. One cavity at 6,000 available hours handles it. Double the volume, and two cavities start to make sense.
The report should show the calculation, not just the answer. If it recommends 2 cavities, it should also show the cycle time, the machine size, and the cost per part at 1 vs 2 cavities.
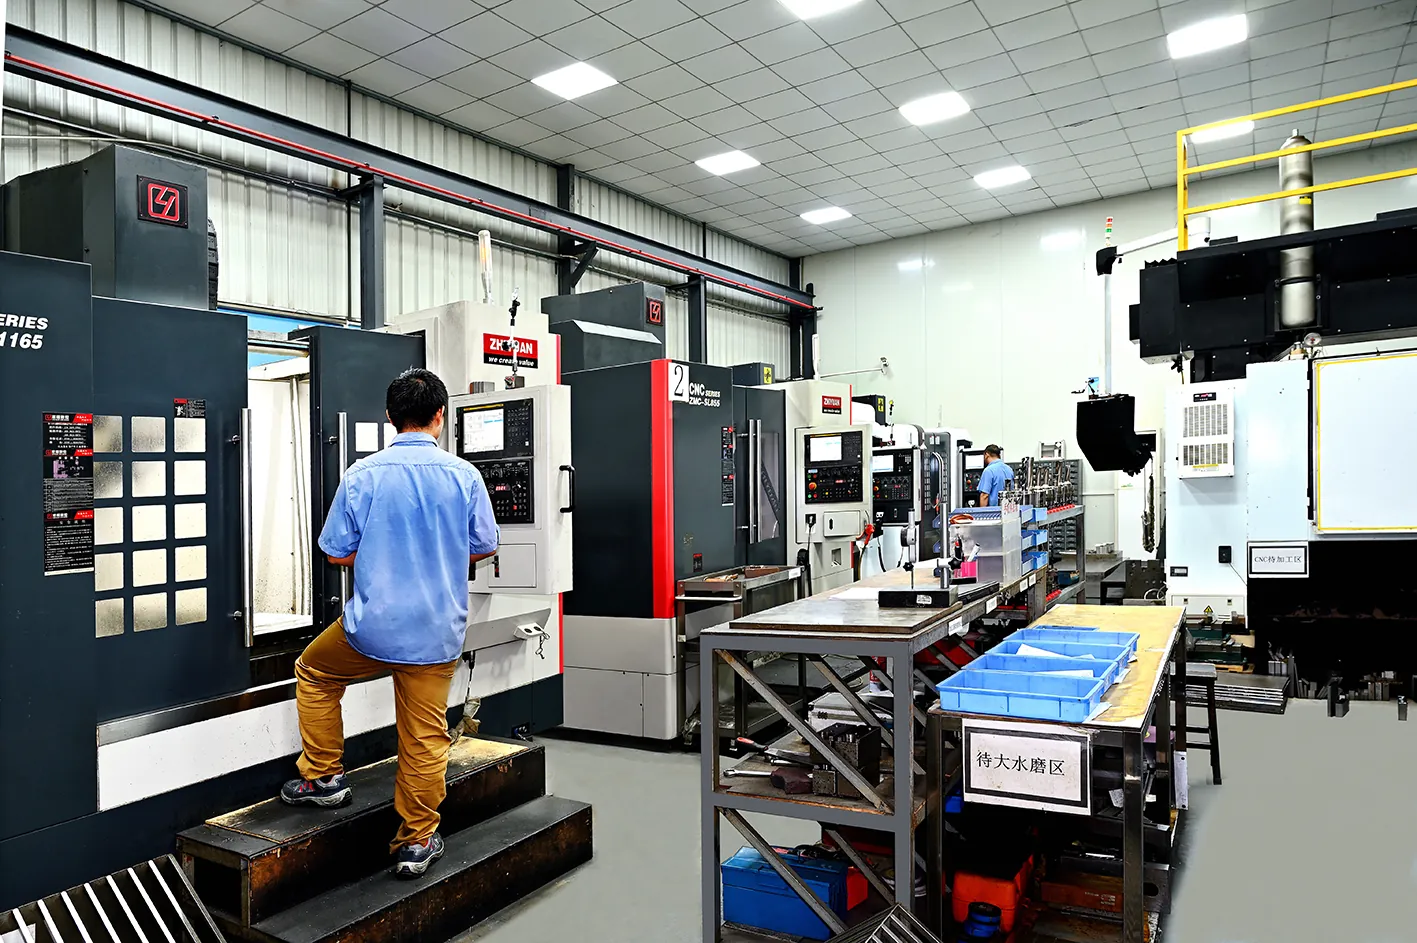
A machining center cuts the cavity block to the compensated geometry. The same block then goes through finishing, EDM if needed, polishing, and inspection before assembly.
Parting Line and Gate Strategy
The parting line decides where flash can appear and how the part looks at the seam. A line placed on a visible edge hides flash. A line through a functional surface does not. The report should mark the parting line on your part and justify the position.
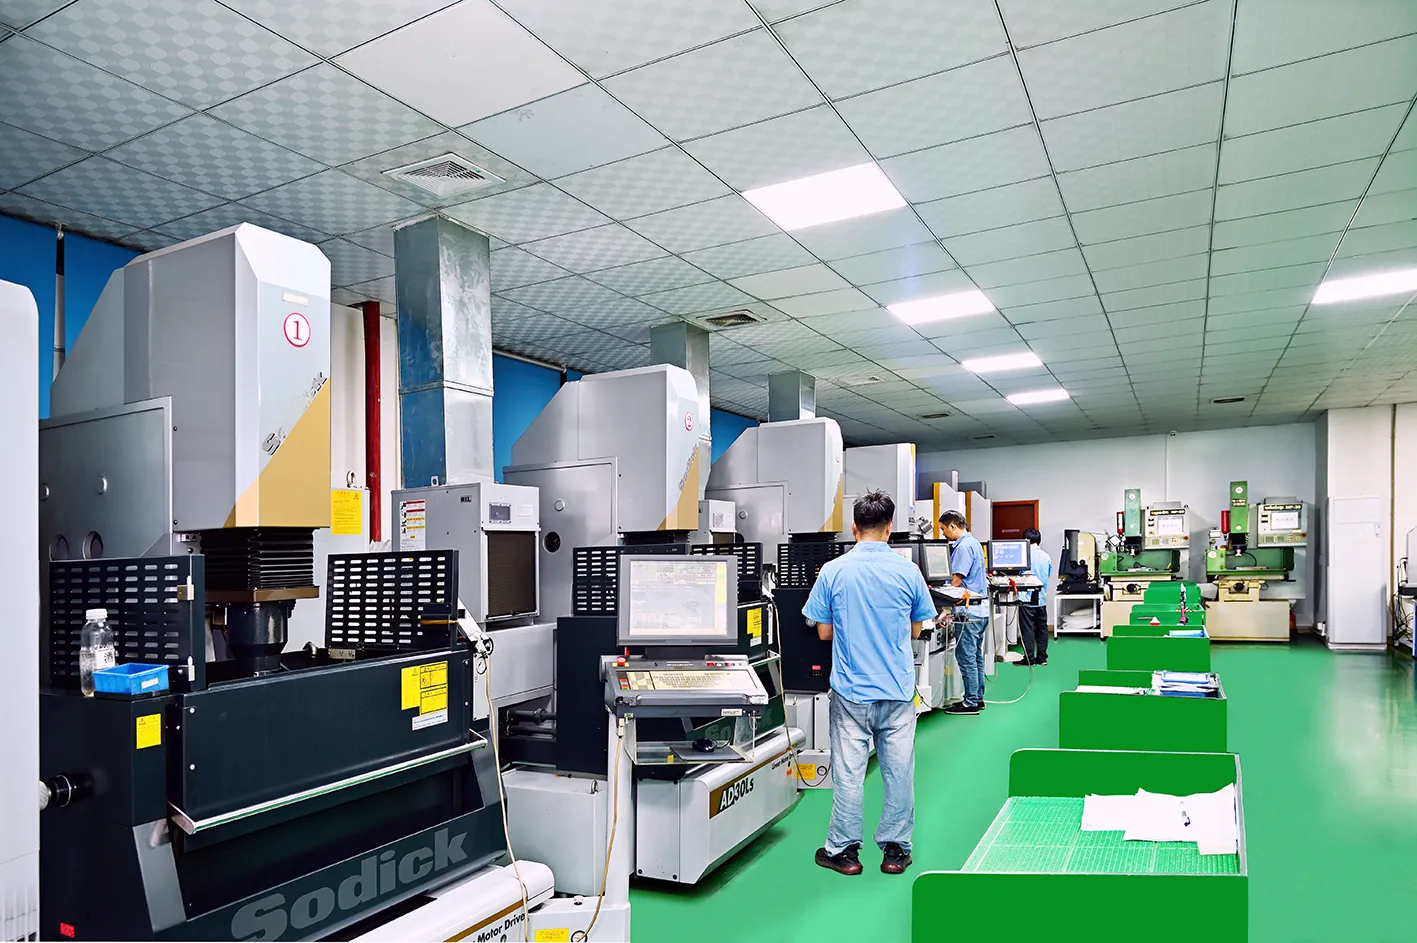
Gate position follows from the flow analysis and the parting line. Complex gate details are often EDM'd: wire for through-features, sinker for blind detail. The report states which method and why.
Ejection Strategy
Every part needs a way out of the mold. The report lists ejector pins, sleeves, lifters, or stripper plates, with positions sized to the part. Pins too few or too small leave witness marks. Pins too close to thin walls can pierce them.
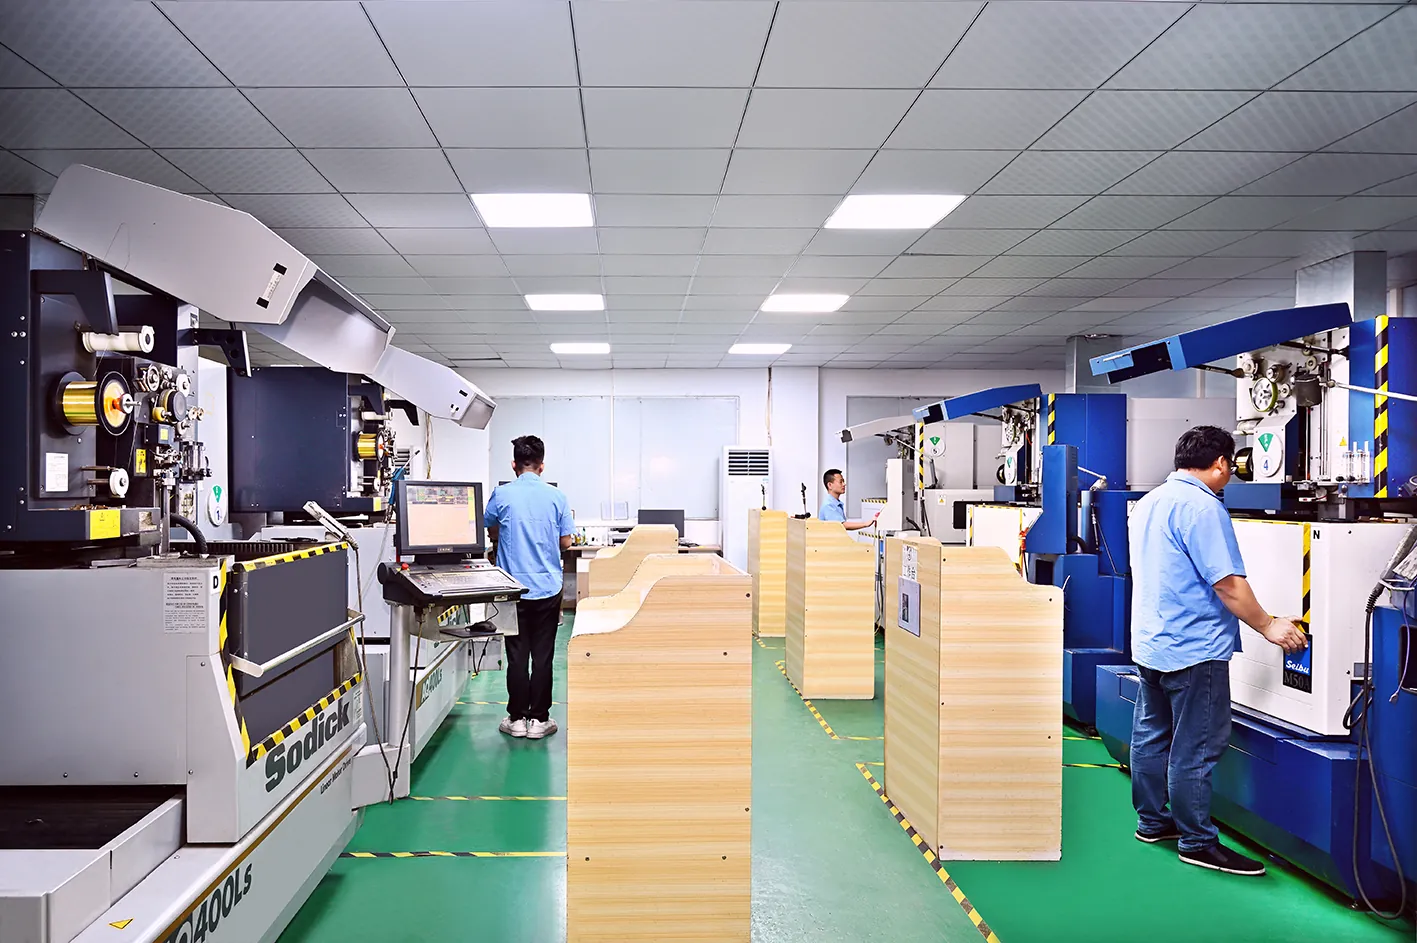
Ejector holes and inserts are cut by wire EDM for straightness and positional accuracy. A clean ejector system is what keeps a thin-wall part from sticking.
Steel Selection and Hardness
Steel choice follows from volume and material. Pre-hardened P20 around HRC 30 handles low-volume prototyping. High-wear resins like glass-filled nylon or POM need harder tooling. DieStrike hardens tools to HRC 62 where wear is the risk and verifies hardness on every block.
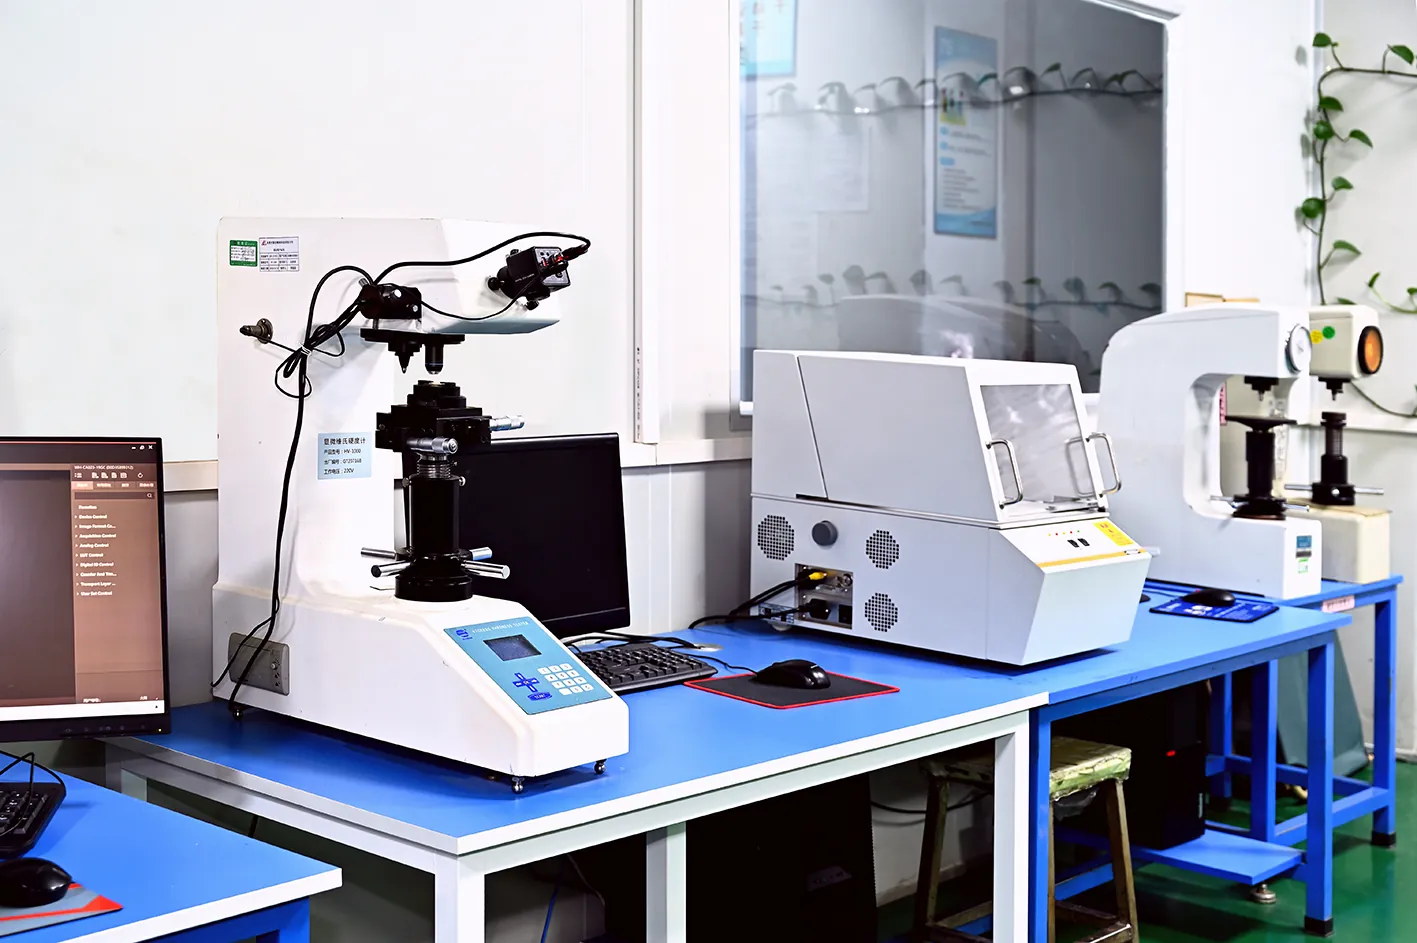
Hardness is verified with a vickers test on a film gauge, and the value is recorded in the mold record. A number on paper beats a claim in an email.
Cooling Plan
Cooling drives cycle time, typically 50-70% of the molding cycle. The report should show cooling line layout, spacing, and distance from the cavity surface. A common design rule is spacing and distance at 2-3x the line diameter, with 16-20°C water temperature control as a starting point.
Straight drilled lines handle most tools. Conformal cooling follows the cavity contour and cuts cycle time on deep or complex geometries, typical 10-20% on the right part. It also adds cost and lead time, so the report should say which you get and what it costs.
The report should say where the lines run, not just that "cooling is optimized." If a thick boss has no cooling near it, expect sink. The report should already have flagged that.
The Risk Register: Five Defects with Likelihood and Mitigation
Every mold has risks. The professional report lists them in a register with three fields: likelihood (high, medium, low), trigger, and mitigation. Five defects cover most injection-molded parts.
Warp
Cause: uneven cooling or non-uniform wall thickness. Likelihood: medium for most flat panels, high for thin walls with long flow. Mitigation: balanced cooling, uniform walls, gate placed for symmetric fill. Verification: CMM check on the first shot.
Sink Marks
Cause: thick sections shrinking away from the cavity wall. Likelihood: high wherever wall exceeds 4 mm, typical. Mitigation: replace thick walls with ribs, gate near the boss, cooling under the feature. Verification: visual check and wall-section measurement.
Flash
Cause: parting line mismatch, insufficient clamp tonnage, or soft steel at the parting line. Likelihood: low on a well-fit mold, higher on hardened tools with thin edges. Mitigation: correct parting line design, adequate venting, HRC 62 at wear surfaces. Verification: trial shots at full tonnage.
Weld Lines
Cause: two flow fronts meeting and freezing. Likelihood: high around holes and bosses, typical for most multi-gate parts. Mitigation: gate position moves the weld line to a non-critical area, flow leaders, higher melt temperature. Verification: molded samples and strength testing if structural.
Short Shots
Cause: thin walls, long flow, or low injection pressure. Likelihood: medium on parts with 0.8 mm walls, typical. Mitigation: wall review, larger gate, adequate venting. Verification: fill study on the first shot.
If a risk lands on the register with "monitor during trials" and no mitigation, treat it as unfunded. Every risk needs a number, a trigger, and a response. Likelihood is a judgment, not a prediction. What matters is that every defect has a named trigger and a named mitigation. If the register is empty, the reviewer did not look hard enough , every mold has at least one risk worth writing down.
Tolerance Feasibility: What the Mold Can Actually Hold
Every print lists tolerances. The DFM report separates the ones the mold can hold from the ones that will fight you.
Critical Dimensions and Mold Capability
DieStrike holds ±0.005 mm as standard and ±0.002 mm on precision tools. Those numbers are the mold's capability, not a promise on every dimension. Shrinkage variation, packing, and cooling add part-to-part spread on top of the cavity's accuracy.
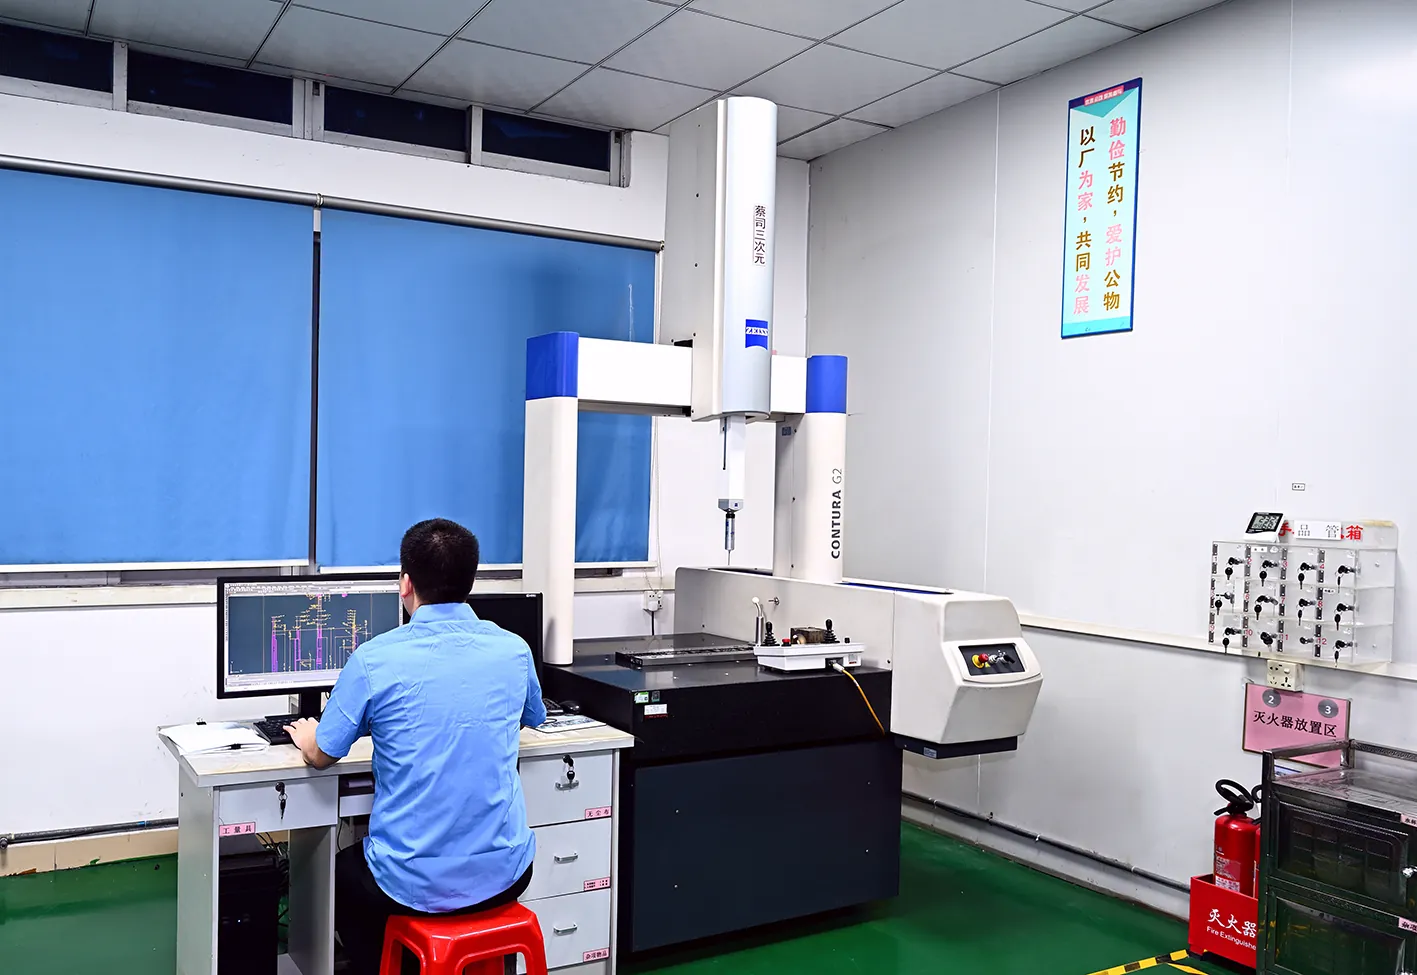
Every critical dimension gets a verification plan. CMM measurement on the first shot and at agreed intervals keeps the capability honest. If your print calls for ±0.001 mm on a 50 mm boss, the report should say so plainly. That is beyond what a molding process holds, typical, and it needs a design change or a secondary operation.
Part tolerance is not cavity tolerance. The cavity holds its dimension, then shrinkage and process spread add their own variation. A practical rule of thumb: part-to-part spread adds roughly 0.05-0.1% of the dimension on top of cavity accuracy, typical. The report should tell you which number applies to your critical dimensions.
Where to Relax Tolerances
Mating features, press-fit diameters, and datum structure deserve tight tolerances. Cosmetic radii, free surfaces, and hidden walls do not. A good report marks the datum scheme and tells you which dimensions are cheap to hold and which are expensive.
Every tolerance you tighten adds cost. A report that quotes the same ±0.02 mm everywhere is a report that has not looked at your part.
Cost and Lead Time Estimate with Assumptions
The engineering sections feed the money section. Every cost line should trace back to a decision in the DFM: cavity count, steel grade, hot runner vs cold runner, side actions, surface finish.
What Assumptions Drive the Estimate
The report must state its assumptions in writing: annual volume, target cycle, machine size, steel grade, and finish class. Change an assumption and the number changes. A quote without stated assumptions is a guess with a letterhead.
Read the cost section against the mold quote itself , they should tell the same story. The guide to reading a mold quote covers the line items to verify.
Typical Numbers
DieStrike production molds ship in 2-5 weeks; standard parts go out in 3-7 days. Those windows hold when the DFM is approved without a long iteration loop. Every change request after steel is cut adds days, typical: a re-cut, a new insert, or a re-polish each carries its own lead time.
The estimate should also name the biggest cost driver on your specific tool. Sometimes it is steel, sometimes EDM hours, sometimes a hot runner system. Naming it lets you decide where to negotiate.
Questions Back to You: The Missing Information List
A professional DFM report ends with questions. If yours returns zero questions, someone did not read your part. The report is only as good as its inputs, and most inputs are missing at quote time.
Typical questions include annual volume, target cycle time, exact material grade and supplier, finish class, and functional tolerances. Others: inserts, overmolding, target mold life, sampling and PPAP dates. Each maps to a decision in the report.
Answer them before steel is ordered. A volume answer that doubles after the mold is cut means a cavity count that was wrong from the start.
Answer speed matters too. A quote that waits on your answers has a clock running: steel prices, machine time, and your sampling date all move. Once you confirm the missing list, DieStrike locks the DFM assumptions and the 2-5 week production mold clock starts, typical.
What Separates a Good DFM Report from a Template
Template reports are easy to spot. They use the same wall-thickness sentence for every part. They never name your material's shrinkage. They never ask a question. They close with "we look forward to working with you."
A good report is specific at the feature level. It says your 2.8 mm wall at the boss base exceeds the 2.5 mm target for PC/ABS. It says your ABS grade shrinks 0.6%, so the 100 mm dimension gets a 100.6 mm cavity. It flags your 5 mm boss and proposes a gusset.
Specific numbers are the difference between analysis and decoration. Boilerplate costs money later. Every issue it misses lands in the mold shop, where the same change costs 5-10x what it cost on the CAD screen, typical.
How DFM Fits the Quoting Process
The quoting process has five steps: quote request, DFM review, report, iteration, and purchase order. The DFM sits second, before any commitment. That ordering is what makes it cheap.
At DieStrike the DFM review runs as part of the quoting workflow. A mold design and DFM service review lands within 1-3 days of the request, typical, and the report drives the quote. The quote and the report reference each other, so the numbers reconcile.
Plan for two to three revision rounds, typical, before the report is signed. Each round tightens the numbers: cavity count, steel grade, gate position. That is the process working , a report that never changes is a report that was never read.
If a supplier quotes without a DFM, ask why. The report is the only document that proves the supplier looked at your part before pricing it.
FAQ
What is a DFM report in mold making?
A DFM report reviews your part against the mold that will produce it. It covers geometry, material, mold construction, risks, tolerances, and cost. It returns within 1-3 days, typical, before steel is ordered.
How long does a DFM report take?
One to three days is typical for a standard injection-molded part. Complex parts with side actions, inserts, or tight tolerances take longer, and the supplier should say so at the start.
Is the DFM report included in the quote?
Most production mold builders run the DFM review during quoting, DieStrike included. Ask whether the report is included before you pay, and get the report before you commit to the mold.
What if my part fails the DFM review?
Failing is normal , most parts need at least one change. The report tells you what to change and why. Early changes are cheap: a CAD edit before steel is cut costs hours, while a re-cut after first trials costs days and steel.
What tolerances can a mold hold?
DieStrike holds ±0.005 mm standard and ±0.002 mm precision. Tighter tolerances are possible only with tighter process control, a measurement plan, and usually a higher price. The report should tell you which of your dimensions are realistic.
Should I get a DFM report before ordering the mold?
Yes. The report is the cheapest inspection your part will ever get. It protects both sides: you know what you are buying, and the builder knows what they are building.
The Bottom Line
A DFM report is a risk document with numbers attached. It exists to find defects while they cost hours, not weeks. When it is specific , your walls, your shrinkage, your tolerances , the mold gets built right the first time. When it is vague, the mold gets fixed in the shop.
When it is boilerplate, it is a liability. Every sentence that applies to any part applies to no part.
Ask your supplier for the report before steel is ordered. Read it against a DFM checklist and verify every number. DieStrike is IATF 16949 and ISO 9001 certified, runs 120+ machines, and builds production molds for customers including TE, Amphenol, Luxshare, and Dongshan. We hold ±0.005 mm standard and ±0.002 mm precision, harden tooling to HRC 62, and ship production molds in 2-5 weeks. The report comes first, and it comes with numbers.
NEXT STEP
Ready to Start Your Mold?
Send us your element dimensions or part numbers — our team responds within 24 hours with pricing and lead time.

Written by
Ray ChanMold Buyer's Guide Author · Precision Mold Manufacturing Specialist. Ray helps global importers, distributors and OEMs source factory-direct molds and mold parts.