
How to Balance Multi-Cavity Molds: Runner, Gate and Cooling
Table of Contents
A 16-cavity mold that fills unevenly does not fail one part at a time. It fails by the bank. The cavities nearest the sprue fill first, overpack, and flash. The far cavities hesitate, freeze early, and short-shot. One bad cavity wastes 1/16 of every shot.
The arithmetic compounds fast. A 200,000-piece program on that tool discards about 12,500 parts at that loss rate. Sorting catches some of them. The rest reach the customer and come back as a claim. Then the press stops for the fix, and the downtime bill starts.
Balance is the rule that prevents this sequence. In a balanced mold, every cavity fills at the same pressure, packs at the same density, and cools at the same rate. Parts from cavity 1 and cavity 16 weigh the same and measure the same. Imbalance breaks the rule in three visible ways: short shots, flash, and dimensional drift.
Cavity counts of 8, 16, 32, and 64 push unit cost down, then multiply the balance problem. Runner length, gate size, and cooling circuits all scale with cavity count. Design each one by habit and the tool fails at first trial. Design them as one system and a multi-cavity mold runs millions of cycles.
The Snapshot
- 2–3% typical maximum shot-weight spread across cavities. Above it, the light cavities short-shot at volume.
- ±3–5 °C typical coolant differential across cavities. Uneven cooling moves dimensions shot to shot.
- ±0.01 mm typical cavity-to-cavity dimension spread at the CMM. Machining holds it; filling and cooling keep it.
- 8/16/32/64 cavity counts. Each doubling halves the per-part tooling cost and doubles the balance work.
- 0.5–1.0 mm typical gate land with ±0.01 mm gate depth tolerance. Identical gates keep fill identical cavity to cavity.
Why Cavity Balance Matters
Multi-cavity molds exist for one reason: economics. A 16-cavity tool makes 16 parts per cycle for roughly the press time of one. The per-part share of mold cost, press rate, and overhead all drop as cavities multiply. That math only works if the parts are interchangeable.
Imbalance breaks interchangeability. Filling follows flow resistance, so the cavities closest to the sprue fill first. The far cavities fill last, after the melt has cooled and the pressure has dropped. Near cavities pack harder and flash. Far cavities pack lighter and shrink differently.
The costs are measurable. A 1% scrap rate on a million-part program is 10,000 parts. A 16-cavity mold on a 25-second cycle typical produces about 18,400 parts per shift. Losing 2% of that to short shots and flash is about 370 parts per shift, most of it found at sorting.
Downtime is the second bill. A balance fix means a runner or gate rework, a mold pull, and a re-trial. A 16-cavity tool pull and rework runs one to three days typical. A press at $80-150 per hour typical sits idle the whole time. The rework also adds days to the delivery schedule.
The third cost is dimensional. Cavities that pack at different pressures shrink differently. On a part with 0.4% shrinkage typical, a 20% pack pressure difference between banks can move molded dimensions past a ±0.05 mm print tolerance. Parts that pass alone fail in a set.
Natural vs Artificial Runner Balance
Runner balance comes in two flavors. Natural balance means every cavity sees the same flow length from the sprue or manifold drop to its gate. The runner mirrors itself across the tool. Pressure drop is identical cavity to cavity by geometry, not by tuning.
Artificial balance means the flow lengths differ and the designer compensates. The fixes are flow restrictors, smaller runner sections, or valve gates. Artificial balance works, but it depends on the resin and the process. Change the melt temperature or the fill rate and an artificially balanced runner drifts out of balance.
Natural balance is the starting point for every 8, 16, 32, or 64-cavity tool. An 8-cavity mold takes an H-pattern or X-pattern runner with equal flow length to all eight gates. Sixteen cavities take a symmetric layout from a central sprue. Thirty-two and sixty-four cavities typically run hot-runner manifolds sized for equal pressure drop to every drop.
When natural balance is impossible, the fix order is fixed: move the gates, then resize runner sections, then restrict flow, then add a valve gate. Each step adds complexity and process sensitivity. The resin datasheet and a mold flow analysis decide where the tool lands in that order.
Runner Sizing for 8-64 Cavities
Runner sizing follows a progression from sprue to gate. The sprue feeds a primary runner. The primary splits into secondaries. Each secondary feeds one gate or a pair of gates. Every step drops in diameter because the flow splits.
The working ratios are simple. The sprue at the parting line is typically 1.5-2.0x the primary runner diameter. A secondary runner is typically 70-80% of the primary. A tertiary is typically 70-80% of the secondary. These ratios keep pressure drop low and the runner cool in cycle.
Cross-section matters as much as diameter. Trapezoidal runner cross-sections are standard because they eject cleanly and pack less material than a full round channel. A trapezoid is cut in one half, so it needs no parting-line split and cannot flash at the seam. The depth-to-width ratio runs about 0.8 typical.
Runner Diameter Progression
On an 8-cavity cold runner, the H layout splits the sprue into two arms and each arm feeds four cavities. The X layout feeds eight cavities from a central sprue. Either way, every gate sits the same flow length from the sprue. Runner diameters follow the progression above: sprue, primary, secondary, gate.
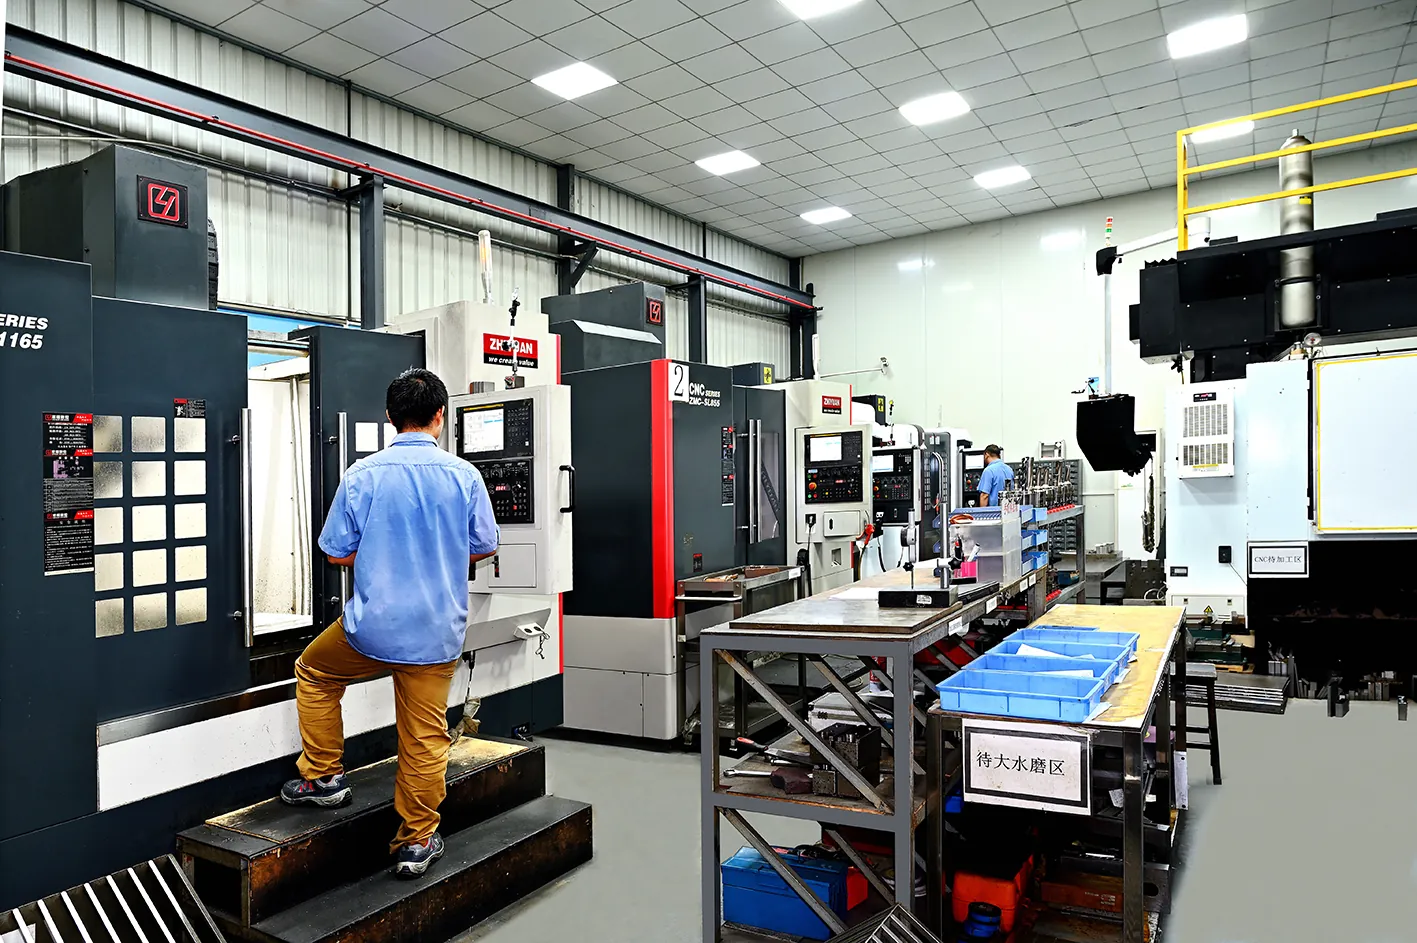
Cut runner channels to a surface finish of Ra 0.8 µm typical or better. Rough walls add pressure drop that differs cavity to cavity as the steel wears. A polished, symmetric runner network is the cheapest balance insurance in the tool. DieStrike machines runner channels on CNC machining centers to ±0.005 mm standard.
The cold runner carries a scrap cost that grows with cavity count. A 16-cavity cold runner can carry 10-20% of the shot weight typical as runner. That runner is regrind on many resins but restricted on flame-retardant and high-temperature grades. At 32 and 64 cavities, the runner economics usually push the design to a hot runner.
Gate Balancing Across Cavities
The gate is the last flow control before the cavity and the most sensitive. Every gate must pass the same flow rate at the same pressure. Gate depth, width, and land length are cut identically cavity to cavity. They are held there through the life of the tool.
Gate size follows the cavity position in the runner network. A naturally balanced runner starts with identical gates. An artificially balanced runner cuts near gates smaller and far gates larger. Mold flow analysis sets the starting sizes, and the trial refines them.
Gate depth is the primary lever. A 0.05 mm change in gate depth typical shifts fill time and pack pressure measurably. Gate depth tolerance of ±0.01 mm typical is achievable with EDM or precision milling. It is the difference between balanced and drifting fill.
Gate Size and Land Adjustments
Gate land is the straight section after the gate opening. Keep the land short, 0.5-1.0 mm typical. A long land adds pressure drop and makes the gate sensitive to wear. Air-gauge the gates at buyoff and record the numbers.
Gate adjustment is a measured process, not a guess. When trial shot weights show the far cavities running light, deepen the far gates in 0.02-0.05 mm typical steps. Re-trial and re-weigh after each step. Change one variable at a time, or the data is worthless.
The gate is the first place wear shows. Abrasive glass-filled resins open the gate over time, and an opened gate flows more resin into that cavity. Hardened gate and cavity steel resists the wear. DieStrike runs cavity steel up to HRC 62 when the program demands it. Gate dimensions belong on the periodic inspection list.
For the full gate design playbook, see our 7 gate design best practices.
Mold Flow Analysis Before Steel
Mold flow analysis is where balance is proven or killed before steel is cut. The simulation runs the actual part geometry, the resin datasheet, and the runner and gate layout. It reports fill pattern, pressure drop, weld lines, and cooling. A 32-cavity tool with a bad runner shows the problem in the first fill-time plot.
Read the report for four numbers. Fill time per cavity: all cavities should match within a few percent typical. Pressure at end of fill: the spread across cavities should stay under 10% typical. Weld line position: lines should sit where the print allows them. Pressure drop through the runner: high drop means the runner is undersized.
The analysis also finds hesitation. Thin walls, long flow paths, and sharp transitions show up as regions where the flow front stops. On a multi-cavity tool, hesitation in one cavity is a balance failure in the making. The resin that hesitates in cavity 12 is also flowing differently in cavity 4.
Weld lines deserve their own check. Every multi-cavity mold creates weld lines where flow fronts meet. Glass-filled resins weaken at weld lines. If a weld line lands in a structurally critical spot, move the gate or add a vent before cutting steel. An analysis costs days on the schedule; a cavity rework costs weeks.
Cooling Balance Across Cavities
Cooling decides dimensional consistency, cycle time, and shrinkage. A cavity bank that runs 4 °C hotter than its neighbor molds a different part every shot. Cooling balance means every cavity sees the same mold temperature through the whole cycle.
The target is a coolant temperature differential of ±3-5 °C typical across the tool. Hold it with equal waterline layouts and equal circuit lengths. Series circuits are the classic failure: coolant enters at 40 °C and exits the last cavity at 48 °C. The last cavity runs hot for its entire life.
Waterline geometry follows the same ratios on every cavity. Standard waterlines run 8-12 mm diameter typical. Space them 2-2.5x the hole diameter apart. Keep them 2-3x the hole diameter from the cavity wall. Deviate and the hot spots appear at the end of each circuit.
Cooling Channel Layout
Deep-hole drilling and precision machining place the cooling channels. Channel position tolerance matters. A waterline that drifts 1 mm toward the cavity surface cools that spot faster and warps the part. DieStrike drills and machines cooling channels to the same ±0.005 mm standard as the cavity work.
Core cooling is the hard part. Cores carry the most steel per part and the least access for waterlines. Below 6 mm core diameter typical, a straight waterline cannot fit. The core cools by conduction into the core plate, so the plate must be waterline-backed. Bubblers, baffles, and heat pipes cover the cores above that size.
Mold temperature control completes the loop. A temperature controller with ±1 °C stability typical on each circuit holds the cavity bank uniform. Log the circuit temperatures at buyoff. When dimensional drift appears later, check the circuits first. For the full cooling rule set, see our 5 mold cooling channel design tips.
Cavity-to-Cavity Dimensional Consistency
Balance only matters if the parts measure the same. Cavity-to-cavity consistency is verified with measurement, not a visual check. The target spread across cavities is ±0.01 mm typical on critical dimensions. Verification happens at tool buyoff and periodically in production.
Machining sets the floor. If the cavities are cut differently, no process window fixes it. DieStrike machines cavity details to ±0.005 mm standard and ±0.002 mm on precision features, with wire EDM for the tightest work. A 32-cavity tool is one build: same programs, same inserts, same tolerance chain.
Verifying Cavity Dimensions
The CMM is the arbiter. Every cavity is measured on the same program and the results are compared cavity to cavity. The report shows the spread, not just the average. A ±0.01 mm spread typical across 32 cavities means the cavities were cut as one system. A 0.05 mm spread means the machining plan drifted.
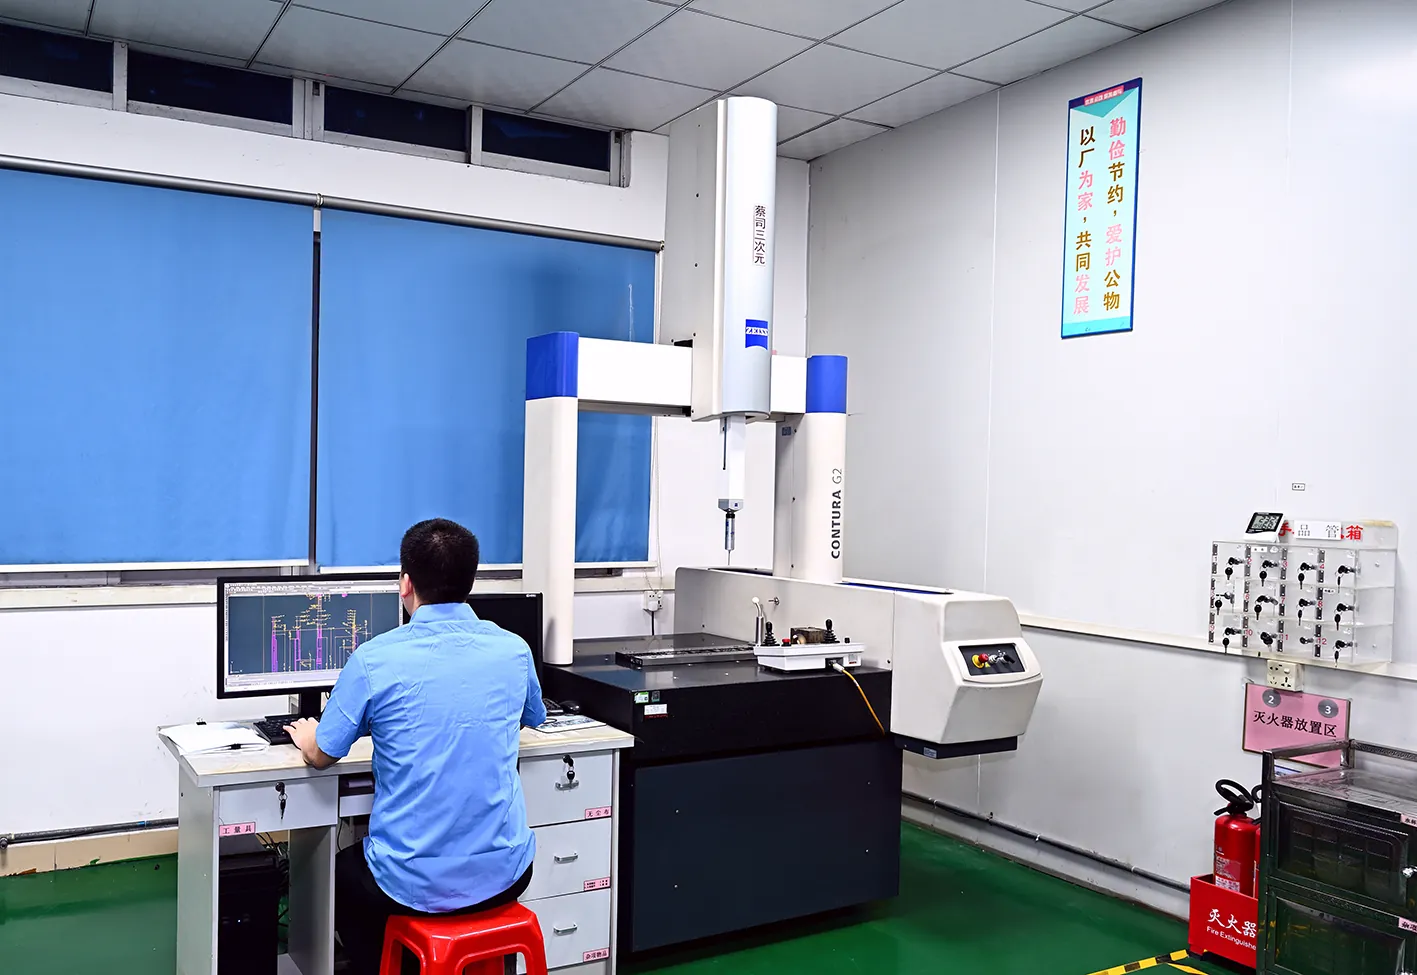
Vision measuring systems cover what a CMM probe cannot reach: small holes, edge radii, and gate vestige geometry. Vision measurement runs the same program across all cavities and flags the outliers. The combination of CMM and vision catches machining drift before it becomes a molding problem.
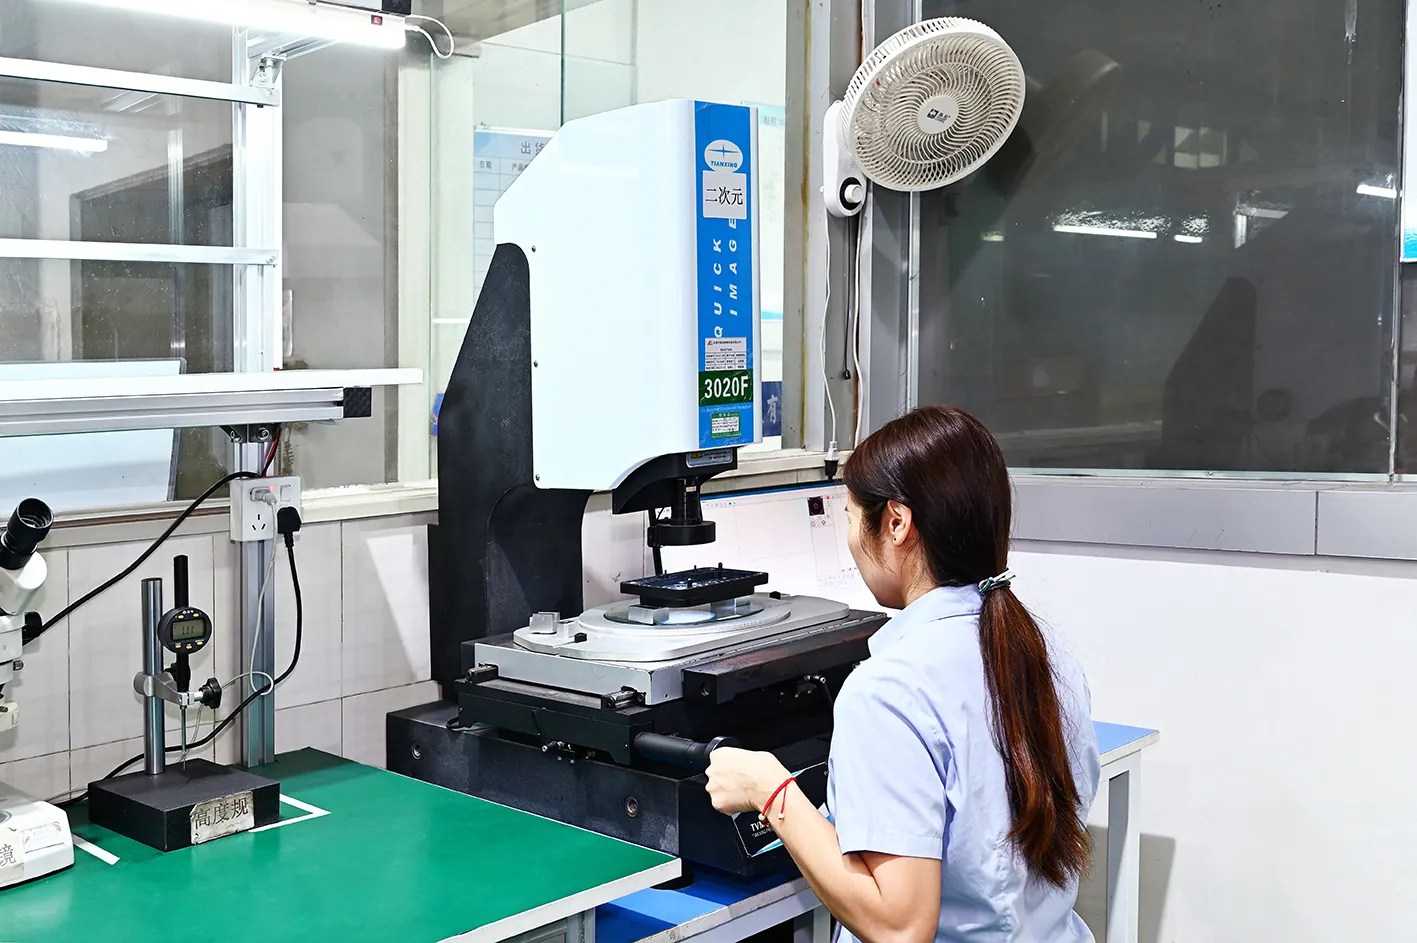
Height gauges cover the shop-floor checks: cavity depth, insert step heights, and parting line offsets. Every cavity gets the same check at the same point in the build. A 0.01 mm height difference between two cavities shows up as a wall thickness difference in the molded part.
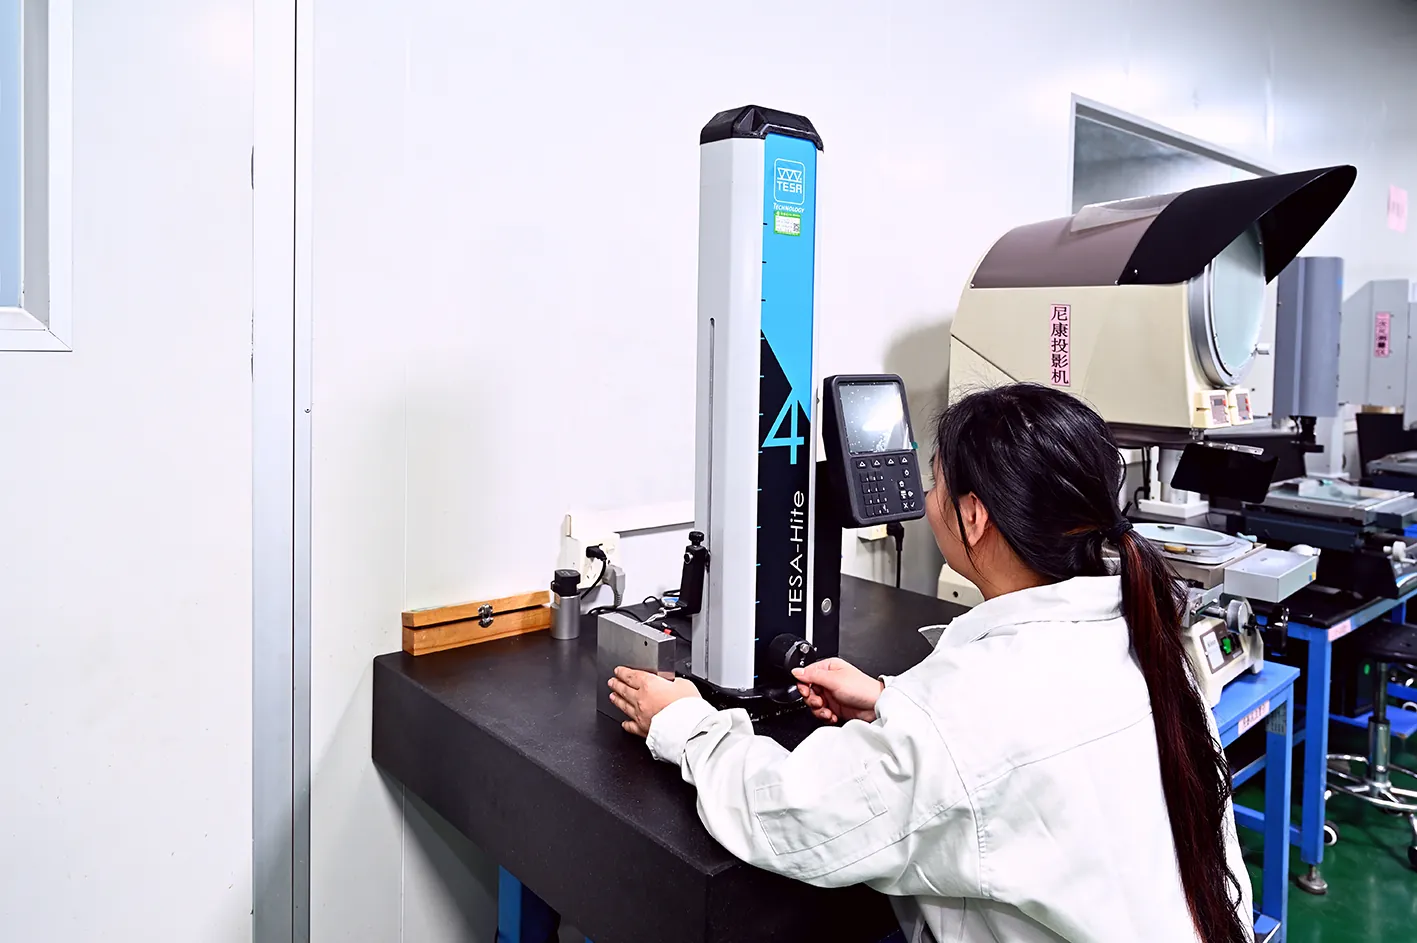
Shrinkage compensation is part of the dimensional plan. The cavity is cut oversized by the resin's shrinkage allowance, typically 0.3-0.8%. That allowance must be identical cavity to cavity. If the steel matches but cooling differs, the parts land differently anyway.
Trial Verification: Shot Weights and Process Windows
Trial is where balance gets proven, and shot weight is the fastest proof. Weigh the part from every cavity on a scale accurate to 0.01 g. The spread should hold under 2-3% typical. The cavity that weighs light is the one that will short-shot at volume.
Run the shot-weight check at the start of the trial, at the process midpoint, and at the end of the trial day. Balance that holds at one set point but drifts with barrel temperature is process-sensitive. Log the weights cavity by cavity so the balance record survives the trial.
Process window checks follow the weights. Fill at the low and high ends of the recommended fill rate. Raise and lower melt temperature within the datasheet window. A balanced mold holds the shot-weight spread across all four corners. An unbalanced mold looks fine at the nominal set point and falls apart at the edges.
The balance verification table below is the trial checklist. Each check has a method and a pass criterion. Run the list in order and the tool ships with a balance record instead of an opinion.
| Check | Method | Pass Criteria |
|---|---|---|
| Shot-weight spread | Weigh each cavity on a 0.01 g scale | Spread under 2-3% typical across all cavities |
| Fill time per cavity | Short-shot series or mold flow analysis | Fill times within a few percent typical, cavity to cavity |
| Pack pressure spread | Pressure sensors in the runner or analysis | Spread under 10% typical at end of fill |
| Coolant differential | Thermocouple or IR check on each circuit | ±3-5 °C typical across all circuits |
| Cavity dimensions | CMM program run on every cavity | Spread within ±0.01 mm typical on critical dimensions |
| Gate dimensions | Air gauge or pin gauge at buyoff | Gate depth within ±0.01 mm typical cavity to cavity |
| Process window corners | Trial at low and high fill rate and melt temperature | Shot-weight spread holds at all four corners |
← swipe to scroll →
The weight check catches filling and packing imbalance. The CMM check catches dimensional drift. Both belong in the trial protocol and in the PPAP file. The customer's quality engineer will ask for the balance record at first program review.
When to Use Valve Gates
Valve gates are the strongest balance tool available. A valve pin opens and closes each gate on command. The mold controls fill order and pack time cavity by cavity. A valve-gated runner does not depend on the resin's flow behavior for balance.
Use valve gates when the process window is narrow or the part is critical. Thin-wall parts, glass-filled resins, and visible-gate prohibitions all justify the cost. Valve gates also eliminate the gate vestige, which matters for parts feeding automated assembly lines. The cost is the actuation system, the control sequence, and the maintenance.
Valve gates solve the last-cavity-short failure directly. When a cold runner starves the far cavities at the window edge, a valve sequence packs each cavity at its own time. On 32 and 64-cavity tools, the manifold balance and the valve sequence are designed together in the analysis. The sequence is verified at trial with the shot-weight check.
Common Balance Failures and Fixes
Balance failures repeat in predictable signatures. The last cavity short-shots. The near cavities flash. One bank runs hot, and one cavity always weighs light. Each signature has a cause and a fix, and each fix is verified with the checks above.
Last cavity short: the runner or gate starves the far cavities. Fix the runner sizing first, then the gate depth, then consider a valve gate. Verify with a fill-time plot before any steel change. The fix order matters because changing two variables at once destroys the data.
Near-cavity flash: the near cavities overpack because they fill first. Reduce pack pressure, restrict the near gates, or rebalance the runner. Flash that appears only after 50,000 cycles typical is gate wear or parting steel wear, not process.
Hot spot on one bank: a cooling circuit is short, blocked, or series-connected. Measure the circuit temperatures and re-route the waterlines. A hot bank shows up as dimensional drift before a visible defect. That is why the coolant differential is a pass criterion at trial.
Consistent light cavity: a cavity that always weighs light has a machining difference. Measure the gate, the runner, and the cavity steel. If they all match, check the venting. A blocked vent traps gas and hesitates the fill. The fix is maintenance, not design.
FAQ
What does a balanced multi-cavity mold mean? Every cavity fills at the same pressure, packs at the same density, and cools at the same rate. Shot weight spreads under 2-3% typical across cavities. Coolant stays within ±3-5 °C typical. Molded dimensions hold ±0.01 mm typical spread. The parts from every cavity are interchangeable.
Natural or artificial runner balance , which should I use? Natural balance first, because equal flow lengths are stable across process changes. Use artificial balance only when the layout forces unequal flow lengths. Then verify it with mold flow analysis at every process window corner. Valve gates are the last resort when neither geometry works.
How much can shot weight vary across cavities? Keep the spread under 2-3% typical. Weigh each cavity on a 0.01 g scale at the start, middle, and end of the trial day. The cavity that weighs light will short-shot at volume. Fix it before the tool ships, not after.
What coolant temperature differential is acceptable? Hold ±3-5 °C typical across all circuits. Series circuits fail this test because the last cavity runs hot. Use parallel or individually controlled circuits. Log circuit temperatures at buyoff and re-check them when drift appears.
When do I need valve gates for balance? When the process window is narrow, the part is thin-walled or glass-filled, or the far cavities short-shot at the window edge. Valve gates control fill order cavity by cavity. They also eliminate the gate vestige for automated assembly lines.
What tolerance can a multi-cavity mold hold cavity to cavity? DieStrike machines cavity details to ±0.005 mm standard and ±0.002 mm on precision features. The molded spread holds ±0.01 mm typical on critical dimensions. That holds only when filling, packing, and cooling are balanced. The CMM report at buyoff is the proof.
The Bottom Line
Multi-cavity balance is a closed loop: design it, simulate it, machine it, verify it. The runner network sets the flow. The gates tune it. The cooling holds it. The trial proves it.
Each stage has numbers: runner ratios, ±0.01 mm gate depth tolerance, ±3-5 °C coolant differential, under 2-3% shot-weight spread, and ±0.01 mm CMM spread. Every number is checked before the tool ships. The balance record from first trial is the deliverable the customer's quality engineer asks for. Build the tool so the record passes.
DieStrike builds multi-cavity tools under IATF 16949 and ISO 9001 quality systems, with 120+ machines on the floor. Cavity machining runs at ±0.005 mm standard and ±0.002 mm precision. Production molds ship in 2-5 weeks. Standard mold parts ship in 3-7 days. Customers including TE Connectivity, Amphenol, Luxshare, and Dongshan run multi-cavity programs on tools built to these numbers.
Start with the mold flow analysis and the resin datasheet. Lock the runner, gate, and cooling plan before the mold base order. If the runner decision is still open, work through the trade-offs in our guide to choosing a hot runner for multi-cavity automotive molds.
NEXT STEP
Ready to Start Your Mold?
Send us your element dimensions or part numbers — our team responds within 24 hours with pricing and lead time.

Written by
Ray ChanMold Buyer's Guide Author · Precision Mold Manufacturing Specialist. Ray helps global importers, distributors and OEMs source factory-direct molds and mold parts.