
How to Improve Material Utilization in Stamping Dies
Table of Contents
A 1.3 million part year on a 0.8 mm mild-steel bracket pulled 1,180 tonnes of cold-rolled coil, and the single-row layout in the original die pushed 71 percent of every strip into the skeleton. The die ran clean at 220 strokes per minute, and a 10 point gain in purchased yield would have released 257,000 USD of coil in twelve months. Material is 45 to 70 percent of piece cost on a stamped part, which is why that 10 point gain is the tooling budget for the next program.
This guide covers where the material bill sits, the yield arithmetic, nesting and strip width rules, skeleton and scrap handling, the process levers that move yield, and the points where yield has to give way to burr and edge quality.
The Snapshot
- Material is 45 to 70 percent of piece cost. Cold-rolled and coated coil runs 0.5 to 1.5 USD per kg, and steel at 7.85 g per cm3 puts the sheet cost inside every stamped unit.
- A single row on a 1,000 mm coil wastes 65 to 75 percent. Pulling one 300 mm strip per coil width leaves 650 to 750 mm of side scrap unless the coil is slit or the die nests two parts across.
- A 2-out nested layout reaches 78 to 88 percent of the strip. A 2 mm web between blanks and 3 mm edge trim at the strip edges is the configuration that gets there.
- The skeleton is a hard floor at 1.2 mm. Webs run 1.5 to 3 mm, never below 1.2 mm on 0.4 mm stock, and a 0.05 mm pitch error on a 12 mm pitch costs 0.4 percent of yield over 1 million hits.
Where the Material Bill Sits in a Stamped Part
Cold-rolled and coated coil lands between 0.5 and 1.5 USD per kg. A hot-dip galvanized DC01 at 0.8 mm sits near the bottom of that band, a 590 MPa dual-phase grade sits near the top, and price moves with zinc coating weight, mill tolerance band and the width the mill has to trim for you.
Piece cost follows the sheet, not the labor. On a 0.8 mm mild-steel part the material line is 45 to 70 percent of piece cost, direct labor and press time together are usually 10 to 20 percent, and tooling amortization covers the remainder. Steel at 7.85 g per cm3 and aluminium at 2.70 g per cm3 make the arithmetic direct, because blank weight is just area times thickness times density.
Take a bracket with a net blank area of 42,000 mm2 in 0.8 mm mild steel. The blank weighs 42,000 mm2 times 0.8 mm times 0.00785 g per mm3, which is 264 g, and at 0.85 USD per kg the material in the finished part is 0.22 USD. At 71 percent yield the coil consumed per saleable part is 372 g and the material line is 0.32 USD. At 85 percent yield consumption falls to 311 g and the line falls to 0.26 USD.

That 0.06 USD per part is the whole argument. Over 5 million parts it is 300,000 USD of coil, which is a new progressive die, a coil line upgrade and a year of die maintenance. Nothing else on a stamping program moves cost that far with so little change to the press.
Scrap recovery softens the loss but never erases it. Side scrap sold as No. 1 bundles returns 60 to 80 percent of new-coil value, and a clean, dry, banded bundle sits at the top of that range. A tangled skeleton in a landfill bin returns nothing and costs 0.02 to 0.05 USD per kg to remove. Buying at 0.85 USD per kg and selling offal at 0.55 USD per kg still charges 0.30 USD per kg against every kilogram that leaves as skeleton.
Yield Arithmetic: Blank Area Against Coil Area
Utilization has two denominators, and confusing them is how programs get budgeted wrong. Strip-level yield is net blank area divided by the strip area consumed in one pitch. Coil-level yield is usable strip width divided by purchased coil width. Purchased yield is the product of the two, and that is the number the finance sheet should carry.
For a single blank per hit, strip yield is blank area divided by strip width times pitch. Add the edge trim on both sides and the bridge between blanks, and the denominator grows before any of the part has been formed. A part with a 42,000 mm2 net area in a 206 mm strip at a 303 mm pitch consumes 62,418 mm2 per blank, so the strip yield is 67 percent.
Coil-level yield is where the big losses hide. If that 206 mm strip is pulled from a 1,000 mm coil as a single row, the remaining 794 mm is side scrap and coil utilization is 21 percent. Run four strips across the same coil at 206 mm each plus slitting kerf, and coil utilization climbs above 82 percent. The die did not change. The slitting and buying decision did.
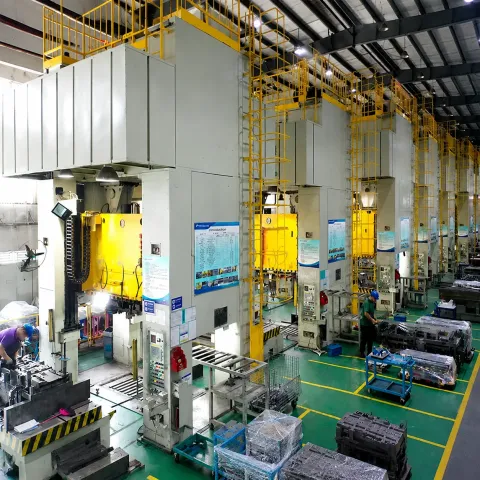
Nesting changes the strip term. A 2-out nested layout shares the denominator across two blanks, so yield rises sharply: with a 2 mm web between blanks and 3 mm edge trim, it reaches 78 to 88 percent of the strip. An interlocking arrangement, where the profiled edge of one blank sits inside the cutout of the next, adds a further 5 to 15 points.
| Layout | Strip yield | Coil yield | Purchased yield |
|---|---|---|---|
| Single row, 300 mm strip from a 1,000 mm coil | 25 to 35 percent | 30 to 35 percent | 8 to 12 percent |
| Single row, coil slit to 310 to 340 mm | 60 to 70 percent | 92 to 96 percent | 57 to 66 percent |
| 2-out nested, 2 mm web, 3 mm edge trim | 78 to 88 percent | 92 to 96 percent | 72 to 84 percent |
| Interlocked blanks, symmetric part | 85 to 95 percent | 92 to 96 percent | 78 to 91 percent |
| 4-out nested, 300k plus annual volume | 82 to 92 percent | 94 to 97 percent | 77 to 89 percent |
← swipe to scroll →
Table note: bands are typical industry values for 0.5 to 1.5 mm mild and coated steel on a mechanical press. Confirm against the coil certificate, the strip layout drawing and the weighed scrap from the first production run.
Reading Your Current Yield Before Changing Anything
A yield number taken from the die drawing is nominal, and it will disagree with the line. Measure the real one in an afternoon. Weigh 50 consecutive parts on a 0.1 g scale and average them, then weigh the coil consumed across a known stroke count. Purchased yield is total part weight divided by total coil weight consumed.
Weighing resolution decides whether you can see the problem at all. A 0.1 g scale on a 264 g blank resolves to 0.04 percent, well inside the 2 to 4 percent band you are trying to measure, while a 1 g platform scale carries a 0.4 percent error and a 10 g scale carries 4 percent, which is more than an entire nesting change is worth.
Measure the strip directly as well. Pull a 2 m length from the feed, mark 20 pitches by hand and measure the span with a steel rule or height gauge. Twenty pitches at 12 mm nominal span 240 mm, so a 1 mm error across that span is a 0.05 mm pitch error, and 0.05 mm on a 12 mm pitch is 0.4 percent of material across a million hits. Weigh a 1 m length of skeleton and divide by the pitches in it to get exact offal grams per part, which separates skeleton loss from edge trim loss.
Record three numbers per run: part weight in g, coil consumed per 1,000 parts in kg, and skeleton grams per part. Below 45 percent purchased yield the layout is the problem. Between 45 and 70 percent, the strip and the buying decision are the problem, and the blanking die geometry and clearance that set the blank edge are usually sound by then. Above 70 percent, the remaining levers are coil grade, pitch accuracy and edge trim.
Nesting Rules That Change Yield
Rotate the blank 180 degrees for a mirror-pair part. On a symmetric bracket, pair the two halves so the profiled edge of one faces the profiled edge of the other, and the gap between them collapses from a full blank width to a narrow web. Interlocking the profile of one blank into the adjoining blank with a 1.5 to 3 mm skeleton adds 5 to 15 percentage points of strip yield over a plain side-by-side nest.
Treat the web between blanks as a structural feature, not a leftover. The bridge land carries the strip through the feeder and holds the pilots in register, so it runs 1.5 to 3 mm on 0.5 to 1.5 mm stock. Never take it below 1.2 mm, and never below 2 mm on 0.4 mm stock, because the skeleton tears in the feed rolls and the line stops with a strip wrapped around the pilot.
Edge trim runs 3 mm per side as a working default. That absorbs slit-coil width tolerance and camber without shaving the outer blank. Below 2 mm the outer blank can pick up a burr from the strip edge, and above 5 mm you are paying for width you never form.
Design a straight-side carrier when the outer profile allows it. A carrier that runs along both edges and feeds the blanks on the progressive stations uses the full strip width instead of the 60 to 70 percent a conventional centre carrier leaves behind. On a 2-out progressive layout that change alone is worth 8 to 12 points.
Finally, plan scrap removal at the same time as the nest. Interlocking blanks create closed cutouts, and a cutout with nowhere to fall will ride the strip into the next station and mark the part. Size a slug hole or a trap door under every closed cutout before the die drawing is released.
Strip Width and Pitch Decisions
Strip width follows one equation: blank width plus 2 times 3 mm edge trim, plus the skeleton for a single row, or 2 times the skeleton plus the inner web for a 2-out layout. Set the coil width from that number rather than from the mill's standard catalogue.
Going 100 mm wider than the layout needs adds 4 to 8 percent dead material across the whole program, and that material is bought, shipped, stored, oiled and scrapped without ever being formed. Ordering a 340 mm slit coil instead of a 440 mm coil is a phone call, and a slitting premium of 0.03 to 0.06 USD per kg is repaid by the first few percent of recovered width.
Pitch is the second half of the denominator and the more sensitive one. Pitch equals blank length plus the bridge, and any error there multiplies by the hit count. On a 12 mm pitch, a 0.05 mm error is 0.4 percent of yield, which on a 5 million hit year is 20,000 parts of material. On a 300 mm pitch the same 0.05 mm error is only 0.017 percent, which is why short-pitch connector and terminal work is where pitch control pays.

Pitch error comes from three places: feed roll slip, pilot pin clearance, and strip growth after each trimming station. Feed roll pressure set too light slips on an oily strip, and a pilot at 0.05 mm clearance on a 12 mm pitch can pull the strip forward or back by half that clearance on every hit. Check both before redesigning a layout, because no nest recovers a pitch that drifts. A coil feed line set up for progressive dies with loop control and roll pressure logged per run is the cheapest place to fix this.
Skeleton, Side Scrap and Scrap Value
Scrap has a shelf value and it is worth defending. Clean side scrap returned as No. 1 bundles draws 60 to 80 percent of new-coil value, while a tangled, oil-soaked skeleton in a mixed bin draws the bottom of the ferrous range. The run-cost difference between scrap sold and scrap landfilled is 0.02 to 0.05 USD per kg.
Keep skeletons off the floor and oiled. A skeleton coiled under the press and banded within the shift holds its value. A pile of bent offal on a concrete floor picks up grit, water and floor sweepings, and the dealer discounts the lot. Put a scrap chopper or a coil winder at the die exit so the offal leaves as a compacted bundle rather than a tangle.
Segregate by grade. Coated, galvanized and 590 MPa-plus AHSS offal carry different prices from mild-steel offal, and the spread between the top and bottom ferrous grades runs 30 to 50 USD per tonne. One mixed bin destroys that spread across the whole year. Label four bins at the press: mild, coated, AHSS and mixed, and treat the mixed bin as a defect.
Watch the fill ratio as well. A skeleton that is 90 percent holes makes a full bin weigh as little as 300 kg. Weigh collected offal against the theoretical skeleton weight every week, because a gap between the two means material is going into the floor sweepings and never being credited.
Process Levers That Move Yield
Tailored coil widths are the cheapest lever. Buy the exact slit width the layout needs, in the grade the part needs, and stop paying for the mill's standard width. A 340 mm slit coil at 0.85 USD per kg replaces a 440 mm coil with 30 percent dead width, and the change needs no tooling at all.
Move to a 2-out or 4-out die above roughly 300,000 parts a year. A 2-out die typically costs 40 to 70 percent more than a 1-out tool of the same stations, and it pays back through the strip percentage, not through the stroke rate. Above 1 million parts a year, a 4-out layout on a straight-side press with a carrier on both edges is often the lowest cost per part, provided the press tonnage and bed size can take it.
Progressive nesting with a straight-side carrier is the structural lever. Instead of blanking a finished part on the last station, the progressive die carries the outer profile from station to station so the leading edge of one blank becomes the trailing edge of the next. That is what converts an interlocking sketch on paper into 85 to 95 percent strip yield.
Angled trimming cams and a scrap chopper handle what a straight cam cannot. Angled trim stations cut an outer profile that is not perpendicular to the feed, and on a part with a curved outer edge they recover 3 to 8 points that a straight trim turns into a wider skeleton.
One caution before any of these. Every lever above adds die stations, press tonnage or maintenance surface. A 4-out interlocking layout with a straight-side carrier is a more expensive tool to build and to repair, so run the payback against the die's full life, not against the first year of coil savings.
When Yield Fights Quality
Every point of yield taken from the skeleton comes out of the tool's ability to hold the part. A wider web reduces slug pulling, holds the pilots in register and keeps the burr inside spec, so the last 3 to 5 points of yield are the most expensive ones on the drawing.
Set a quality floor and treat it as a hard constraint. Burr height on a 0.8 mm mild-steel blank typically specs at 0.05 mm with an 0.08 mm maximum, and a skeleton squeezed under 1.2 mm on 590 MPa-plus AHSS pushes the trimmed edge into cracking and the burr past that limit. Leave the skeleton at 1.5 to 3 mm and take the yield from the buying and nesting side instead.
Slug pulling is the other trip wire. A web that is too narrow lets a trimmed slug ride back up on the punch and print a raised mark on the next blank, and the fix is a wider web or an angled punch face, never a tighter strip. Edge trim below 2 mm shows up the same way, as a shaved strip edge and a rolled burr on the outer blank.
Coil Width, Grade and Supplier Decisions
Coil buying is where yield is won or lost before the press starts. Two numbers on the purchase order decide most of it: the slit width and the thickness tolerance band. A slit width 100 mm wider than the layout needs is 4 to 8 percent dead material, and a thickness band held at plus or minus 0.02 mm on a nominal 0.8 mm coil instead of minus 0.05 mm is another 2 to 3 percent of steel in every part.
Grade substitution is a yield lever only when the formability allows it. Dropping a 590 MPa dual-phase to a 340 MPa high-strength low-alloy grade widens the forming window and lets a tighter nest run without edge cracking, but it changes crash performance and needs the customer's release, so that call does not belong in the tool shop.
Where a program needs the die and the coil planned together, a stamping die manufacturer working to IATF 16949 with 120+ machines and DFM feedback inside 24 hours can run the strip layout against the coil widths actually available, and hold mold and die tolerance at plus or minus 0.005 mm, with plus or minus 0.002 mm on EDM and jig grinding. Die programs from a shop at that level run 2 to 5 week lead times, with standard components at 3 to 7 days.
Measuring Yield on the Line
Put five numbers on one weekly scorecard and the program manages itself: purchased yield in percent, strip yield in percent, skeleton grams per part, pitch error in mm, and scrap credit in USD per part.
Convert every point into money. On this program 1,320 tonnes of finished parts is the annual output, so one point of purchased yield is about 15 tonnes of coil, roughly 13,000 USD a year. A 10 point target over two quarters is 130,000 USD, and that number belongs on the press-side board, not in a finance deck.
Material Utilization FAQ
Q1. What is a realistic material utilization for a stamped part?
Between 60 and 88 percent of the strip is typical, and 45 to 75 percent of the purchased coil once coil width and slitting are counted. A single row on a 1,000 mm coil with one 300 mm strip used wastes 65 to 75 percent of the coil width.
Q2. How narrow can the skeleton between blanks be?
1.5 to 3 mm on 0.5 to 1.5 mm stock. Never below 1.2 mm, and never below 2 mm on 0.4 mm stock, because the skeleton tears in the feed rolls and a 590 MPa-plus grade cracks at the trimmed edge.
The Bottom Line
Material utilization in stamping is two numbers multiplied: strip yield from blank area against strip width times pitch, and coil yield from usable strip width against purchased coil width. Hold the web at 1.5 to 3 mm, the edge trim at 3 mm per side, and the pitch error under 0.05 mm on a 12 mm pitch, and a 2-out nested layout reaches 78 to 88 percent of the strip.
Buy the coil in the width the layout needs, keep the skeleton clean, banded and segregated by grade, and weigh the offal against the layout theory every week. Those moves need no new tooling. Above 300,000 parts a year, a progressive nest with a straight-side carrier is the structural answer.
DieStrike builds stamping dies and precision molds to IATF 16949 with plus or minus 0.005 mm mold tolerance, HRC 62 cavity heat treatment and 120+ machines, serving tier-1 programs with TE, Amphenol, Luxshare and Dongshan. If a strip layout is leaving material on the floor, send the part drawing and the annual volume and we will return a nesting and coil width proposal before the next die drawing is cut.
KEEP READING
Related Reading
How to Design a Strip Die: Layout, Pitch and Carrier
The strip layout decisions that fix yield before a single cut is made on the die.
Read articleArticleHow to Set Up a Coil Feed Line for Progressive Dies
Feed accuracy, loop control and the pitch error that eats yield across a million hits.
Read articleArticleHow to Select Stamping Lubricants for Die Life
Lubricant film, coating compatibility and the cost per part of getting the film wrong.
Read articleServiceStamping Die Manufacturing
IATF 16949 progressive and transfer dies with DFM feedback in 24 hours and 2 to 5 week lead times.
Read articleNEXT STEP
Ready to Start Your Mold?
Send us your element dimensions or part numbers — our team responds within 24 hours with pricing and lead time.

Written by
Ray ChanMold Buyer's Guide Author · Precision Mold Manufacturing Specialist. Ray helps global importers, distributors and OEMs source factory-direct molds and mold parts.