
How to Write a First Article Inspection Report for Molded Parts
Table of Contents
A connector OEM returned a 16-cavity mold shipment because the first article inspection report listed 42 features while the drawing carried 78. The supplier measured every dimension, but the report could not prove it. Two months of program delay followed, plus a requalification fee that ran into five figures. This is the most common failure mode in mold buy-off. The parts were fine. The paperwork was not.
A first article inspection report, or FAI report, is the legal bridge between "the mold works in our shop" and "the mold is approved for production." Buyers at automotive, connector and medical-adjacent programs reject more tooling packages over documentation gaps than over dimensional failures. A well-written FAI report answers one question with zero ambiguity: does every single characteristic on the revision-level drawing match the parts this mold produces, measured by a method accurate enough to prove it?
DieStrike runs IATF 16949 quality systems across 120+ machines for connector OEMs including TE Connectivity, Amphenol and Luxshare. Every mold we ship for a T1 sampling milestone leaves with a dimensional report attached. This guide shows how that report gets built, section by section, and where suppliers lose approval rounds.
The Snapshot
- AS9102-style FAI covers 100% of drawing characteristics. Missing one ballooned feature is the #1 rejection reason, ahead of any dimensional miss.
- Measurement resolution must be at least 10% of the tolerance band. For a ±0.05 mm feature, that means a 0.005 mm resolution instrument or better.
- Typical full layout uses 3-5 parts from consecutive shots. Capability studies (Cpk ≥1.33) need 30-125 parts depending on the customer spec.
- Gauge R&R must stay under 10% of tolerance for critical characteristics and under 30% for non-critical ones, per AIAG measurement system analysis rules.
- Precision mold FAI at DieStrike holds ±0.005 mm on key mold dimensions and ±0.002 mm geometry on mold components, verified on CMM before report writing starts.
What a First Article Inspection Report Must Prove
An FAI report is not a quality certificate. It is an evidence package. It must prove four things, and customers audit all four independently.
1. Every design characteristic was measured. Every dimension, note, GD&T callout and material spec on the drawing gets a numbered line in the report. A drawing with 78 balloons produces a report with 78 result rows. No consolidation, no "verified where critical."
2. Each measurement used an adequate method. The report names the instrument per characteristic: CMM program number, caliper serial, optical comparator, or functional gauge. The 10% resolution rule applies. A ±0.025 mm tolerance cannot be verified with a 0.02 mm graduation caliper, and auditors check this arithmetic first.
3. Actual values are recorded, not just pass marks. Modern buyers want measured numbers. "OK" or a checkmark without data fails most automotive and connector audits, because a reviewer cannot judge marginality or process centering from a binary flag.
4. Any deviation is dispositioned and traceable. Out-of-tolerance results need a documented path: rework, reject, or customer-approved concession with a deviation number and expiry. A blank disposition field freezes the entire approval.

The report also fixes the configuration baseline. It records the drawing revision, mold ID, cavity number, material lot and process conditions at sampling time. If the mold later produces drift, the FAI report is the reference point that separates a mold problem from a process problem. That baseline function is why customers archive FAI packages for the life of the tool, often 7-10 years in automotive programs.
FAI vs PPAP vs ISIR: Which Document You Need
Three acronyms overlap enough to cause real delays. Writing the wrong document wastes an entire submission cycle, typically 2-4 weeks.
FAI (First Article Inspection) comes from aerospace practice, standardized as AS9102 with its three-form structure: part number accountability, product accountability, and characteristic accountability. It inspects 100% of drawing characteristics on 1-5 parts. Many industrial and connector customers now ask for "AS9102-style FAI" even outside aerospace.
PPAP (Production Part Approval Process) is the AIAG automotive package. A full Level 3 submission carries 18 elements, and the dimensional results form is where the FAI-style layout lives. PPAP additionally demands capability studies (Cpk ≥1.67 typical for critical characteristics), control plans, PFMEA and a signed PSW. The dimensional piece alone rarely satisfies an automotive buyer. See our PPAP mold sampling guide for the full package.
ISIR (Initial Sample Inspection Report) is the European, VDA-flavored equivalent: 3-5 consecutive production parts, full dimensional layout, plus material certs and appearance approval. German and European automotive programs usually ask for ISIR at mold buy-off and PPAP-style data at SOP.
The practical decision rule: check the purchase order quality clause. If it references AS9102, build the three-form FAI. If it references AIAG PPAP, the dimensional report is element 9 of 18 and you need the whole package. If the buyer is European or references VDA, plan an ISIR with consecutive-shot samples. Writing an FAI when PPAP was contracted is the most expensive mismatch, because 17 other elements still remain.
The Anatomy of a First Article Inspection Report
A complete FAI package for molded parts has eight sections. Every section maps to a customer audit question. Build them in this order and the package reviews cleanly.
Section 1: Header and part accountability. Part number, drawing revision level, mold number and cavity ID, purchase order number, sample date, and quantities produced versus inspected. For a family mold, every cavity gets its own report or its own column set.
Section 2: Configuration baseline. The exact drawing revision, plus every approved deviation or ECN that changes it. If a concession from a previous submission is still active, its number appears here. This section answers "what definition did you inspect against?"
Section 3: Material and process records. Resin supplier, grade, lot number, certificate number, drying conditions and the process window used at sampling. Colorant lot for colored parts. Insert part numbers if the mold is an insert-molding tool.
Section 4: The ballooned drawing. A copy of the drawing with every characteristic numbered in circles (balloons). This is the master index for Section 5. One number per requirement, including notes.

Section 5: Characteristic results table. The core of the report. One row per balloon: number, characteristic description, nominal, tolerance, measured value(s), method/instrument, and result. This table is where 80% of review time goes.
Section 6: Nonconformance and deviation log. Every out-of-tolerance characteristic gets a row: deviation number, description, quantity affected, disposition, and customer approval status. Empty means all-pass, which reviewers still sign explicitly.
Section 7: Supporting evidence. CMM program outputs, gauge R&R studies for critical characteristics, material certificates, appearance approval (grain, gloss, color delta-E), and photos of cosmetic surfaces under defined lighting.
Section 8: Signatures. Inspector, quality engineer, and the authorized supplier representative. Customer sign-off block stays blank until they approve. Unsigned reports are treated as drafts and bounce back immediately.
Ballooned Drawings and Characteristic Numbering
Ballooning is where FAI reports live or die. The rule is absolute: one balloon per verifiable requirement. Reviewers count balloons and compare against the drawing, and a mismatch rejects the package before any measurement is read.
What gets a balloon. Every dimensioned feature, every GD&T callout (flatness, position, profile each get separate numbers), every note that creates a verifiable requirement ("all edges break 0.05-0.15 mm," "texture per SPI B-2," "no sink on A surface"), the material spec, and regulatory markings like UL symbols or recycle codes.
What commonly gets missed. Notes in the title block. General tolerance notes still need one balloon covering all undimensioned features, usually inspected by attribute or sampled dimensions. Datums referenced by GD&T callouts need to be physically identifiable and noted in the report. Threads get their own balloon with the gauge class named, for example "M3 x 0.5 - 6H go/no-go gauge."
Numbering discipline. Number balloons sequentially by drawing zone or feature type, and keep the numbering stable across submissions. If revision B adds three features, they become new numbers at the end. Re-numbering everything between revisions breaks traceability and forces the customer to re-review the whole report.
Count verification. Two people count independently: the inspector who balloons and the quality engineer who audits. For a connector housing with 60-120 characteristics, independent counting catches the missed note in roughly 1 review out of 8. The count appears on the report header: "78 characteristics ballooned, 78 inspected, 78 results recorded." That single line preempts the most common audit question.
Critical, Major and Minor Characteristics
Not all balloons are equal. Classification drives sampling size, method choice and deviation policy, so it gets decided before measurement starts, usually at DFM stage. Most automotive and connector programs use a three-tier scheme.
Critical characteristics (CC) affect fit, function or safety directly: mating interface dimensions on a connector housing, pin cavity positions, sealing surfaces, thread geometry. These demand CMM or dedicated gauge measurement, 100% reporting, Cpk ≥1.67 in PPAP submissions, and gauge R&R under 10% of tolerance. Typical critical tolerance bands run ±0.025 to ±0.05 mm on precision molded parts. Any critical deviation is an automatic reject unless the customer signs a concession in writing.
Major characteristics affect assembly or appearance but not safety: overall envelope dimensions, wall thickness at visible areas, boss heights. Method can be CMM, optical comparator or calibrated calipers, with R&R under 30% of tolerance. Deviations can be dispositioned internally if within functional limits, but still get logged and reported.
Minor characteristics are cosmetic or non-functional: radii without callouts, hidden ribs, non-mating draft surfaces. Sampling inspection is acceptable. Deviations rarely block approval but must still appear in the log.
Classification comes from the drawing if the customer marked it (many use triangle or diamond flags). If the drawing is silent, the supplier proposes a classification list and gets it approved before sampling. Proposing after measurement starts looks like grade-shopping and draws a second review round. Classification also sets reporting depth: critical characteristics often need all 5 sample values listed individually, while minor characteristics can report max/min across the sample set.
Full Dimensional Layout vs Sampling
AS9102 FAI requires 100% characteristic coverage, but coverage and sample size are two different decisions. Coverage means every balloon gets a result. Sample size means how many physical parts back that result.
Standard FAI layout: 3-5 parts. The industry norm for mold buy-off is 3 to 5 consecutive shots per cavity, fully measured. Consecutive matters: shots 47, 48 and 49 prove the mold runs stable, while cherry-picked parts prove nothing. For a 16-cavity mold, that is 48-80 parts measured, each cavity reported separately or in a cavity-by-characteristic matrix.
When more parts are required. Capability submissions (Cpk) need 30 parts minimum, with 100-125 parts common for automotive critical characteristics. Appearance approval may need 5-10 parts across the process window. If the customer references a specific sampling standard, follow it exactly rather than substituting judgment.
Cavity-to-cavity variation. Multi-cavity molds fail FAI most often on cavity variation, not absolute dimensions. Runner imbalance shows up as one cavity running 0.03-0.05 mm different from the rest on the same characteristic. The report must show per-cavity data so this pattern is visible. A single averaged value hides it and gets rejected when the customer runs their own layout.
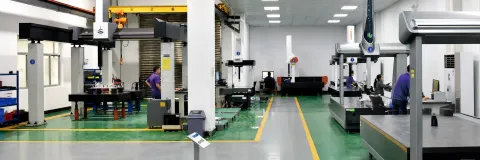
The reduced-layout shortcut and why it fails. Some suppliers measure only critical characteristics and label the rest "verified by tooling." This is a rejection trigger in any IATF 16949-audited program. The whole point of first article inspection is that the tooling assumption gets proven against reality. If cost pressure is real, negotiate the layout scope with the customer in writing before sampling, not after.
Matching Measurement Methods to Features
Each characteristic gets a named method in the report. The method must resolve at least 10% of the tolerance band, and for critical features 10:1 is treated as the floor, not the target. Method mapping is where mold shops show their metrology depth.
| Feature Type | Preferred Method | Typical Resolution | Report Entry Notes |
|---|---|---|---|
| 3D profiles, hole positions, true position GD&T | CMM (contact probing) | 0.0005-0.001 mm | Record program number + datum scheme |
| Linear dims >±0.05 mm, external features | Digital caliper / micrometer | 0.01 mm / 0.001 mm | Serial number + calibration due date |
| Thin walls, fine ribs, delicate geometry | Vision system / optical comparator | 0.001-0.002 mm | Non-contact avoids deflection error |
| Threads | Go/no-go gauge + thread pins | Attribute | Name gauge class, e.g. M3-6H |
| Flatness, warpage on A surfaces | CMM scan or granite + indicator | 0.002-0.005 mm | State fixture and clamping condition |
| Cosmetic: grain, gloss, color | Visual vs limit samples / gloss meter | Attribute / gloss units | Define lighting, distance, angle |
← swipe to scroll →
Table note: Typical industry resolutions for molded-part FAI; instrument selection must meet the 10% resolution rule against the specific drawing tolerance.
CMM programming discipline. Every CMM characteristic in the report traces to a numbered line in the measurement program. The program runs against the same datum scheme as the drawing: A-B-C datums in the drawing order. Restraint condition gets documented, because a free-state measurement of a thin-wall housing can differ 0.05-0.1 mm from a fixtured one. The report states which was used. For details on reading the output side, see our CMM report guide.
Gauge R&R timing. Measurement system analysis runs before first article measurement, not after a rejection. For each critical characteristic measured by hand gauge, a 10-part, 3-trial, 2-appraiser study is standard. If R&R exceeds 10% of tolerance, the method gets upgraded before sampling. Recording "R&R = 8.2% of tolerance" in the report header removes a whole audit branch.
Temperature conditions. Precision work references 20°C per ISO 1. Parts equilibrate 4-8 hours before CMM measurement. A molded part measured at 28°C in summer can read 0.02-0.04 mm larger on a 100 mm steel-equivalent dimension from thermal growth alone. The report records lab temperature for critical layouts.
Recording Actual Values and Out-of-Tolerance Flags
The results table has a fixed column structure. Deviating from it costs review time and draws questions.
Columns, left to right: balloon number, characteristic description, nominal value, tolerance (plus/minus or limits), measured actual, method/instrument ID, result flag. For multi-sample layouts, one column per part or cavity: "P1, P2, P3" or "C1 through C16."
Record actuals with full instrument resolution. A CMM reading of 4.9873 mm gets written as 4.987, not rounded to 5.0 and not marked "OK." Rounding to the tolerance limit is a specific audit trap: a 4.996 reading against a ±0.005 limit passes, but hiding the actual value prevents the reviewer from seeing the process runs at the edge. Edge-running processes get flagged for capability review even when all values pass.
Flag conventions. In-spec rows show the value. Out-of-spec rows show the value plus a clear flag: asterisk, bold, or "OT" in the result column, and a cross-reference to the deviation log number. The flag must be impossible to miss. A reviewer who finds an unflagged out-of-tol value stops trusting the entire report and re-audits everything.
Marginal results deserve commentary. When a characteristic reads within 20% of the tolerance limit, a good report adds a note: "running high, correlates with gate-side shrinkage; mold compensation planned at revision." This turns a nervous pass into evidence of process control. It also protects the supplier if the characteristic drifts out later, because the report showed awareness.
Attribute characteristics. Cosmetic and go/no-go features record the standard used ("limit sample LS-03 approved 2026-04-12") and the result per part. Vague entries like "acceptable" without a referenced standard fail IATF audits.

Handling Deviations: Reject, Rework or Concede
Every FAI has a chance of finding out-of-tolerance results. The report quality is judged by how deviations get handled, not by whether they exist. A clean disposition path often saves the approval timeline even with real misses.
Option 1: Re-run the sample. If the miss traces to a transient cause (wrong process setting, unmatured parts, fixture error), correct it, re-run production and re-inspect. The report then carries the new data, with a note that the first run was invalidated and why. Parts molded within 24 hours can still show post-mold shrinkage movement, so a 24-48 hour stabilization before final measurement is standard practice and prevents false rejects.
Option 2: Fix the mold. Dimensional misses from the mold itself mean steel gets cut, welding and re-machining happens, or inserts get remade. The deviation log records the root cause and the corrective action: "Cavity 7 bore diameter 0.03 mm under nominal, insert remachined, re-sampled 2026-09-14." A new FAI or a delta-FAI covering affected characteristics follows.
Option 3: Customer concession (deviation permit). When the measured value sits outside the print tolerance but the part still functions, the supplier submits a written deviation request. It states the characteristic, the measured range, functional justification, quantity covered and an expiry (typically one shipment lot or 90 days). The customer's design or quality engineer signs it. Only then does the deviation number appear in the FAI report with "conceded per DEV-2026-041" status. Self-approved concessions do not exist. An unsigned concession is just a rejection with extra steps.
What never works: deleting the failed row, re-measuring until a pass appears without documenting the re-run, or marking the characteristic "not verified." Customers compare balloon counts against drawing counts, and auditors compare measurement timestamps. All three shortcuts surface.
Material Certs, Process Records and Traceability
Dimensional data without traceability proves nothing about repeatability. Section 3 of the package carries the supporting chain, and reviewers check dates for consistency before reading any measurements.
Material traceability. Resin certificate of analysis matching the lot number on the bag used at sampling. Drying record: temperature and hours, for example 4 hours at 80°C for a typical unfilled PA66 grade, per the supplier datasheet. Moisture-related dimensional drift is real, and a missing drying record invites the question of whether the layout represents a properly processed part.
Process record. The actual parameter sheet at sampling: melt temperature, mold temperature, injection profile, holding pressure and time, cycle time. Not the theoretical window. If the customer later reports production problems, this sheet shows whether their process matches the approved sample conditions.
Mold and tooling identification. Mold serial number, cavity and insert IDs, and the mold revision status. Where the mold itself was verified, its own dimensional data connects here. DieStrike records mold component geometry at ±0.002 mm and key mold dimensions at ±0.005 mm before tooling leaves the shop, which is the upstream data that makes part-level FAI results predictable rather than surprising.
Sample part retention. Retain 2-3 golden samples with the report, labeled with mold ID, date and deviation references. Customers ask for them back months later when a production drift dispute starts. Retention is typically the life of the program.
The Approval Package: Signatures and Archiving
The final assembly of the package determines whether it clears review in one pass. Format matters as much as content.
Assembly order. Follow the eight sections listed earlier, plus a cover sheet summarizing: total characteristics (ballooned/inspected/passed/deviated), sample size and dates, active deviations and their approval status, and the overall recommendation ("approve for production," "approve with deviations," or "hold pending mold correction"). A reviewer should decide the disposition from the cover sheet alone.
Signature discipline. Wet or verified e-signatures from the inspector and quality authority. Stamped dates. The customer block stays empty. Pre-signed customer blocks void trust instantly.
Digital package standards. One PDF, bookmarked by section, under 50 MB. CMM raw data attached as separate files with program numbers matching the results table. File naming that includes part number, revision, mold ID and date: "PN12345_revC_MOLD-088_FAI_2026-09-17.pdf." Review teams handle dozens of submissions weekly, and clean naming alone reduces bounce-backs.
Archiving. Supplier-side retention matches or exceeds the customer requirement, commonly 7 years minimum in automotive and the life of the tool plus one year elsewhere. The archive stores the signed PDF, raw CMM data, gauge R&R studies, material certs and the retained-sample log. When a mold goes back into production after 3 years in storage, the archived FAI is the baseline that tells you what to re-verify.
7 FAI Report Mistakes That Trigger Rejection
These seven failure modes account for most bounced first article submissions across mold buy-off programs. Each one is cheap to prevent and expensive to recover.
1. Balloon count mismatch. The report shows 74 characteristics, the drawing has 78. Usually missed title-block notes or GD&T callouts. Automatic rejection, full re-review.
2. Insufficient measurement resolution. A ±0.03 mm tolerance verified with a 0.01 mm caliper violates the 10% rule on paper, even when every value passes. Reviewers check the instrument column against the tolerance column with a calculator.
3. Pass marks without actual values. Checkmarks and "OK" entries instead of measured numbers. Common in legacy spreadsheet templates. Fails IATF-style audits on sight.
4. Averaged multi-cavity data. Reporting one mean value across 16 cavities hides a runner imbalance of 0.03-0.05 mm on one cavity. The customer's own layout finds it, and the credibility of the whole package collapses.
5. Undocumented deviations. An out-of-tol value with no deviation number, no disposition and no concession signature. Worse than the miss itself, because it reads as concealment.
6. Wrong sample provenance. Parts from trial shot 3 with unstable process, or parts measured 1 hour after molding before shrinkage stabilizes. Dimensional results can shift 0.02-0.08 mm in the first 24-48 hours depending on resin crystallinity.
7. Stale revision baseline. Inspecting against revision B while the PO references revision C. The whole report is void regardless of measurements, and it restarts the 2-4 week approval clock.
One systematic guard catches all seven before submission: an independent audit of the package against the drawing by an engineer who did not perform the inspection. At DieStrike, every FAI-style dimensional report attached to a GD&T-flagged drawing passes that second-pair check before it ships with the tool.
FAQ: First Article Inspection Reports
Q1. How many parts do I need for a first article inspection?
For AS9102-style FAI or ISIR, 3-5 consecutive production shots per cavity is standard, all parts fully measured. Capability studies need more: 30 parts minimum, 100-125 for automotive Cpk submissions at level 3 or higher. Cavity-by-cavity data is mandatory for multi-cavity tools.
Q2. Can I use a caliper for a ±0.05 mm tolerance?
Yes. The 10% resolution rule allows instruments resolving 0.005 mm or finer for a 0.1 mm total band. A 0.01 mm digital caliper qualifies on resolution, though CMM is preferred for position and profile callouts where datum alignment drives the result. Record the caliper serial number and calibration date either way.
Q3. What if one characteristic fails but the part works?
Submit a written deviation request with the measured range, functional justification, affected quantity and an expiry date, typically 90 days or one lot. The customer design or quality engineer must sign it. Log the approved deviation number in the FAI report. Never disposition a print deviation unilaterally.
Q4. Is an FAI report the same as PPAP?
No. The dimensional layout inside PPAP (element 9 of 18 at Level 3) resembles an FAI, but PPAP adds capability studies at Cpk ≥1.67 for critical characteristics, control plan, PFMEA, material certs and a signed PSW. Check the PO quality clause: AS9102 means FAI forms, AIAG means the full 18-element package.
Q5. How long does an FAI report take after mold trial?
For a single-cavity part with 40-60 characteristics, 3-5 working days including CMM programming, measurement, report assembly and internal audit. A 16-cavity mold with 100+ characteristics per part typically needs 7-10 days. Part stabilization (24-48 hours post-molding) and gauge R&R studies run inside that window.
The Bottom Line
A rejected FAI report costs 2-4 weeks and a requalification cycle, almost always over paperwork rather than parts. Balloon every characteristic, record actual values with adequate resolution, disposition every deviation in writing and keep per-cavity data visible. That discipline is what separates a one-pass approval from months of drift.
DieStrike ships IATF 16949-grade tooling with dimensional reports and T1 sampling data as standard. If your next program needs a first article package that survives audit on the first pass, talk to our engineering team before steel gets cut.
KEEP READING
Related Reading
How to Read a CMM Report: Dimensional Data for Mold Buyers
Decode CMM output: nominal, deviation, out-of-tol flags and what each line tells you about the mold.
Read articleArticleHow to Run Mold Sampling for PPAP: ISIR and Capability
Sample sizes, Cpk targets and the ISIR paperwork that gets PPAP signed without extra rounds.
Read articleArticleGD&T for Mold Buyers: How to Read Datums, Flatness and Tolerance Callouts
Datum schemes, flatness callouts and tolerance interpretation before you balloon a drawing.
Read articleServiceMold Trial & T1 Sampling
T0/T1 trials with dimensional reports, sample parts and first article approval support at DieStrike.
Read articleNEXT STEP
Ready to Start Your Mold?
Send us your element dimensions or part numbers — our team responds within 24 hours with pricing and lead time.

Written by
Ray ChanMold Buyer's Guide Author · Precision Mold Manufacturing Specialist. Ray helps global importers, distributors and OEMs source factory-direct molds and mold parts.