
How to Compensate Springback in Stamping Dies: Fixes and Loop
Table of Contents
A dual phase bracket comes off a brand new die sitting 3 degrees open on every flange against a print that allows 0.5 degrees. The die was machined correctly. The steel moved back when the punch retracted, and nobody paid for that movement up front. The first rework consumes a welding and regrind cycle, and an unmanaged loop burns 2 to 6 weeks of tryout and 3 to 8 die reworks before the angles settle. This article covers the discipline that closes springback before launch: measure the recovery on the real coil, compensate the die steel against that number, retry, and hold the result against a deviation chart.
Scope is bent and formed features on carbon, stainless, dual phase and martensitic sheet from 0.5 to 3 mm.
The Snapshot
- Strength multiplies the rebound. Elastic modulus barely moves across steel grades at 205 to 210 GPa while yield climbs from 140 to 1,500 MPa, so a 980 MPa dual phase part rebounds 2 to 3 times the angle of an S304 low-carbon sheet on the same tool.
- Each correction removes 60 to 80 percent of the residual. Two to four iterations from first try to print is normal, and the count drops toward two when the CAE model is calibrated on a physical try.
- Coining re-trims the angle. A bottoming strike at 1.2 to 1.5 times the normal forming force sets the bend by plastic volume displacement instead of elastic recovery.
- The loop has a price. Unmanaged compensation runs 2 to 6 weeks of tryout and 3 to 8 die reworks. Calibrated simulation plus one physical try cuts roughly half of that.
Why Springback Scales With the Material
Every air bend is part plastic and part elastic. The punch presses material past its yield point near the inner surface, while the outer layers only stretch. When the load releases, the elastic half pulls back and the part loses angle. That lost angle is springback, and the die has to give it back somewhere.
Two ratios set the size of the loss. The first is bend radius over sheet thickness, R over t. A sharp inside radius at R/t near 1 keeps most of the section plastic, so recovery stays small. A radius at R/t of 6 stores elastic energy across a thick band of material, and the return angle grows with it.
The second ratio is yield strength over elastic modulus. This is the number that makes high strength grades hard. All steels carry roughly the same modulus, 205 to 210 GPa, whether they are DC01 mild or 1,500 MPa martensitic. The yield strength spans a factor of ten across that same range.
Elastic strain at the point of forming is yield divided by modulus, so a 980 MPa dual phase grade stores 5 to 7 times the recoverable strain of a 140 MPa mild steel. That is why the dual phase part rebounds 2 to 3 times the angle of an S304 low-carbon sheet at the same tool.

Part stiffness couples into the same picture. Bending stiffness scales with thickness cubed, so a 0.8 mm flange keeps flexing during handling and measurement while a 2.5 mm box section holds whatever the die gave it. The same recovery angle is a bigger functional error on the flexible part because assembly pulls it further. Graded material selection and its springback trade-offs are covered in the article on designing for high strength steel stamping.
On multi-bend parts the recovery does not stay local. One flange springs, the panel rotates about its neutral axis, and the neighboring bend lands somewhere else. This is why a deviation map per feature beats a single overall angle check.
Measure the Coil Before You Cut the Steel
Compensation starts with a number, and the only number worth paying for is measured on the coil lot that will run the program. Ask for a free-bend test from the material supplier or run it in-house: form a strip to 90 degrees over a defined radius, release, and record the returned angle. Do it at 0 degree, 45 degree and 90 degree to the rolling direction, because springback varies with grain orientation and can differ by a full degree between directions on the same coil.
At tryout, measure the trimmed part, not the in-strip part. Spring-formed features relax further once the surrounding web is cut away. A CMM with a stylus on the bend angles, or a blue light scan against nominal CAD, gives the deviation map: per feature, in degrees on angles and millimetres on radii and hole positions. That map is the compensation work order.
Springback varies lot to lot, so the measurement discipline extends to the material certificate. Track the n-value, the r-value and the yield spread printed on the mill certificate for every coil. A 40 MPa shift in yield between two coils of the same grade moves the recovery angle, and a die compensated on the trial lot can start passing or failing parts on the first production lot if nobody checked the certificate.
The tool has to be trustworthy before the part is judged. At DieStrike, critical die features are held to 0.005 mm, and EDM and jig-grinding work goes to 0.002 mm, so a measured deviation of 1 degree traces to the material and not to a sloppy radius. When a die arrives from another shop, verify the formed radii against the drawing before blaming the coil.
The Die Geometry Compensation Toolkit
Five levers move a sprung part back onto nominal. Most production dies combine two or three of them, chosen by feature geometry and tonnage headroom.
Overbend the angle. Cut the die to close the bend past 90 degrees by exactly the measured recovery, so the rebound lands the part on print. An overbend of 2 to 4 degrees is routine on dual phase flanges. This is the cheapest fix and the first one attempted, because it changes one surface. Its limit is accuracy: overbend assumes the recovery is constant, and recovery drifts with lot-to-lot yield spread, so pair it with certificate tracking.
Undercut the radius. Springback on a flange rotates the wall about the inside radius, so the wall overshoots nominal while the radius itself springs tight. Grind the punch nose radius slightly under nominal, or cut a shallow reverse curvature into the die radius, so the rebound flattens the profile onto the drawing radius instead of overshooting it. Radius compensation matters most where the print controls a profile or a seal line rather than an angle.
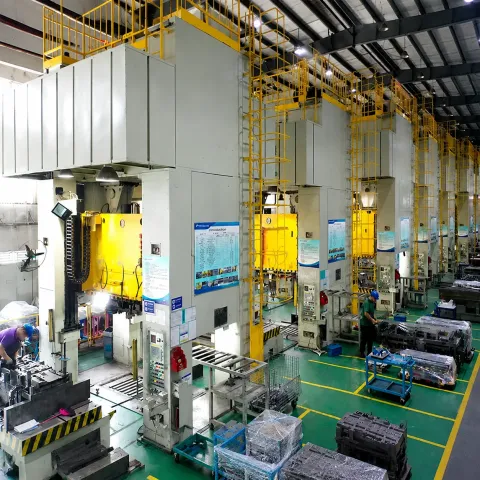
Bottom and coin the bend zone. A coining strike at the end of the stroke plastically re-trims the angle at the bend line, so the recovery has almost nothing left to spring. Plan the force at 1.2 to 1.5 times the normal forming load; on a part whose 90 degree bend needs 40 tonnes, the coined version needs 50 to 60 tonnes, and the press must own that margin with the usual safety factor on top. The press-tonnage arithmetic behind that decision is worked through in the article on calculating press tonnage for stamping dies. Coining is the strongest answer for short, stiff flanges and the wrong answer for long automotive panels, where 60 tonnes of local coining pressure across a 400 mm flange leaves visible read-through marks on the cosmetic face.
Add beads and embosses. Draw beads and small embosses lock panel shape by putting tension into the flange, and tension-dominated sections spring far less than bending-dominated ones. On an automotive outer panel, two beads 80 to 150 mm from the trim line can recover 1 to 2 degrees of bow that overbending alone cannot hold, because the bead stretches material instead of merely redirecting its elastic return.
Raise the blankholder force. On draw and reform stations, a heavier blankholder pulls the flange into membrane tension during forming. Sweep the force toward the top of the wrinkle-free window: on a 1.2 mm HSS part the difference between 100 kN and 160 kN of blankholder load can move the flange angle by a full degree. Go too far and the surface scars or the wall thins past 10 percent, so the blankholder is tuned against the same deviation map that measures springback, not set by habit.
On a progressive die, these levers sit inside station sequencing. The form station carries the compensation angle, the shutoff trims to final profile, and any coining strike needs its own station or a dedicated cam, which feeds the pitch decision covered in the progressive die layout guide.
Friction, Coatings and the Wear Drift
Friction is the hidden variable in every compensation number. During the bend, friction between the die radius and the sheet decides how much of the flange stretches versus slides, and that balance changes the stored elastic energy. TiN or CrN PVD layers of 2 to 5 micrometres cut the friction coefficient from about 0.15 on bare, lubricated tool steel to about 0.08, and the same die angle returns 0.5 to 1.5 degrees of recovery differently after the coating goes on.
Two consequences follow. First, compensate and tryout the die in the coating state it will run in production. A die corrected bare and then shipped to the coater drifts off the corrected angle, and the second rework is a self-inflicted cost. Second, keep lubricity in the measurement: springback measured on a dry test strip does not predict a wet production line, and a 0.07 shift in friction coefficient moves the flange as much as a 30 MPa yield shift.

Wear couples back into the springback discipline. On high strength grades, die wear at the radius runs on the order of 0.02 mm per 100,000 strokes, and a widened effective radius stores more elastic energy, so the flange angle drifts back toward the uncompensated side stroke by stroke. The deviation chart from tryout is therefore not a launch artifact; it is the baseline for production drift. Sample parts at defined counts, plot the angle, and schedule the regrind when the trend line meets the tolerance band, not when a part finally fails. A punch or die radius reground to nominal resets the angle for another 100,000-stroke cycle, and coating renewal rides with the regrind because grinding destroys the PVD layer on the refreshed surface.
Simulation and the Auto-Compensation Loop
Forming simulation predicts springback and, increasingly, rewrites the die surface to cancel it. Modern sheet metal solvers compute the elastic unloading after the forming solution, then apply an auto-compensation iteration: the die is virtually overbent, the spring is recomputed, and the surface updates until the predicted part sits on nominal. Typical toolchains converge the virtual die in 3 to 5 cycles in hours rather than weeks.
The honest limit is calibration. A simulation fed generic grade data from a handbook predicts the shape of the problem and misses its size by 20 to 40 percent, because it does not know your coil's actual yield spread, hardening exponent or friction state. A model fed the real stress-strain curve from the mill test and tuned on one physical tryout predicts the residual to within fractions of a degree. That is the difference that collapses the loop: with an uncalibrated model you are simulating a guess, and with a calibrated one the die is cut 80 percent compensated before steel ever touches a tryout press.
Ask your die maker which solver carries your grade, and whether the CAE compensation gets calibrated against the first physical try.
The Tryout Loop: Try, Measure, Compensate, Retry
The tryout loop is where compensation becomes accountable. The sequence is fixed: run the die, measure the trimmed part against nominal, compensate the geometry by the deviation map, and retry. Two to four iterations from a first try to print are typical, because each correction removes 60 to 80 percent of the residual error.
Run the loop with discipline rather than enthusiasm. Bring the production coil, or at least a coil with a matching yield band from the certificate, to every try. Run twenty shots before measuring, because the first five settle the lubricant film and the die temperature. Measure with one method per feature and record it: CMM stylus angles, or scanner best-fit angles, never a mix, because the two disagree by up to half a degree on tight radii. Log every compensation event against the deviation chart, so the die file shows how the angles were reached and what material state they were reached on.
Compensation between iterations is real machining, and the shop's tolerance stack decides whether it holds. Overbend corrections of 1 to 3 degrees on a die radius land in the hundredths of a millimetre on the cut surface, inside the 0.005 mm window a precision die shop works to, with EDM and jig-grind features at 0.002 mm. A shop that cannot prove that accuracy will chase springback with shims and hand stoning, and shims move with heat and press load while hand-worked angles carry no traceability.
Close the trial the way you would close a mold sampling. Run capability on the corrected die over a full run with two coil lots, issue dimensional reports against the deviation map, and update the drawing set so the compensated die surfaces become the reference geometry. The next regrind crew then inherits the angles, not the original design. The staged trial discipline in the mold trial guide applies feature for feature to dies.
A Compensation Decision Table by Grade and Stiffness
Pick the toolkit by two axes: what the grade springs, and how stiff the part is. A soft, flexible flange tolerates a larger angular error because assembly pulls it home. A stiff box section cannot be coaxed and must be compensated in the die. The table below maps common sheet grades to the first compensation move and its watch-out.
| Material and thickness band | Typical recovery at R/t of 4 | First compensation move | Watch-out |
|---|---|---|---|
| DC01 mild, 0.8 to 2.0 mm | 0.5 to 2 degrees | Overbend 1 to 2 degrees | Rarely critical, hold one iteration in the plan |
| HSLA 340 to 420, 1.0 to 3.0 mm | 2 to 4 degrees | Overbend plus radius undercut | Yield spread between lots up to 40 MPa |
| DP600, 0.8 to 2.5 mm | 3 to 6 degrees | CAE overbend, coining on short flanges | Springback varies with bend direction to rolling |
| DP980 to DP1180, 0.7 to 2.0 mm | 5 to 10 degrees | Calibrated simulation, overbend plus beads | Edge cracking limits inside radius, R/t at 1 to 1.5 |
| Martensitic MS1300 to MS1500, 0.7 to 1.6 mm | 8 to 15 degrees | Hot forming or multi-stage re-form, not single-strike coining | Springback so large that geometry alone cannot recover it |
| Stainless 304, 0.5 to 2.0 mm | 3 to 7 degrees | Overbend plus blankholder tension | Work hardening shifts recovery across the stroke set |
← swipe to scroll →
Table note: recovery bands are typical published and industry values for air-bent flanges at a bend radius four times the sheet thickness. Measure the actual coil lot before cutting compensated steel; every number here is a starting budget, not a guarantee.
Read the table against part stiffness, not just grade. A 1.0 mm DP980 bracket with six short flanges and two coining windows can be held to 0.5 degrees. A 0.7 mm DP980 member 600 mm long springs over the whole span, and no single-strike coining reaches the middle of it; that part needs beads, blankholder tension and a print-conversation at the DFM stage rather than another die rework.
What an Unmanaged Springback Loop Costs
Price the loop before it starts. An unmanaged springback correction burns 2 to 6 weeks of tryout time and 3 to 8 die reworks, and every week of that sits on top of a 2 to 5 week base die lead time. On a program with a fixed launch, the rework weeks are the weeks that buy overtime premiums, late-change fees and a parts shortage on the customer assembly line.
The reworks themselves add machining hours and cost: a die radius re-weld and regrind, an insert swap to reset an overbend, and blankholder force profiles tried on the press at 100 to 300 dollars an hour per setting.
Calibrated simulation plus one disciplined physical try cuts roughly half of that exposure. The die is cut 80 percent compensated, the first try measures a small residual instead of a structural miss, and two iterations close the gap. The buyer's question to any die maker is therefore simple and revealing: which springback method do you run, does the CAE get calibrated against your own tryout data, and what is the plan when the measured recovery lands outside the predicted band.
Holding Springback Down in Production
Launch is not the end of the springback problem; it is the beginning of a slower version of it. Three drifts move a compensated die off nominal in the field. Material drifts coil to coil, tracked by the mill certificate and a sample angle at every coil change. Friction drifts with lubricant viscosity, coolant carryover and coating wear, tracked by a quarterly angle check. The die itself drifts with radius wear of about 0.02 mm per 100,000 strokes on high strength grades, and each drift pushes the angle back toward the uncompensated side.
The control is the deviation chart carried forward from tryout. Sample defined shot counts, plot the angles per feature, and let the trend schedule the intervention. Regrind the radius when the trend meets the tolerance band, renew the coating with the regrind because grinding removes the PVD layer, and update the drawing set so the compensated geometry is the geometry the next crew inherits. A die maintained against its chart runs 100,000-stroke cycles at print. The same die maintained against failures accumulates angle creep until a customer reject forces the stop.
Built and maintained this way, a compensated die is an IATF 16949 process artifact, not a blacksmith's approximation: the compensation method, the calibration data, the deviation chart and the regrind trigger all belong in the tool file that audits ask to see. DieStrike builds stamping dies to 0.005 mm on critical form features with the compensation loop planned at DFM and the deviation chart handed over at sign-off, backed by 120+ machines and standard die components shipping in 3 to 7 days; the stamping die manufacturing service page carries the details.
Springback Compensation FAQ
Q1. How much springback should I budget before the first try?
On a bend radius four times the sheet thickness, expect roughly 1 to 2 degrees on mild steel, 3 to 6 degrees on DP600 class, 5 to 10 degrees on DP980 to DP1180 and 8 to 15 degrees on martensitic grades. Budget against the measured free-bend value of your coil, because the grade name predicts the shape of the problem and the certificate predicts its size.
Q2. Is overbending or coining the better fix?
Overbend is cheaper and applies to almost every angle, but it assumes constant recovery, so it needs lot tracking behind it. Coining at 1.2 to 1.5 times the forming force is more decisive because it removes the recovery at the source, and it is the right answer on short stiff flanges where the tonnage fits and no cosmetic face shows the strike.
Q3. How many tryout iterations are normal?
Two to four is typical, because each correction removes 60 to 80 percent of the residual error. A fifth iteration signals a systemic cause, usually coil-to-coil variation or a blankholder setting, and cutting more steel will not remove it.
Q4. Does simulation remove the need for a physical try?
No. A calibrated model, tuned on one physical tryout, removes most of the iterations that follow. An uncalibrated model using handbook material data misses the residual by 20 to 40 percent and just moves the argument from the press to the meeting room.
Q5. When does springback mean the part design is wrong?
When the required compensation exceeds the practical range, a recovery above 10 degrees that beads and coining cannot absorb, or when the compensated die angle makes the inside radius crack the edge. At that point the fix belongs on the drawing: move the bend line, thicken the local section, or accept a wider angle tolerance at the DFM review.
The Bottom Line
Springback is not a defect to be argued with; it is a measurable property of the coil, and the die either pays for it in the steel or pays for it in the tryout room. Measure the recovery on the real lot, compensate with the cheapest lever the geometry allows, and run the try-measure-compensate-retry loop with 20 shot settling and one measurement method per feature. Two to four iterations with a calibrated CAE model is a normal launch. Five weeks of rework against an uncalibrated one is the same physics priced without planning. Carry the deviation chart into production, let radius wear of 0.02 mm per 100,000 strokes set the regrind trigger, and keep the coating state of the die identical to the die you compensated.
KEEP READING
Related Reading
How to Design for High Strength Steel Stamping
Which grades crack, which spring, and what the part design must concede before the die is drawn.
Read articleArticleHow to Design a Progressive Die Layout
Station sequencing and carrier design, and where a form station earns its pitch.
Read articleArticleDie Protection Sensors in Progressive Dies
Misfeed and double-hit detection that keeps a bent punch from rewriting your bend angles.
Read articleServiceStamping Die Manufacturing
IATF 16949 die building with springback compensation planning, 2 to 5 week lead times and 120+ machines.
Read articleNEXT STEP
Ready to Start Your Mold?
Send us your element dimensions or part numbers — our team responds within 24 hours with pricing and lead time.

Written by
Ray ChanMold Buyer's Guide Author · Precision Mold Manufacturing Specialist. Ray helps global importers, distributors and OEMs source factory-direct molds and mold parts.