
How to Design Molds for Recycled Plastics: PCR Tooling Rules
Table of Contents
A PCR-blended connector housing that ran clean for two years can start throwing black specks at 40,000 shots, right after a supplier switches regrind batches. The mold did not change and the press program was logged as identical. What changed was the melt: 30% post-consumer polycarbonate carrying 20-60 ppm metal fragments, a batch-to-batch MFR spread of ±25%, and ash content near 0.3%. Recycled plastic mold design is the discipline of building tooling that absorbs that variability instead of discovering it at incoming inspection.
Post-consumer resin (PCR) and post-industrial resin (PIR) typically enter a mold at 15-50% of shot weight, and packaging tools can run beyond 70%. Recyclate is not virgin resin with a lower price tag. It carries contaminants, it holds moisture differently, it changes molecular weight every time the feedstock changes, and it often brings fillers from mixed collection streams. Each difference lands on a specific mold feature: gate land, hot runner valve pin, vent land, cavity surface, cooling circuit and ejection system. This guide maps each failure mode to the tooling decision that prevents it.
The Snapshot
- PCR and PIR loads run 15-50% of shot weight in most programs, with packaging tools reaching 70% or more.
- A batch-to-batch MFR swing of ±20-30% shifts cavity pressure by 10-20% and molded shrinkage by 0.2-0.6%.
- Metal and sand contamination at 20-200 ppm erodes gate lands 2-4x faster than virgin resin on unprotected steel.
- Gate lands and valve pins need HRC 58-62 steel plus 3-8 µm DLC or TD coating for PCR service above 250,000 shots.
- Black speck limits tighten to 3 or fewer specks above 0.3 mm per 100 cm² on visible surfaces, checked every 5,000 shots.
How Recycled Plastics Change the Mold Problem
Recyclate moves three mold variables at once: wall friction, melt pressure and thermal load. A virgin resin datasheet covers none of them at the tolerances a production tool needs. The feedstock arrives from bottle wash lines, crate regrind, e-waste ABS and industrial trim, and each stream carries its own filler, moisture and contamination profile.
Contamination load is the first difference. Mechanical recycling leaves metal fragments, sand and glass fines embedded in flake and pellet. Published recyclate specifications for PP and HDPE regrind commonly allow 20-200 ppm of non-melt foreign matter. Lines with only magnetic separation can deliver spikes well above that band. A 50 µm aluminum chip at 1,400 bar injection pressure behaves like a lapping particle traveling at 10-40 m/s through a gate.
Molecular weight moves with every feedstock change. Reprocessing shortens polymer chains, so recycled polypropylene often sits 10-25% lower in MFR than the same grade molded once. Mixed collection streams add a second effect: two PCR batches from different suppliers can differ by ±20-30% in MFR at identical nominal grade. That spread changes fill pressure, packing pressure and shrinkage together.

Thermal and surface behavior also shifts. Mineral fillers and ash raise thermal conductivity slightly and raise melt viscosity at the same barrel temperature. Molded parts from rPP and rPET typically show 0.2-0.6% more shrinkage scatter than virgin equivalents, and gate blush appears at lower fill speeds. The practical conclusion for tool design is simple: design to the worst end of the feedstock band, not to a nominal pellet certificate.
Contamination and the Wear It Causes
Wear in a PCR mold is abrasive, and it concentrates where velocity peaks. Gate lands erode first, then runner direction changes, then valve gate tips and narrow core features. On unprotected P20 at HRC 28-32, shops running 30% PCR PP at 1,000 shots per day measure gate growth of 0.02-0.05 mm inside 150,000 shots. That growth changes fill balance across a multi-cavity tool.
Size the gate for the dirty stream, not the clean one. PCR-grade tools should run gate cross sections 20-30% larger than the virgin equivalent, with a land depth of 0.8-1.2x wall thickness and a short land of 0.4-0.8 mm. Larger passages lower melt velocity and spread the abrasive load over more area, which cuts erosion rate roughly in proportion to the velocity drop.
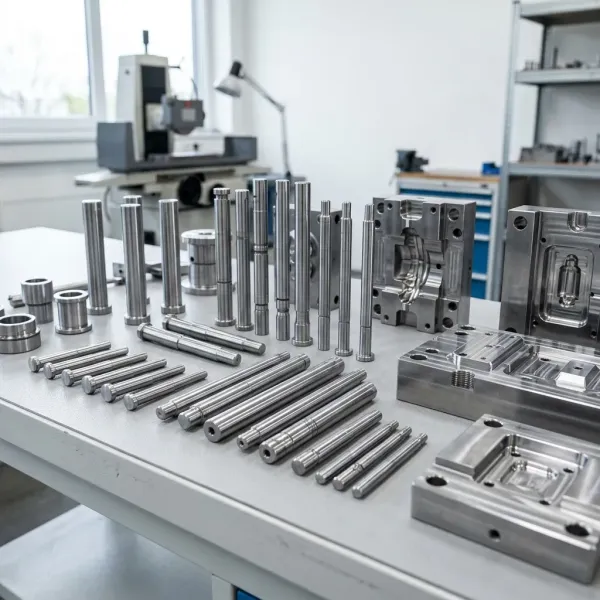
Put every wear zone in a replaceable insert. Gate lands, valve gate seats, runner crossovers and the last 10-15 mm of each hot drop should sit in inserts. Those inserts run through-hardened steel at HRC 58-62 or solid carbide. The insert must be removable with the mold in the press, because a wear part that needs a full teardown will not be swapped on schedule.
| PCR risk | Tooling response | Typical target |
|---|---|---|
| Metal and sand fragments | Carbide or hardened gate inserts, 20-30% larger gate section | Gate growth under 0.02 mm per 250,000 shots |
| Valve pin seat erosion | HRC 58-62 pin tip with DLC or TD coating, guided pin bore | DLC layer 3-8 µm, pin life 500,000 shots |
| MFR swing between lots | Wide process window, cavity compensation set at band midpoint | Shrinkage scatter held to 0.2-0.6% |
| Acid residue from PVC or PET | Stainless cavity steel plus Ni-P plating on gates and vents | Nickel-phosphorus layer 25-50 µm |
| Recycled glass fiber | Solid carbide at gates, hardened cores in high-flow zones | 500,000-1,000,000 shot tooling class |
| Black specks and deposits | Wider vents, polished cavities, shorter cleaning interval | 3 or fewer specks over 0.3 mm per 100 cm² |
← swipe to scroll →
Table note: contamination, MFR and shrinkage bands are typical industry figures for 15-50% PCR blends and vary with feedstock source quality.
Measure the wear, do not wait for it. Gate size and valve pin guide clearance should be recorded at T1 and re-measured every 50,000-100,000 shots. Once gate land growth passes 0.02 mm, fill balance across a 16-cavity tool drifts. Short-shot pressure then moves by 5-10%, and parts from the outer cavities start varying in weight.
Melt Viscosity Swing and Shrinkage Compensation
Shrinkage compensation on a recycled program cannot be a single scale factor. Cavity dimensions are cut once, while MFR and filler content move with every delivery. The mold design response is to pick compensation values from the middle of the expected band and then widen the dimensional strategy around them.
Set compensation from measured lots, not certificate values. Ask the molder for MFR data on the last 6-10 lots of the actual PCR grade, measured to ISO 1133 at the correct temperature and load. If the spread is ±25% around nominal, compensate at nominal and plan the tolerance budget for the full scatter. A 60 mm housing with 0.4% extra differential shrinkage moves 0.24 mm, which is 12x a ±0.02 mm positional tolerance.
Sample both ends of the band before steel acceptance. T1 should run one lot at high MFR and one at low MFR within the first week. Cavity pressure differences of 10-20% between those lots are normal. If the cavity cannot hold dimensions across both, the fix belongs in the tool: thicker walls near the gate, larger gates, or a hotter cavity zone.

Widen tolerance where function allows. Buying a PCR program at virgin-resin tolerances is the most common source of scrapped tools. Where the part has a non-critical cosmetic surface, releasing ±0.10 mm instead of ±0.05 mm absorbs MFR scatter without touching steel. Keep tight windows only on the features that mate, seal or transmit a signal.
Gate and Hot Runner Hardening for PCR
Gates and hot runner components take the highest velocity in the tool, so they take the most abrasion from a dirty melt. A PCR program that keeps virgin gate geometry will see fill balance drift within one production quarter. Four changes pay for themselves on any run above 250,000 shots.
Enlarge the gate section. Use a round or full-round gate where the part allows it, with a cross section 20-30% larger than the virgin-resin equivalent. Edge gates on PCR should run 0.8-1.2x wall thickness in depth, deeper than the 0.5-0.8x band used for clean unfilled resin. The larger passage cuts peak velocity by roughly a third and spreads the abrasive load across more steel surface.
Harden the land and the pin together. Gate lands belong in through-hardened inserts at HRC 58-62, or solid carbide when the program runs past 500,000 shots. Valve gate pins need the same treatment at the tip, plus a DLC layer of 3-8 µm or a TD coating of 5-10 µm. Pin-to-bore clearance should stay in the 0.01-0.02 mm band so contamination cannot migrate into the guide bore and gall the stem.

Protect the drop and the manifold. Nozzle tips at HRC 56-60 and hardened drop seats stop wear from migrating up into the manifold. On shared molds that run both virgin and PCR lots, add a purge sequence of 5-10 shots between material changes, and inspect the drop bore every 100,000 shots. Contamination that reaches a manifold bore turns a $3,000 component replacement into a $12,000-25,000 manifold rebuild plus two weeks of downtime.
Corrosion from PVC and Flame Retardant Residue
Mixed collection streams bring chemistry, not only abrasion. Traces of PVC in a PET or PP recyclate release hydrogen chloride above 200 °C, and that gas attacks steel wherever moisture condenses. Flame retardant additives in e-waste streams add brominated and phosphorus compounds that do the same job at cavity temperature.
Corrosion starts at the vents and the gate. Vent lands run 0.02-0.03 mm deep with sharp edges, so any pitting immediately changes gas escape and produces burn marks. Cavity surfaces near the gate lose polish and show dull patches within 100,000-200,000 shots on standard P20. Standard practice for PCR blends with unknown PVC content is stainless cavity steel such as S136 or 420SS at HRC 50-54. Add electroless nickel-phosphorus plating of 25-50 µm on gates, vents and any water-adjacent face.
Cooling circuits are the hidden corrosion site. Acidic condensate plus untreated water accelerates pitting inside channels, which reduces flow and lengthens cycle time before anyone sees a defect. Check cooling water pH every month and hold it in the 7-9 range. For PCR tools, plan a channel inspection and descaling every 6-12 months rather than the 24-month interval used on clean resin.
Cap the PVC content in the specification. Recycling standards for PET flake commonly limit PVC to 0.1-0.5% by weight. Write the same rule into a PCR purchase specification for PP and ABS streams. If the supplier cannot certify the limit, assume the worst case and specify corrosion-resistant steel and plating from day one.
Recycled Fibers: rPET and Glass-Reinforced PCR
Some PCR streams are inherently abrasive because they contain fibers. Bottle-derived rPET keeps short crystallite and fiber-like structures, and automotive recyclate often arrives as glass-filled rPP or rPA at 20-30% glass content. Recycled glass fiber is shorter and more contaminated than virgin chopped strand, so it does not polish a cavity the way virgin fiber does. It grinds it.
Wear rates double or triple. Industry testing on glass-filled recycled polypropylene shows abrasive wear 2-3x that of an equivalent virgin GF30 compound, mostly because mineral filler and metal fines travel with the fiber. Gate lands in hardened steel still erode, and cavity surfaces lose texture definition fastest at rib roots and near the gate.

Specify carbide where fiber velocity peaks. For recycled GF grades, carbide gate inserts become the default above 500,000 shots. Cores in high-flow zones need HRC 54-58 hardening, and any sliding shut-off face benefits from a PVD or nitrided surface. Deep ribs and thin cores in recycled GF parts should be built as separate inserts, since they are both wear items and crack risks.
Add draft and radius for fiber drag. Recycled fiber increases ejection force. Add 1-2° of draft beyond the standard allowance on deep walls and radius all internal corners at 0.5 mm minimum. Sharp corners concentrate both fiber impingement and stress, and they are where most cracked cores in recycled fiber tools begin.
Venting and Black Speck Control
Black specks are the visible symptom of degradation, and degraded material sitting in a vent land or gate corner produces them batch after batch. In PCR molding the problem compounds because ash and char from reprocessing act as nucleation sites for more deposits. Mold design and maintenance both have to answer for it.
Set vent depth by resin family. PP and PE blends run vents at 0.02-0.03 mm of depth. PA, PET and PC blends run tighter, at 0.015-0.02 mm, because their lower melt viscosity flashes sooner. Vent land length stays 2-3 mm, vent width 3-6 mm, and vents must be cut every 25-50 mm along the last-fill flow path. Add a vent at every weld line location and at the end of each runner.
Shorten the cleaning interval. A virgin-resin tool may run 20,000-50,000 shots between vent cleaning and cavity polish. A PCR tool at 30-50% regrind typically needs that work every 5,000-10,000 shots. Build the maintenance plan around that shorter interval from the start, and specify cavity polish at Ra 0.2-0.4 µm on visible surfaces so deposits release instead of bonding.
Use purge and limit samples. A 5-10 shot purge with a commercial purging compound before every restart removes carbon that would otherwise release as specks. Define the acceptance limit visually. A common PCR automotive limit is 3 or fewer specks larger than 0.3 mm per 100 cm². Judge them against photographed limit samples under 800-1,000 lux inspection lighting.
Cooling and Cycle Time Shifts with Regrind
Recycled feedstock changes how heat leaves the part. Mineral ash and filler raise thermal conductivity slightly, while higher viscosity and lower melt temperature stability push the other way. The net effect on a well-designed tool is a small cycle-time increase, not a redesign.
Expect a 5-15% cycle increase. PCR polypropylene commonly runs 0.20-0.22 W/m·K against 0.22-0.24 W/m·K for the virgin grade, and molded density scatters between lots. Together with longer hold time to control sink, that adds 5-15% to cycle on the same mold. Budget the machine time before the RFQ, not after T1.

Keep cooling in turbulent flow. Channel bores of 8-12 mm with water at 2-4 m/s hold Reynolds numbers above 10,000, which is where heat transfer stays predictable. Aim for cavity surface uniformity within ±2-3 °C. Filler-rich PCR absorbs more heat at the gate, so the gate zone needs its own circuit or a baffle so the hottest area gets the coldest water.
Clean for conductivity, not for looks. Scale of 0.1-0.2 mm inside a cooling channel can cut heat transfer by 10-20% and add seconds to the cycle. Schedule a flow and temperature check every 6 months on PCR tools, and compare measured return-water temperature against the T1 baseline. A rise of 3 °C or more on the same settings signals fouling that the eye will never find.
Tolerances and Appearance Acceptance Criteria
Recycled programs fail at the acceptance gate more often than at the press. The dimensional and cosmetic criteria agreed before steel is cut decide whether a tool that holds ±0.05 mm on virgin resin also passes on 40% PCR. Two rules keep the argument short: tighten only functional features, and write numeric cosmetic limits into the drawing.
Spend tolerance where it matters. Assign a Cpk target of 1.33 or better to mating, sealing and connector-interface features, and release cosmetic-only surfaces to ±0.10-0.15 mm. Reference datums must be on the part, not on a fixture. PCR lots shift wall thickness slightly, and fixtures built to a nominal part will mask the drift. A full tolerance stack on the critical features belongs in the review pack before cutting.
Make appearance measurable. Gray or black PCR grades hide flow marks but show specks. Natural and light colors show both. The table below lists the acceptance bands most PCR programs use, built on public test methods rather than shop opinion.
| Attribute | Reference method | Typical PCR limit |
|---|---|---|
| Color difference | ASTM D6290 / CIELAB, 3 specimens averaged | ΔE 1.5 or less against the approved standard |
| Black specks, visible surface | Visual against photographed limit samples | 3 or fewer specks above 0.3 mm per 100 cm² |
| Ash content of feedstock | Thermogravimetric ash test on incoming lots | 0.5% or less for 30% PCR polypropylene |
| Moisture before molding | Karl Fischer or loss-on-drying per lot | 0.2% or less for PCR PA, PET and PC |
| Melt flow rate | ISO 1133 at the grade temperature and load | Within ±20% of the declared nominal |
| Critical dimensions | Sampled inspection plan, capability study | Cpk 1.33 or better on functional features |
← swipe to scroll →
Table note: limits are typical acceptance bands used with 15-50% PCR content and should be confirmed against the molder's material specification.
Trigger engineering review on drift. Any lot measuring ΔE above 2, ash above 1.0% or moisture above 0.4% should stop the run and trigger an engineering review, not a press adjustment. Those three readings predict dimensional and cosmetic failure within a few thousand shots, and they cost $50-150 per lot to test.
Lot Traceability and Recycled Content Rules
Recycled content is now a documented claim, not a marketing line. Public packaging regulation in the European Union sets recycled content targets for plastic packaging and requires recyclability by design. Brand owners pass those obligations down to molders and tooling suppliers as reporting duties. A mold that cannot be tied to a material lot cannot support that claim.
Keep a four-part lot record. For every PCR delivery, store supplier name, lot code, recycled percentage, and the measured MFR, ash and moisture values. Keep a 500 g retention sample per lot and hold records for 12-24 months. When a customer asks which recycled content ran in a given week, the answer must come from a file, not from memory.
Mark traceability into the tool. Engrave a cavity identification number in every cavity, and where the part allows it, mold the date and recycle marks so each shot carries its own origin. Register the tool in a maintenance log with a cycle counter, so shot count drives the vent cleaning, gate measurement and pin inspection intervals described above.
Simplify the stream count. Programs that run three recycled suppliers on one tool struggle to control MFR scatter. Two qualified streams with documented MFR bands keep the process window workable and make claims defensible. If a new stream is needed, run it through the same lot record and the same T1 validation before it touches production. Material choice itself is the upstream decision here, and the resin family rules in our material selection guide set the baseline before any tooling choice is made.
DFM Checkpoints for PCR Tooling
Every recycled program should clear the same gates before steel is ordered. These six checkpoints catch the failures above at the drawing stage, where a correction costs hours instead of weeks of downtime.
1. Declare the recycled content and stream. The RFQ must state recycled percentage, PCR or PIR, source stream and the PVC cap. A 15% closed-loop PIR and a 50% mixed PCR tool are different tools. A program that may raise recycled content later must be built to the worst case at day one.
2. Map the wear zones. Mark every surface where melt velocity exceeds 2 m/s: gate lands, runner crossovers, valve pin tips, narrow ribs and sliding shut-offs. Each zone gets an insert, a hardness and a coating decision. Hardness and coating options for acid-bearing blends are covered in our corrosive resin steel guide.
3. Set compensation from measured lots. Use the molder's MFR history for the actual grade, not the compound datasheet, and compensate the cavity from the middle of that band. Ask for at least 6 prior lots of data. Datasheet averages hide 0.2-0.6% shrinkage scatter between batches.
4. Size gates and vents for the dirty stream. Confirm a 20-30% larger gate section, edge gate depth of 0.8-1.2x wall, vent depth inside the resin band and vent spacing every 25-50 mm along the last-fill path.
5. Plan the corrosion and insert strategy. Stainless cavity steel plus nickel-phosphorus plating where PVC content is unknown. Carbide or HRC 58-62 inserts at wear zones, and every wear insert removable with the mold in the press. Spares should be quoted with the tool.
6. Agree the acceptance standard in writing. Color, speck count, ash, moisture and capability targets as shown above, plus a documented route for a non-conforming lot. Wall and draft rules that keep recycled parts moldable are set out in our moldability design rules.
DieStrike returns DFM feedback within 24 hours on recycled-content programs, covering these six gates plus venting, ejection and cooling layout. Production tooling is built to ±0.005 mm mold accuracy, with cavity inserts and pins heat treated to HRC 62. Standard components ship in 3-7 days for tooling that serves connector OEMs including TE Connectivity, Amphenol and Luxshare.
FAQ
Q1. Can I run PCR in an existing mold built for virgin resin?
For trials under 50,000 shots, yes, with expectations managed: gate lands will erode and cavity polish will dull. For production, retrofit hardened inserts at the gate and wear zones first. That retrofit typically costs 8-20% of a new tool and multiplies usable life 2-4x on a 30% PCR blend.
Q2. How much more does a PCR-ready mold cost?
Hardened inserts, stainless cavity steel, plating on gates and vents, and additional vents add a typical 10-25% to tool cost. On a program running 500,000 shots at 1,000 shots per day, that premium is recovered quickly. One avoided gate replacement shutdown and stable fill balance across the cavity set pay for it.
Q3. What hardness and coating should the gate insert have?
Use through-hardened steel at HRC 58-62 for most PCR work, or solid carbide above 500,000 shots or with recycled glass fiber. Valve pins and sliding faces benefit from DLC at 3-8 µm or TD at 5-10 µm, which extends coated zones 2-4x in abrasive service.
Q4. How do I hold a ±0.05 mm window at 40% recycled content?
Compensate the cavity from a measured MFR band rather than a datasheet. Sample both the high and low MFR lots at T1, and keep cooling uniform within ±2-3 °C. Where that still misses, widen the cosmetic-only features to ±0.10-0.15 mm and keep the tight window on mating features only.
Q5. What black speck limit should go into the inspection standard?
For visible automotive and appliance surfaces, 3 or fewer specks above 0.3 mm per 100 cm² is the working band. Judge against photographed limit samples under 800-1,000 lux lighting. Pair it with a 5,000-10,000 shot vent cleaning interval so the limit holds between audits.
The Bottom Line
Recycled resin punishes soft gate steel, tight cosmetic tolerances and long cleaning intervals. Hardened insert gates at HRC 58-62, 20-30% larger gate sections and compensation from measured lots change the outcome. Add a 5,000-10,000 shot maintenance rhythm and a 150,000 shot problem tool becomes a 500,000 to 1,000,000 shot asset. DieStrike builds IATF 16949 production molds to ±0.005 mm mold accuracy with 24-hour DFM feedback on recycled-content programs. Send us your PCR part drawing for a wear-zone and gating review before you commit to steel.
KEEP READING
Related Reading
How to Design Molds for Glass-Filled Resins: Wear, Gates and Steel
Gate insert hardness, DLC coating payback and directional shrinkage rules for abrasive filled resins.
Read articleArticleMold Venting: Depth, Location and Design Rules
Vent depth bands by resin family, spacing rules and the last-fill locations that trap gas.
Read articleArticleHow to Maintain a Mold: Weekly/Monthly/Annual Schedule
A weekly, monthly and annual inspection schedule that catches wear before parts drift.
Read articleServiceMold Design & DFM
24-hour DFM feedback on gating, steel, cooling and tolerances before the first cut.
Read articleNEXT STEP
Ready to Start Your Mold?
Send us your element dimensions or part numbers — our team responds within 24 hours with pricing and lead time.

Written by
Ray ChanMold Buyer's Guide Author · Precision Mold Manufacturing Specialist. Ray helps global importers, distributors and OEMs source factory-direct molds and mold parts.