
How to Design Parting Lines: Placement and Shut-Off Rules | DieStrike
Table of Contents
A buyer approved a cosmetic cover with the parting line running across the middle of the face. The model split there, so the tool split there. The first article showed a 0.08 mm step and flash at 0.03 mm on a class A surface. Sorting cost two shifts, and the tool went back for a 0.5 mm grind and a full re-spot. The repair added $4,200 and 9 days to a 4-week mold schedule.
The parting line is a mold design decision, not a leftover CAD split line. It fixes where the two steel halves meet, how much bearing area seals the cavity, and where the witness line lands on the part. A line placed on the wrong face turns a $30,000 mold into a flash machine. This guide covers placement rules, shut-off geometry, venting, and the DFM checks that catch the errors before steel is ordered.
DieStrike designs and builds production molds under IATF 16949 with 120+ machines. Mold size precision holds to ±0.005 mm, and critical geometry to ±0.002 mm. A production injection mold ships in 2-4 weeks, and DFM feedback returns within 24 hours.
The Snapshot
- Flash is visible on class A surfaces at a 0.02-0.05 mm gap at the parting line, typical.
- Seal-off land width runs 3-5 mm minimum, typical. Below 3 mm, edges crush or chip under clamp load.
- Sliding shut-offs carry 0.01-0.03 mm preload and faces angled 5-7 degrees minimum, typical.
- Vent depth ranges from 0.01 to 0.05 mm depending on resin, typical, with land length of 1-3 mm.
- DieStrike machines mold geometry to ±0.005 mm, with ±0.002 mm on critical features, and returns DFM feedback in 24 hours.
What the Parting Line Controls
The parting line controls four things at once. They are flash, appearance, release, and mold cost. Each one has a number attached, and the parting line decision sets all four before any steel is cut.
Flash Control
Flash starts when the steel halves separate under cavity pressure. Typical injection pressure in the cavity runs 300-800 bar, and it pushes the halves apart wherever the bearing area is short. A separation of 0.02-0.05 mm is enough for most resins to leak through, which is why that gap shows up as a visible fin. The seal land, clamp force, and steel stiffness all fight that separation together.
Appearance and the Witness Line
Every parting line leaves a witness mark on the part. A step of 0.05 mm between the halves is visible from arm's length on a gloss surface, and textured surfaces show mismatch at 0.02 mm. Class A tooling is spotted to a zero-step condition at T1. Any later grinding of the parting surface re-opens the mismatch and can change the part's edge geometry by 0.1 mm or more.
Release and Draft
The parting line defines the pull direction and the draft system. Every surface that opens against the line needs 0.5-2.0 degrees of draft, typical, or the part sticks on the wrong half. A line moved 10 mm across a face can change which half holds the part. The ejector layout, draft map, and texturing plan all follow that shift.
Mold Cost and Lead Time
A flat parting line is the cheapest surface to machine and fit. A stepped or contoured line adds machining time, hand spotting, and tryout risk. Typical cost premiums over a flat line run 15-25 percent for stepped geometry and 30-60 percent for a fully contoured line. Spotting hours climb from 4-8 on a flat line to 20-40 on a contoured one, typical shop figures. These are the numbers buyers see when the quote lands.
Parting Line Placement Rules
Placement rules exist to keep the witness line off visible faces, off sealing surfaces, and on the shortest possible steel path. Run each rule before you lock the split in the 3D model. A drawing change is free. A parting surface change after hardening is not.
Follow the Outermost Contour
Set the line at the widest silhouette of the part, seen from the pull direction. That keeps the cavity wall draft positive and lets both halves release without drag. The seal land follows the envelope 3-5 mm outboard of the cavity edge, typical, so the steel bearing area surrounds the part completely.
Hide the Witness Line
Put the line on an edge, a bottom rim, or an inside corner where the eye does not rest. When the part needs a visible seam, step the line onto a chamfer or a groove that is 0.3-0.5 mm deep. A mismatch of 0.05 mm is then lost in the shadow line instead of sitting on a flat face. Cosmetic requirements should state the allowed witness zone on the print, or the mold maker will guess.
Stay Off Sealing and Bearing Faces
Never run a parting line across a surface that seals or carries load in the assembled product. A 0.05 mm witness or a 0.02 mm flash fin on a gasket face becomes a leak path. On snap-fit or press-fit features, the line adds a raised edge that changes the interference fit by 0.1-0.2 mm, typical, and that changes assembly force.
Respect the Draw Direction
The line should sit in one plane wherever possible. When the part demands height changes, step the line or contour it, and accept the extra machining. Every deviation from the plane must still allow draft of 0.5-2.0 degrees on both halves, typical. A zero-draft vertical shut-off that parallels the draw direction wears and gallops through the mold's life.
Flat vs Stepped vs Contoured Parting Lines
Three parting line geometries cover most production tools. Flat lines stay in one plane. Stepped lines change height in discrete levels. Contoured lines follow a 3D surface of the part. Each one changes machining cost, sealing risk, and maintenance, so the choice belongs in the DFM review, not on the shop floor.
| Characteristic | Flat Parting Line | Stepped Parting Line | Contoured Parting Line |
|---|---|---|---|
| Machining cost index | 1.0x baseline | 1.15-1.25x | 1.30-1.60x |
| Sealing risk | Lowest | Low at steps, corners seal at 0.005-0.01 mm flatness | Highest, full contour must fit |
| Hand spotting time | 4-8 hours | 10-20 hours | 20-40 hours |
| Maintenance | One flat grind resets the land | Each step ground and re-spotted | Re-cut per contour, weld risk rises |
| Typical application | Covers, housings, single draw direction | Boxes with flanges, multi-height walls | Class A trims where the line follows a styling radius |
← swipe to scroll →
Table 1. Flat, stepped, and contoured parting lines compared on cost, sealing, and upkeep. All values are typical industry figures. Final selection depends on part geometry, resin, and annual volume.
Choose the flat line when the part allows it. The seal is the easiest to fit, and a future grind of 0.05-0.10 mm resets the whole land in one pass. Stepped lines earn their cost when a housing has flanges at different heights. The step keeps the line at the part contour instead of dragging it across a visible wall.
Contoured lines carry the highest risk. The two halves must match across a freeform surface, and contact has to land within 0.005-0.01 mm of fit, typical. Small mismatches open as vent-sized gaps of 0.02-0.05 mm, and those become flash at the exact spots the part cannot tolerate. Contours are justified only for styling surfaces where a straight line would cut across a visible radius.
Stepped and contoured lines also need more rigidity. Every vertical step face pushes against the mating half under cavity pressure of 300-800 bar, typical. Toolmakers support each step with 5-10 mm of bearing land. They relieve the rest of the surface by 0.5 mm, so only the sealing rim carries load.
Shut-Off Design Basics: Width, Flatness and Direction
A shut-off is any place where mold steel seals against mold steel to block the melt. It can be a land around the cavity, a vertical face on a core, or a pin sealing through an opposite wall. Three numbers govern every shut-off. They are width, flatness, and direction.
Minimum Land Width
Seal-off land runs 3-5 mm wide minimum around a standard cavity, typical. Inserts and small cores use at least 5 mm where the drawing allows. Wide bearing zones on large automotive molds run 25-35 mm. The inner and outer edges are relieved by 0.5 mm, so only the sealing band contacts. Below 3 mm, the edge crushes under clamp force of 200-500 tons, typical, and chips during handling.
Flatness and Parallelism
The land must sit flat against its partner to block melt at 300-800 bar of cavity pressure. Target flatness runs 0.005-0.01 mm across the land width, typical. Stepped faces need the same flatness plus squareness to the main plane within 0.005 mm per 25 mm of height. Grinding marks should run across the land, never toward the cavity, so any scratch does not become a melt channel.
Direction and Draft
Every shut-off face that opens in the draw direction needs angle. Vertical telescoping shut-offs carry 3-5 degrees minimum, typical, so the faces approach without rubbing their full length. Faces angled below that gall within 10,000-50,000 cycles, typical, and start leaking resin. Toolmakers also avoid knife edges on shut-offs by adding a 0.1-0.2 mm edge radius, typical, because a zero-radius edge chips at the first hard close.
Interference vs Clearance Shut-Offs
Moving shut-offs come in two fits. Clearance fits let steel slide with a small gap. Interference fits press one surface against another at full close. Picking the wrong fit is the fastest way to get flash on one side or galling on the other.
Clearance Fits for Sliding Contacts
Slides, lifters, and telescoping cores run on clearance. Typical clearance is 0.02-0.05 mm per side, which keeps sliding faces from galling while the mating land does the sealing. The clearance number must respect the resin's flash margin. Low-viscosity resins flash at smaller gaps, so their sliding hardware uses the tight end of the band and hardened steel.
Interference Preloads
Sealing surfaces that do not slide during the shot run with a small interference so no gap survives at full close. Precision sliding shut-offs carry 0.01-0.03 mm of preload, typical. The crush of that preload closes microscopic mismatch and stops melt from entering the interface. Too much preload above 0.05 mm bends the shut-off, opens the opposite side, and starts a leak of its own.
The Angle Rule for Sliding Shut-Offs
Sliding shut-off faces need 5-7 degrees of angle minimum, typical, relative to the direction of travel. At that angle the faces separate as the slide moves, and they touch only at full stroke. Below 5 degrees, the faces wipe each other across the whole length, wear plating, and gall. Industry rule of thumb floors general shut-offs at 3 degrees, and toolmakers run 5-7 degrees wherever wear life matters.
Verify the fit choice at T1. A hard close with clean contact confirms the preload. A drag mark or a galling streak means the fit needs clearance or the angle needs another degree.
Steel Selection for Shut-Offs
Shut-off steel carries contact stress, sliding wear, and repeated closing impacts. Soft steel in a shut-off wears first, and worn shut-offs flash. Hardness and grade selection start with the resin, the cycle count, and the part volume.
Prototype and low-volume tools run pre-hardened P20 at HRC 28-32, typical. Production shut-offs step up to hardened tool steel at HRC 46-62, typical. DieStrike heat treats cavity geometry to HRC 62, which gives shut-off lands long wear life under 200-500 ton clamping. Corrosive resins and optical parts move to stainless grades at HRC 48-52, typical.
| Steel Grade | Hardness (typical) | Shut-Off Role | Selection Driver |
|---|---|---|---|
| P20 | HRC 28-32 | Low-volume and prototype lands | Lowest cost, easy hand fitting |
| 718H or 738 | HRC 33-38 | Mid-volume cavity blocks | Machinable pre-hard, stable in polish |
| H13 / SKD61 | HRC 46-52 | Shut-off inserts, slides, lifters | Hot strength, resists edge crushing |
| S136 / 420SS | HRC 48-52 | Corrosive and optical shut-offs | Corrosion resistance, polish to Ra 0.01 µm |
| Cavity steel at DieStrike | HRC 62 | Production cavity and land geometry | Wear life at 200-500 ton clamp duty |
← swipe to scroll →
Table 2. Shut-off steel grades and hardness by duty. All hardness values are typical industry figures except DieStrike cavity heat treatment at HRC 62.
Surface treatment extends shut-off life when the grade cannot. Nitriding adds a case of 0.1-0.4 mm at 900-1,200 HV, typical, and chrome or PVD coating protects sliding faces. Treated shut-offs commonly run 2-3 times longer between re-grinds, typical. Coatings stay off sealing lands that must be hand-fitted, because coating thickness of 0.003-0.01 mm, typical, changes the fit dimension.
Replaceable wear points belong in inserts. A shut-off corner that sees the heaviest crush should be a separate insert, so a worn land is swapped instead of welded. Custom inserts follow the mold build schedule, and DieStrike ships standard mold components in 3-7 days.
Venting at the Parting Line
The parting line is the first and cheapest place to vent a cavity. Air and molding gases escape through shallow channels cut across the seal land, before the melt front reaches the end of fill. Vent depth must stay below the resin's flash margin, or the vent becomes a flash source.
| Resin | Vent Depth (mm, typical) | Vent Land Length (mm, typical) | Note |
|---|---|---|---|
| POM (acetal) | 0.01-0.025 | 1-3 | Flash-prone, tight depth window |
| PA (PA6 / PA66) | 0.01-0.02 | 1-3 | Low viscosity, precise vents required |
| PP / PE | 0.02-0.04 | 1-3 | Easy flow, monitor flash margin |
| ABS / PS | 0.02-0.04 | 1-3 | High gas load, vent end-of-fill zones |
| PMMA | 0.03-0.05 | 2-3 | High viscosity, deeper vents allowed |
← swipe to scroll →
Table 3. Parting line vent depths and land lengths by resin. All values are typical industry figures and must be verified against the exact resin grade and its datasheet.
Vent geometry beyond depth follows three rules. Channel width runs 4-8 mm per slot, typical, spaced 20-40 mm apart along the seal land. The shallow land section runs 1-3 mm outboard of the cavity edge. The channel then opens into a relief step of 0.3-0.5 mm depth to atmosphere. That relief keeps the long channel from clogging and gives the trapped gas room to dump.
Vents go where the air goes. Mold filling analysis marks the last-fill points, weld line tips, and rib ends, and those get first priority on the parting surface. Deep ribs over 8 mm, typical, need venting at their roots as well. Vents are cut only after the seal land is spotted, so the shallow channel never breaks the sealing band.
Machining and Fitting the Parting Line
A parting line is machined, hardened, and then fitted by hand before it ever sees resin. The fit quality at T1 is set in the toolroom, not in the mold design review. Each step has a tolerance and a verification method.
Machining the Seal Land
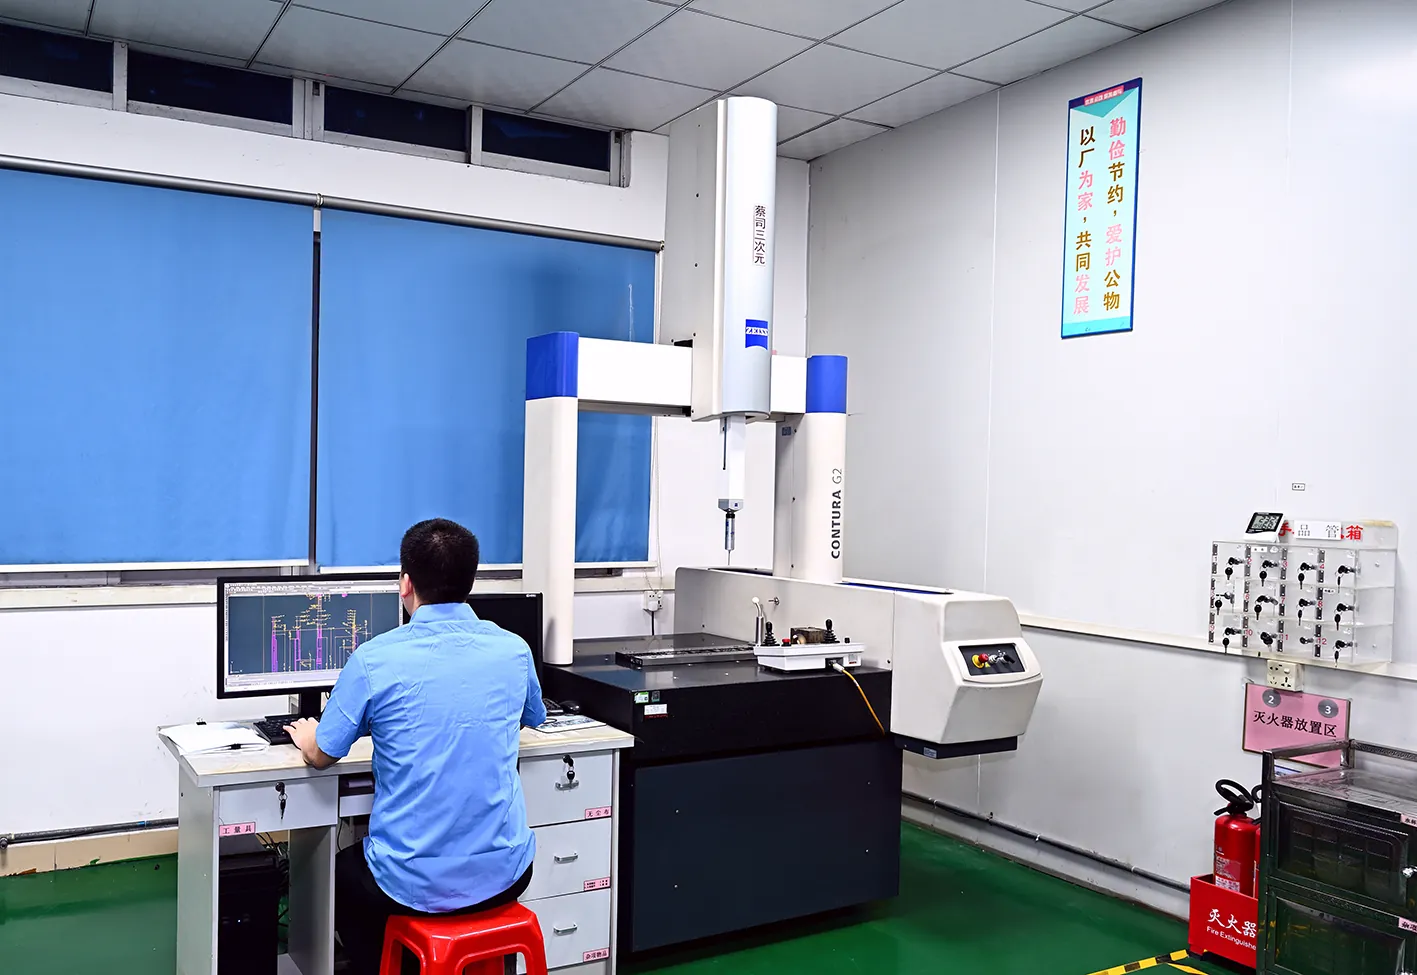
CNC milling roughs and finishes the flat parting surface in DieStrike's mold making plant, leaving 0.1-0.2 mm of stock for grinding, typical. The machine holds position to ±0.005 mm, and critical shut-off geometry to ±0.002 mm. After heat treatment to HRC 46-62, the land is ground flat, because grinding removes heat treat distortion that milling cannot correct.
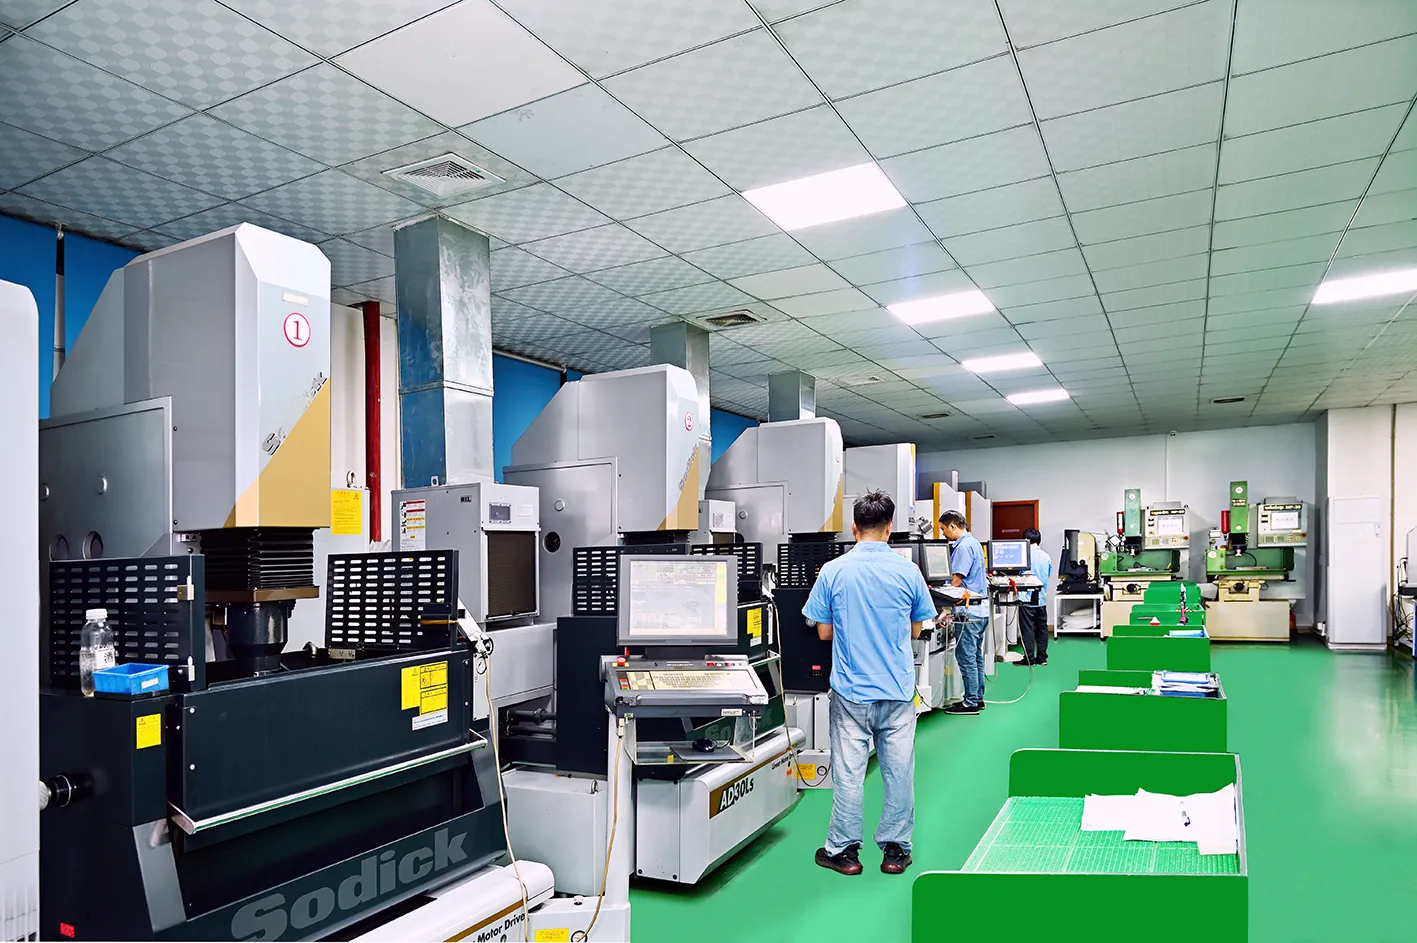
Stepped and contoured lines cannot always be ground flat. Sinker EDM cuts the steps and corner details in the hardened block. Wire EDM trims the vertical faces where a core seals through a wall. EDM leaves a recast layer of 0.005-0.02 mm, typical, on every spark-cut surface. That layer cracks and wears early, so seal faces get ground or polished until the recast layer is gone.
Spotting and Fitting
Fitting starts with spotting compound on one half and a controlled close on the other. Contact marks show where the steel touches and where it does not. Target contact runs 80-90 percent of the land area, typical, before the first tryout. Toolmakers remove high spots in passes of 0.01-0.02 mm and re-check after each pass.
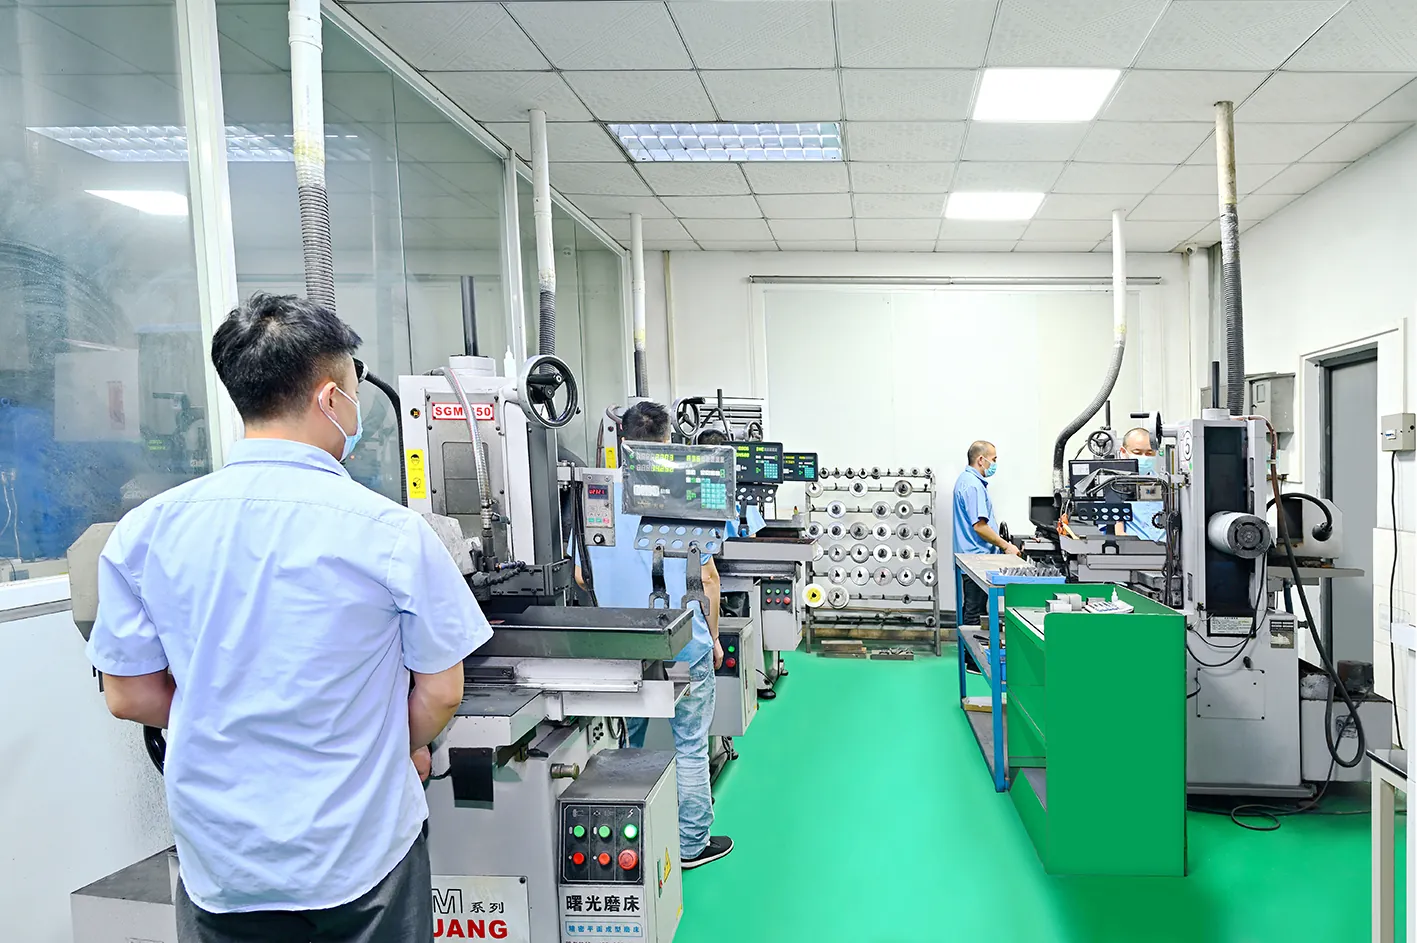
Land flatness is checked against a surface plate with a 0.005 mm indicator sweep. Steps are verified for squareness to the main plane. Every grind or hand pass removes material and changes the land height. The toolmaker records each removal and keeps the two halves matched within 0.02 mm of nominal, typical.
Verifying the Result
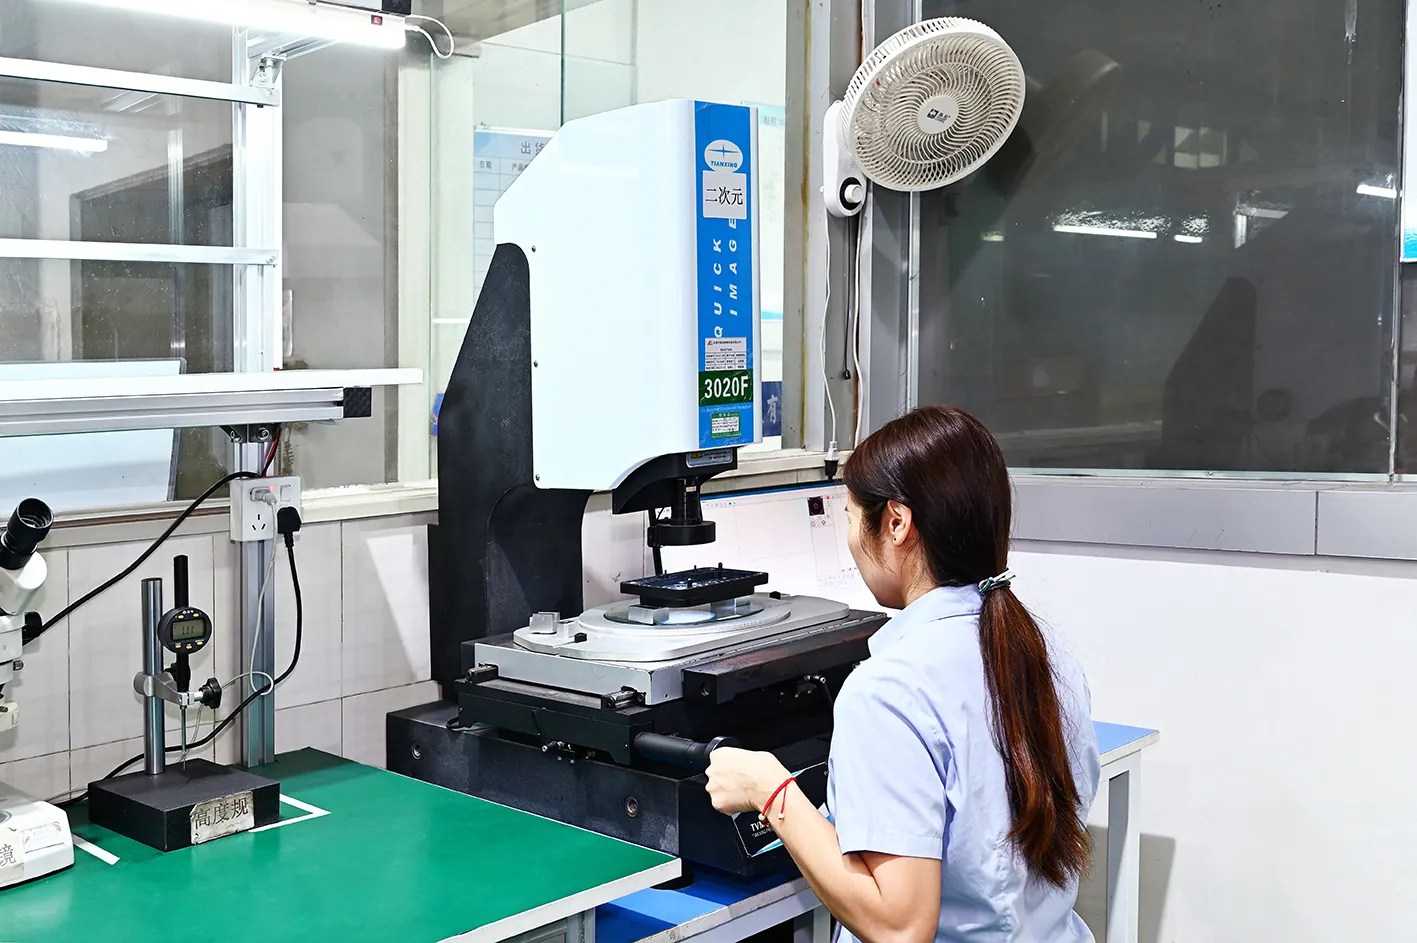
Before the mold leaves the bench, the parting line is measured, not guessed. A CMM sweep of the land position and a comparison of the two halves confirm mismatch targets. Critical shut-off geometry is verified to ±0.002 mm at DieStrike. A clean blue-check contact pattern and a zero-step condition at the cavity edge are the pass criteria for release to T1.
Common Parting Line Defects and Fixes
Parting line defects show up in tryout and again late in a mold's life. Most trace back to land wear, crushed edges, or fit loss. Each defect has a measurable trigger and a repair path.
Flash at the Parting Line
Flash appears when the steel halves separate past the resin's flash margin. Triggers include a crushed land, mold deflection under cavity pressure, and clamp force drift below requirement. Flash of 0.02-0.05 mm is visible on class A surfaces, and it grows with every shot once the land starts peening. The standard fix is a re-grind of the land by 0.05-0.10 mm, a re-spot, and a clamp tonnage check with 10-20 percent margin, typical.
Peening and Impression Marks
Hard particles and closing impacts dent the land. The dents transfer to the part as raised marks of 0.05 mm or more. A particle of 0.1 mm between the halves at close is enough to mark a soft P20 land. Light marks are polished out to a depth of 0.02-0.05 mm. Deeper damage on a hardened land needs a weld repair with 0.5-1.0 mm of stock allowance, typical, before re-machining.
Chipped and Broken Edges
Shut-off edges chip when lands run below 3 mm, when the mold closes on a foreign object, or when a slide returns out of position. A chip of 0.2-0.5 mm on a seal edge opens a leak path that flashes on every shot. Small chips are blended and re-spotted when they stay clear of the cavity edge. Structural edge damage gets welded, re-heat-treated to match, and re-cut, with the weld recorded in the mold book.
Mismatch and Steps Between Halves
A step between core and cavity at the parting line reads as a molded ledge on the part. Steps above 0.05 mm are visible on gloss parts, and textured parts show steps at 0.02 mm. Mismatch comes from uneven land grinding, guide wear, or a sagging half. The repair is re-fitting the land and correcting the guide clearances, then re-verifying on the CMM.
Schedule the parting line check like a calibration. Every 50,000 cycles, typical, measure land condition, mismatch, and clamp repeatability. A land that loses 0.01-0.03 mm of height shows up in the measurement before it shows up as flash on the line.
DFM Checks Before the RFQ
Parting line errors are cheapest at the drawing stage and most expensive on the tryout floor. A DFM review that maps the parting line, its shut-offs, and its vents before the RFQ prevents re-cut steel and schedule slips. DieStrike returns DFM feedback within 24 hours on a complete part package.
The mold design review flags every split decision against the numbers above. It checks witness line placement against the cosmetic class, land width against the clamp load, and vent depth against the resin. Where the part fights the rules, the review proposes the redesign or the cost, before steel is ordered.
- Part 3D model with the pull direction marked and draft shown at 0.5-2.0 degrees, typical, on every outer wall.
- Cosmetic class and the allowed witness line zone. State whether a 0.05 mm step is acceptable on any surface.
- Seal-off land budget. Confirm 3-5 mm of land, typical, fits the part contour at every point of the split.
- Wall thickness map, because projected area times 300-800 bar of cavity pressure, typical, sets the clamp and the land load.
- Resin grade and datasheet, so vent depth of 0.01-0.05 mm, typical, and steel hardness are matched to flash margin.
- Functional faces that must never carry a witness line, including gasket seats, bearing surfaces, and snap features.
- Annual volume and run size, which decide P20 vs hardened shut-off steel at HRC 46-62 and the coating plan.
- Tolerance callouts on shut-off features, so the toolmaker quotes the ±0.005 mm machining and the fitting hours honestly.
DieStrike runs this review inside its mold design and DFM service, and the parting line verdict comes back with the quote. Molds ship in 2-4 weeks for injection tooling, and precision holds at ±0.005 mm, with ±0.002 mm on critical geometry.
Frequently Asked Questions
Q1. What is the minimum shut-off land width for a production mold?
Run 3-5 mm minimum around a standard cavity, typical. Inserts and small cores use at least 5 mm where space allows. Large automotive bearing zones reach 25-35 mm with the remainder relieved by 0.5 mm. Below 3 mm, the edge crushes under clamp and chips during handling, so the land budget belongs in the DFM review.
Q2. How much does a stepped parting line add to mold cost?
Machining runs 15-25 percent above a flat line, typical, and hand spotting climbs from 4-8 hours to 10-20 hours. A fully contoured line runs 30-60 percent higher in machining and 20-40 hours of spotting, typical. Buyers who move the line to a single plane usually recover 10-20 percent of the mold price.
Q3. Why does flash appear at one spot after 50,000 shots?
The land at that spot has worn or peened below the resin's flash margin. Land height loss of 0.01-0.03 mm, typical, opens the gap past 0.02-0.05 mm, and flash follows. The repair is a re-grind of 0.05-0.10 mm, a re-spot, and a clamp check. Schedule the check at every 50,000-cycle service interval.
Q4. Can the parting line be moved after the mold is cut?
Small moves of 0.5-1.0 mm are possible by grinding and re-spotting when the line stays on the existing parting surface. Larger moves mean welding, new inserts, or a new cavity block, and they cost more than the original split decision. That is why the placement rules run before steel, not after flash appears.
The Bottom Line
The parting line decides flash, appearance, release, and mold cost in one stroke. A wrong split costs $4,000-plus in rework and days of schedule. Place the line on the contour, keep lands at 3-5 mm, and angle every shut-off. Check it in DFM before you cut steel.
DieStrike builds precision molds under IATF 16949 with 24-hour DFM feedback and 2-4 week injection mold lead times. Send your part model through the injection mold manufacturing line and get the parting line review before the RFQ is locked.
KEEP READING
Related Reading
Mold Core vs Cavity: Roles and Machining Strategy
Split the tool along the parting line: core-side vs cavity-side machining, steel, and cooling that decide fit and part release.
Read articleArticle9 Draft Angle Mistakes That Kill Moldability
Draft below 0.5 degrees drags on shut-off walls and galling follows. Angle rules that protect the parting line and the part.
Read articleArticleHow to Design Undercuts for Automotive Parts
Parting line logic for side actions: slides and lifters cost $3,000-$15,000 per side, and every shut-off face needs an angle rule.
Read articleArticleMold Venting: Depth, Location and Design Rules
Vent depths of 0.01-0.05 mm by resin, land widths of 1-3 mm, and placement rules that stop burns and short shots at last-fill points.
Read articleNEXT STEP
Ready to Start Your Mold?
Send us your element dimensions or part numbers — our team responds within 24 hours with pricing and lead time.

Written by
Ray ChanMold Buyer's Guide Author · Precision Mold Manufacturing Specialist. Ray helps global importers, distributors and OEMs source factory-direct molds and mold parts.