
Servo Press vs Mechanical Press: What Changes in the Die
Table of Contents
A 200 t crank press delivered 132 t at 1 mm above bottom dead centre. The part was a 2.4 mm HSLA bracket, and the flange sprang back 1.8 mm outside the print. The tool maker added 0.6 mm of over-bend and three shims. The die still ran 14 days late, and the first 4,000 parts needed a manual restrike.
This guide compares the two drives on tonnage window, stroke programmability, dwell, forming speed, blanking shock, energy, capex and die-side consequences.
The Snapshot
- Full tonnage in a 3 to 6 mm band. A crank press reaches its rating only just above bottom dead centre, while a servo holds 30 to 100 percent of rated force across most of the stroke.
- Springback cut 30 to 60 percent. A 0.2 to 0.5 s dwell at bottom dead centre lets the flange stress-relax, which removes over-bend and shim work on AHSS parts.
- 25 to 60 spm against 200 to 800 spm. A servo press trades stroke rate for motion control, so simple high-volume blanking still favours a mechanical crank drive.
- 30 to 60 percent more capex, 20 to 30 percent less energy. A direct-drive servo costs more up front and saves energy per part because there is no flywheel and no clutch.
How a Crank Press Delivers Force
A mechanical press turns a motor and a flywheel into one fixed sine stroke. Slide travel runs 40 to 150 mm on a 110 to 400 t machine, and slide velocity peaks near mid-stroke at 300 to 600 mm/s. At bottom dead centre the velocity falls to zero, and the mechanical advantage available to the ram falls with it.
The force curve is the real constraint on the die. A crank press reaches rated tonnage only in a narrow band above bottom dead centre. Full force lands at 3 to 6 mm, and half force lands around 10 to 15 mm of slide position. Ask a 200 t crank press for 200 t at 1 mm and it will stall or deflect. The rating is a force-against-distance envelope, not a flat ceiling.

Three die decisions follow from that envelope. The first is how far a draw can run before the cushion and the punch run out of usable force. The second is the tonnage a blanking station can pull at the instant of snap-through. The third is the shut height and the stroke, because crank geometry ties stroke length to the frame.
Energy storage adds a second limit. A flywheel press banks kinetic energy between strokes. A heavy coining or embossing hit drags the flywheel speed down, and the press needs 2 to 5 revolutions to recover. On a 300 t press that recovery takes 1.5 to 4 s. The recovery window caps strokes per minute well below the no-load figure.
Coining is the clearest example. Coining a 1.5 mm brass terminal needs 3 to 6 times the force of the same flange in air bending. That force develops in the last 1 to 2 mm of the stroke, inside the band where a crank press still has force to give. It explains why coining stayed on mechanical presses for so long, and why a proper tonnage calculation is the first step of any die project.
What a Servo Drive Changes in the Slide Motion
A servo press replaces the flywheel, clutch and brake with one or more servomotors. The slide is driven through a crank, a knuckle or a screw. Motion becomes a program rather than a fixed geometry.
Velocity, direction and dwell are all settable at any point in the stroke. The controller can slow the slide to 20 to 50 percent of normal speed, hold it, or reverse it before bottom dead centre. It can also dwell at bottom dead centre for 0.1 to 0.5 s without losing position.

The usable tonnage window is the number that matters to a die designer. A servo press holds 30 to 100 percent of rated force across most of the stroke instead of a 3 to 6 mm band. A 300 t machine can therefore deliver useful forming force at 40 mm of slide position, which a crank press of the same size cannot.
Four motion profiles cover most production. A sine profile matches a crank press and serves as a reference. A slow-down profile runs the last 10 to 30 mm of approach at 20 to 50 percent speed. A dwell profile holds force or position for a set time. A linked profile runs a short 5 to 20 mm working stroke at a high rate between positioning moves.
Stroke length stops being a lock on the tool. A crank press has one stroke, so the die must open far enough for the transfer or the coil feed. A servo can run 40 mm of stroke on a flat blank and 200 mm on a deep panel from the same frame. That flexibility matters when one press serves a mixed book of work.
There is a trade, and it is the one buyers miss. Motion control costs strokes per minute. A progressive die on a servo press commonly runs 25 to 60 spm against 200 to 800 spm for the same tool in a mechanical press on simple blanking. The servo wins on yield and loses on raw cycle count.
Springback and Bottom Dead Centre Dwell
Springback is elastic recovery after the punch releases the part. In a 780 to 1180 MPa AHSS flange it shows as 1 to 5 degrees of angle change. That is 1 to 3 percent of the formed dimension, and it lands outside a 0.5 mm profile tolerance on most automotive brackets.
The die maker normally answers it with over-bend, a restrike station and shims under the form block. Each of those answers costs tryout time. A flange that needs three tuning loops on a crank press is a two week delay on a die that is already past its promised date.
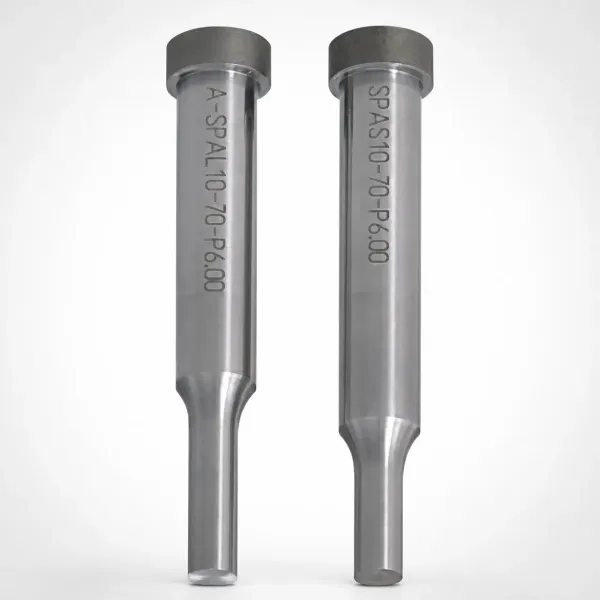
A dwell at bottom dead centre attacks the same problem from the other side. Holding the flange under full force for 0.2 to 0.5 s lets the outer fibres stress-relax while the punch is still in contact. Measured springback after a controlled dwell typically falls 30 to 60 percent against the same tool run at full speed.
That reduction changes the die, not just the process. Less springback means a smaller over-bend allowance, so fewer shim packs and less hand fitting at the tryout. A panel that needed three tuning loops on a crank press often settles in one or two on a servo press.
Dwell only pays when it is controlled by force or position. A timed dwell on a press with no slide position feedback will drift with frame deflection and oil temperature. Set the dwell on a force trigger at 90 to 100 percent of the target tonnage and log the curve for every stroke. The springback compensation rules still apply, because the material has not changed.
The trade is cycle time. A 0.3 s dwell on a 40 spm line costs about 20 percent of the cycle. On a single-hit tool that is roughly 8 strokes per minute given away, so run the dwell only on the stations that need it.
Forming Speed Control on AHSS and Deep Draws
Strain rate decides whether a deep draw tears. Running the first 10 to 30 mm of a draw at 20 to 50 percent of normal speed gives the material time to work-harden ahead of the punch. On a DP780 panel that slower approach typically buys 5 to 15 percent more draw depth before the first split appears.
The same control rescues an existing tool. A die that splits at 12 mm of draw on a crank press can often complete the draw on a servo press without touching the form radii. That is usually cheaper than a new blank shape, an extra anneal or a fourth operation in the tool.
Heat adds a third lever. In hot stamping, 22MnB5 blanks are austenitised at 900 to 950 °C. They are formed at 30 to 100 mm/s before the die quenches them at 30 to 60 °C/s. A servo press holds that forming speed through the whole stroke. A crank press cannot, because slide speed follows the sine curve, which is why hot stamping dies are built around a programmable slide.
Warm forming sits between the two. Aluminium 6xxx and 7xxx sheet formed at 200 to 300 °C tolerates a slower approach and a longer dwell. Both are program settings on a servo drive. On a mechanical press the same window has to be bought with die heaters and a slower machine rate.
Blanking Impact, Noise and Punch Shock
Blanking releases stored energy in a few milliseconds. A 200 t blanking hit can peak at 95 to 105 dB(A) at the operator position. The shock load on the punch reaches 1.5 to 3 times the static tonnage. Both numbers scale with slide velocity at the moment of break-through.
Slowing the slide before snap-through cuts both. A servo profile that drops to 10 to 30 percent of normal speed in the last 2 to 5 mm cuts noise 5 to 10 dB and shaves the shock peak. Less shock means less chipping at the punch edge and fewer cracked inserts behind the die block.

The maintenance effect shows up in the sharpening log. A D2 punch blanking 2 mm mild steel normally holds 80,000 to 150,000 hits per sharpening. Remove the shock peak and the same punch tends to reach the top of that band instead of the bottom. That is straight capacity on a fixed tool budget.
Tool steel choice still sets the floor. A die that runs 1180 MPa AHSS may need a powder metallurgy grade at HRC 60 to 64 and a coated punch, no matter how slowly the slide moves. The drive changes the load path, not the wear mechanism, so steel selection stays an independent decision.
Die Design Consequences After the Drive Changes
Shut height and stroke setting lose the crank geometry constraint. A servo controller can correct a 0.05 to 0.2 mm shut-height error without pulling the die. On a blanking die that correction used to be a shim pack under the bolster, and each change cost 20 to 40 minutes of press downtime.
Cushions and springs stay, but their setting window widens. A hydraulic cushion on a servo press can be programmed with a pressure curve against slide position, from 0 to 100 percent of its capacity. Nitrogen springs are still needed for local hold-down, and they still have to be sized on peak load rather than rated load.
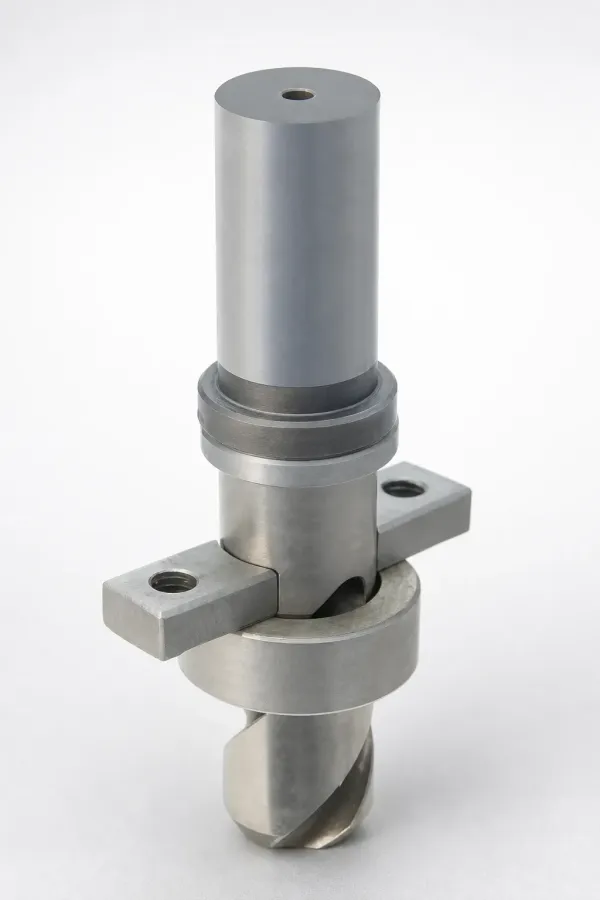
Pilot release timing becomes a setting rather than a cam. In a progressive die the pilots must clear the strip before the feed advances. That release point used to be fixed by cam and link geometry. On a servo press it is a stroke position in the recipe, so a strip material change can be absorbed without cutting new cams.
Die protection stays mandatory. Position, tonnage and strip sensors are the same hardware, but a servo press can read slide position to 0.01 mm and force per stroke. That gives the sensor logic a second data channel, and trip limits can be set on a force envelope instead of a single peak value.
Two habits have to be unlearned. A die setter who tunes a crank press by feel will over-shim a servo tool, because the press can absorb the error. A programmer who drops a sine profile into a servo controller wastes the motion control that the press was bought for.
Tonnage, Strokes Per Minute and Cycle-Count Economics
Cycle count is the first number an accountant asks for, and it favours the mechanical press on simple work. A mechanical press runs simple blanking at 200 to 800 spm. A servo press running a progressive die usually lands at 25 to 60 spm, because the useful motion profiles spend time where a crank press does not.
Yield is the second number, and it favours the servo. A servo press can run a 300 t deep draw at 45 spm with a controlled approach and a 0.3 s dwell. A crank press of the same capacity may need two operations, an anneal and a restrike to reach the same drawing depth.
The table below sets the two drives side by side on the numbers that move a die project.
| Parameter | Mechanical crank press | Servo press | Why the die cares |
|---|---|---|---|
| Stroke programmability | One fixed sine stroke, 40 to 150 mm | Programmable velocity, dwell and reverse motion | Slow approach, dwell at bottom dead centre, short working stroke |
| Tonnage window | Full force at 3 to 6 mm above bottom dead centre, half force at 10 to 15 mm | 30 to 100 percent of rated force across most of the stroke | Draw and coining stations keep usable force |
| Strokes per minute | 200 to 800 spm on simple blanking | 25 to 60 spm on progressive work with motion profiles | Cycle-count economics flip on high-volume flat parts |
| Springback control | Over-bend, restrike and shim packs | A 0.2 to 0.5 s dwell cuts springback 30 to 60 percent | Fewer tuning loops before the die is signed off |
| Energy per part | Flywheel, clutch and brake losses | Direct drive saves 20 to 30 percent, with recovery on deceleration | Lower running cost on a two or three shift line |
| Capex index | 1.0 for an equivalent tonnage | 1.3 to 1.6 for an equivalent tonnage | Paid back by first-pass yield, not by stroke rate |
| Best-fit parts | Flat blanking, simple bending, high-volume mild steel | AHSS forming, deep draws, springback-critical flanges, warm and hot forming, high-mix low-volume | Match the drive to the part, not to the press aisle |
← swipe to scroll →
Table note: ranges are typical published values for 110 to 400 t presses. Confirm the rating curve, the cushion capacity and the energy figure against the machine builder data sheet before a die is released.
The comparison holds only for the part family in the last row. A servo press does not turn a 400 spm blanking job into a 400 spm servo job. It turns a job that a mechanical press cannot hold in one pass into a single-pass job, and that is where the yield gain is booked.
Volume breaks the tie in most plants. A shop that runs 20 million flat washers a year buys a mechanical press and never looks at a servo. A shop that runs 400,000 AHSS seat structures a year buys the servo and writes the extra capex into a 2 to 4 year payback.
Cost, Energy and Maintenance
A servo press costs 30 to 60 percent more than a crank press of the same tonnage. On a 300 t machine that gap is the largest number in the business case. It has to be paid back by yield rather than speed, because the stroke rate usually falls.
Energy is where the drive claws part of it back. A direct-drive servo has no flywheel to spin and no clutch or brake to slip. It also recovers energy when the slide decelerates. Savings typically run 20 to 30 percent of energy per part against a mechanical press doing the same work.
Maintenance changes shape. A mechanical press wears clutch plates, brake linings, a flywheel bearing and a pneumatic counterbalance. A servo drive removes most of those parts, and the wear list shortens to motor bearings, slide guides and the lubrication circuit.
Payback follows part value rather than tonnage. A first-pass yield gain of 5 points on a high-value AHSS panel will carry a 2 to 4 year payback on the press premium. A 1.5 mm mild steel bracket with an open tolerance will not pay it back inside the tool life.
Retrofitting an Existing Die to a Servo Press
Most dies can move to a servo press, but the transfer is not a bolt-up job. The force envelope, the timing and the hold-down all have to be re-verified against the new motion profile before the first production stroke.
Start with the tonnage envelope. A die designed for a crank press assumes full force in the 3 to 6 mm band. A servo press delivers force across a wider window, but the die still sees peak load at the same stroke positions. Recalculate each station against the press rating curve and confirm the cushion capacity at the new dwell point.
Pilot release timing is the next item. Set the release so the pilots clear the strip before the feed advances. Confirm it with a strip-mark check over 20 strokes. A pilot that releases 0.5 mm late will drag the hole and pull a slug at the second station.
The cushion pressure curve has to be reprogrammed, not copied. A crank press cushion rises to a fixed pressure at a fixed stroke position. A servo press can ramp that pressure across the stroke, so the binder holds 80 to 100 percent of its force through the drawn depth and then releases at a set position.
Hold-down force needs a second look on thin material. A servo press can hold the same force for a longer time, which improves flatness on a 0.8 mm panel. The same setting can mark a soft or coated surface if the pressure is carried over from the old recipe.
Finally, retrain the die setter. On a crank press the crew tunes with shims, a feeler gauge and a lead hammer. On a servo press the same crew works in the controller: profile selection, force trigger, dwell time, cushion curve and trip limits. Budget a full shift of training per setter and write every recipe into the tool file, which is the specification we build to on each stamping die project.
The Selection Rule by Part Family
Simple high-volume blanking on mild steel still belongs on a mechanical crank press. Strokes per minute of 200 to 800 and a lower capex index beat motion control when the part is flat, the tolerance is open and the volume is in the millions.
AHSS forming, deep draws and springback-critical flanges belong on a servo press. The 30 to 60 percent springback reduction and the 5 to 15 percent gain in draw depth convert into first-pass yield, which is the only number that pays for the press premium.
Hot stamping sits firmly on the servo side. A 22MnB5 panel needs a controlled form speed through the whole stroke and a quench that starts at a set position. Both are program settings on a servo drive, and neither is available from a sine curve.
High-mix, low-volume work also favours the servo. A shop that runs 20 different brackets a month changes the stroke, the speed and the dwell per part in the controller. On a mechanical press the same change costs setup time at the die and a longer trial.
Warm forming and aluminium panels sit in the middle. Forming at 200 to 300 °C benefits from a slow approach and a longer dwell, but the tool still has to be designed for the temperature and the die surface still has to resist pick-up.
The largest application is automotive structure and body work. Those parts combine AHSS, tight flanges and high annual volume, and that is the mix a servo-driven line serves best. The automotive stamping work we build follows the same pattern, with EV battery trays and motor housings joining the list.
The Bottom Line
Drive choice comes down to four numbers. Full tonnage in a 3 to 6 mm band or across most of the stroke. 200 to 800 spm or 25 to 60 spm. A fixed stroke or a programmable profile. Shim tuning or a force-controlled dwell.
A mechanical crank press still wins flat, high-volume blanking on mild steel, where speed and capex decide the job. A servo press wins AHSS forming, deep draws, springback-critical flanges, warm and hot forming, and high-mix work, where first-pass yield decides it.
The die is where the decision lands. A servo-capable tool needs programmable pilot release, a cushion pressure curve, a verified force envelope and a setter who works in the controller rather than with shims.
DieStrike builds stamping dies and precision tooling to IATF 16949, with a mold tolerance of ±0.005 mm and ±0.002 mm on EDM and jig grinding, cavity hardness up to HRC 62, 120+ machines and tier-1 references including TE, Amphenol, Luxshare and Dongshan. Tool lead times run 2 to 5 weeks, and standard components ship in 3 to 7 days. Send the part print and the press data, and we will return a die concept that matches the drive you run.
KEEP READING
Related Reading
How to Design a Progressive Die Layout
Station sequence, pilot release timing and scrap removal rules for a multi-station tool.
Read articleArticleAir Bending vs Coining vs Bottom Die
Three bending methods ranked by force, springback control and the tooling each one needs.
Read articleArticleDie Protection Sensors in Progressive Dies
Sensor types, placement and trip limits that stop a press before the die takes damage.
Read articleServiceStamping Die Manufacturing
IATF 16949 die building with 0.005 mm tool accuracy, 120+ machines and 2 to 5 week lead times.
Read articleNEXT STEP
Ready to Start Your Mold?
Send us your element dimensions or part numbers — our team responds within 24 hours with pricing and lead time.

Written by
Ray ChanMold Buyer's Guide Author · Precision Mold Manufacturing Specialist. Ray helps global importers, distributors and OEMs source factory-direct molds and mold parts.