
D2 vs DC53 vs PM Tool Steel: Choosing a Stamping Die Steel
Table of Contents
A progressive die cutting a 2 mm mild steel bracket ran a D2 punch at HRC 60 and lost its edge after 96,000 hits. The toolroom pulled the die for sharpening twice a week, and a 500,000 piece order absorbed about 42 hours of unplanned press downtime. Nothing was out of print; the grade was simply wrong for the duty. This article compares D2, DC53 and powder metallurgy cold-work steel on carbide size, toughness, hardness, tempering window, sharpening interval, EDM damage, coating and cost.
Every figure below is a typical published or shop value for cold-work die steel, and each one needs checking against the mill certificate and the heat treatment report.
The Snapshot
- Carbide size sets the ranking. D2 carries eutectic carbide bands 10 to 25 micron wide, DC53 refines that structure into finer and more even particles, and a PM grade holds every carbide under 3 micron.
- Transverse Charpy toughness runs 15 to 25 J on D2, 30 to 45 J on DC53 and 60 to 90 J on a PM grade. The bar is cut across the rolling direction, where a punch corner bends and chips.
- Sharpening interval on 2 mm mild steel runs 80,000 to 150,000 hits on a D2 punch against 300,000 to 600,000 on a PM punch. Above 800 MPa sheet both numbers fall 3 to 5 times and the ranking stays the same.
- Cost index runs 1.0 for D2, 1.3 to 1.6 for DC53 and 3 to 6 for a PM grade. The break points sit near 200,000 pieces for D2 and 1,000,000 pieces for DC53, or for PM with a tight burr limit.
The Three Cold-Work Families on One Axis
D2, or 1.2379, is the reference cold-work grade. It carries about 12 percent chromium and 1.5 percent carbon, hardens in air or in a gas quench, and settles at HRC 58 to 62 after tempering. The carbon and chromium form eutectic carbide bands 10 to 25 micron wide while the ingot solidifies, and rolling turns those bands into stringers along the rolling direction.
DC53 is a modified D2 with roughly 8 percent chromium and a rebalanced carbon, molybdenum and vanadium content. At the same hardness DC53 delivers 1.5 to 2 times the transverse toughness of D2, which is why it holds a punch corner that D2 chips.
A powder metallurgy grade such as CPM 3V or ASP 2023 is gas atomized, so every carbide sits under 3 micron and the distribution is uniform in all three directions.
| Family | Typical composition | Working hardness | Carbide structure | Transverse toughness | Cost index |
|---|---|---|---|---|---|
| D2 / 1.2379 | 12 percent Cr, 1.5 percent C, air hardening | HRC 58 to 62 | Eutectic bands 10 to 25 micron | 15 to 25 J, the reference | 1.0 |
| DC53 | 8 percent Cr modified D2 with Mo and V | HRC 60 to 63 | Finer and more even, 3 to 8 micron | 30 to 45 J, 1.5 to 2 times D2 | 1.3 to 1.6 |
| PM cold-work, CPM 3V or ASP 2023 | Gas atomized, high V and Mo | HRC 60 to 64 | Under 3 micron, uniform in all directions | 60 to 90 J, 2 to 3 times D2 | 3 to 6 |
← swipe to scroll →
Table note: composition, hardness and toughness figures are typical published values for cold-work die steel. Confirm the mill certificate, the carbide rating and the heat treatment report before the die drawing is released.
The structure difference shows up on the shop floor before it shows up in a wear test. D2 polishes to Ra 0.1 to 0.2 micron with effort, because the carbide bands tear out and leave 1 to 2 micron pits. DC53 and PM grades polish faster and hold a finer face, which matters on a punch that runs stainless sheet.

Supply is part of the plan. D2 is stocked in every steel service centre, DC53 usually ships in 3 to 7 days, and a PM grade is mill ordered and can take 2 to 5 weeks. The 12 steel grades comparison covers the hot-work and stainless families.
Toughness and Wear: The Numbers That Rank Them
Impact toughness is measured on a Charpy bar cut transverse to the rolling direction, because that is how a punch edge sees the load. On that bar D2 lands at 15 to 25 J, DC53 at 30 to 45 J, and a PM cold-work grade at 60 to 90 J.
Wear runs on a different mechanism, driven by carbide volume and carbide hardness rather than bulk hardness. D2 carries a large carbide fraction and resists sliding wear. DC53 gives up a little wear volume to the finer structure. PM grades match or beat D2 on abrasive wear, because their vanadium carbides are harder.

Bending fatigue matters more than the Charpy figure on a forming station. A form punch flexes 0.05 to 0.3 mm every stroke, and a face at HRC 62 with a 0.02 mm grinding scratch will start a crack at 200,000 to 400,000 hits. DC53 and PM grades tolerate that scratch regime better, because a crack has to cross fine carbides instead of following a 25 micron band. The burr side of the same decision sits in blanking die design.
Hardness does not scale upward forever. D2 tops out near HRC 62, DC53 near HRC 63, and PM grades near HRC 64 for cold-work duty. Push any of the three 2 points higher and toughness falls faster than wear resistance gains, A purchase order that asks for HRC 66 on a punch is asking for chips at 20,000 hits. The rest are catalogued in the 9 mold steel selection errors.
Heat Treatment and the Tempering Window
D2 austenitizes around 1,010 to 1,040 °C and hardens in air or in a vacuum furnace with a 4 to 6 bar gas quench. Tempering runs 1 to 2 hours at 180 to 230 °C, once or twice, leaving HRC 58 to 62. Do not temper a cold-work D2 part above 250 °C, because hardness drops without a toughness gain.
DC53 takes a higher austenitizing temperature near 1,030 to 1,050 °C and then a secondary hardening temper at 500 to 530 °C, usually two draws of 2 hours each. That treatment lands it at HRC 60 to 63 with the toughness advantage intact. The high temper is also why a DC53 die absorbs a wire EDM recast layer and a coating cycle that would soften a low tempered D2 part.
PM cold-work grades austenitize at 1,050 to 1,120 °C, quench in vacuum gas, and temper twice or three times at 500 to 550 °C to reach HRC 60 to 64. Finer segregation means less quench distortion, up to 0.02 to 0.05 mm less movement on a long punch than D2.
Plan the finish grind after heat treatment on every punch and die insert. Keep 0.10 to 0.30 mm of grinding stock, at the small end for a PM grade. Stress relieve at 600 to 650 °C for 1 to 2 hours before the finish cut, or a 300 mm punch bows by 0.05 mm after hardening.
Sharpening Interval and Die Life by Sheet
A sharpening interval is a shop number, not a datasheet number, because it moves with clearance, coating, lubrication and press condition. On a 2 mm mild steel blank at 7 percent clearance per side, a D2 punch at HRC 60 holds 80,000 to 150,000 hits per sharpening. The same punch in DC53 reaches 150,000 to 250,000 hits, and a PM punch runs 300,000 to 600,000.
Change the sheet and every number falls together. On AHSS above 800 MPa the interval drops 3 to 5 times: D2 to 20,000 to 50,000 hits, DC53 to 40,000 to 80,000, and PM to 80,000 to 180,000. The ranking survives the change.
Stainless 304 at 520 to 700 MPa adds work hardening and adhesive wear. It builds a cold weld on the punch face, so the interval depends as much on coating and lubrication as on the substrate. A TiCN coated PM punch on 1.5 mm 304 runs 3 to 5 times the interval of an uncoated D2 punch.
| Sheet condition | D2 punch at HRC 60 | DC53 punch at HRC 62 | PM punch at HRC 62 |
|---|---|---|---|
| 2 mm mild steel, 7 percent clearance | 80,000 to 150,000 hits | 150,000 to 250,000 hits | 300,000 to 600,000 hits |
| 2 mm galvanized steel | 60,000 to 120,000 hits | 120,000 to 200,000 hits | 250,000 to 450,000 hits |
| 1.5 mm stainless 304 | 25,000 to 50,000 hits | 50,000 to 90,000 hits | 120,000 to 250,000 hits |
| 2 mm AHSS at 780 MPa | 20,000 to 50,000 hits | 40,000 to 80,000 hits | 80,000 to 180,000 hits |
| 2 mm AHSS above 980 MPa | 12,000 to 30,000 hits | 25,000 to 50,000 hits | 50,000 to 120,000 hits |
← swipe to scroll →
Table note: intervals are shop values for a single stroke blanking station at 7 to 10 percent clearance per side and a 0.10 mm burr limit. Confirm against your own hit log, because press condition and lubrication move these numbers by 20 to 30 percent.
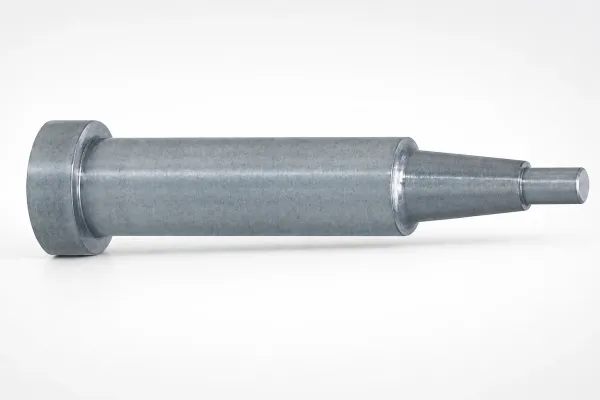
Regrind depth is part of the interval arithmetic. A typical sharpening removes 0.10 to 0.25 mm from a punch face, and every removal eats usable life. Trigger the pull on the entry radius: measure it every 5,000 hits and grind when the radius passes 0.20 mm, or when the burr passes 5 percent of sheet thickness. The punch clearance routine tracks the clearance behind that radius.
Wire EDM, Grinding and Surface Integrity
Wire EDM cuts any of the three families to ±0.002 mm on a punch profile, which is why most stamping punches and die inserts are wire cut rather than milled. The cut leaves a recast layer, and its thickness is set by the carbide structure. On D2 the coarse carbide bands produce a 1 to 3 micron recast layer along with micro-cracks under it. DC53 and PM grades leave a thinner, more even layer because their carbides are small and evenly spaced.
Remove the damage before the die runs. Two or three trim passes bring the recast layer under 1 micron, and a 5 to 10 micron polish pass removes what is left. Take a D2 punch face to Ra 0.1 to 0.2 micron, and a PM punch to Ra 0.05 to 0.1 micron.
Re-temper after wire EDM. A D2 part that comes off the wire machine carries surface stress, and a first hit shock will open that stress into a crack. Bake the part at 30 to 50 °C below the last tempering temperature for 1 to 2 hours.
Grinding follows the same logic. A D2 face ground with a wheel that is too hard burns and re-hardens in spots, and those spots chip at 10,000 to 30,000 hits. Use a softer wheel, hold the down feed at 0.01 to 0.02 mm, flood the cut with coolant and dress the wheel before the finish pass.
Coating and Surface Treatment
A PVD coating of TiCN or AlTiN at 2 to 4 micron is the standard upgrade on a cold-work punch. The coating goes on at a substrate hardness of HRC 62 to 64, and its job is to cut adhesive wear and galling. That matters most on stainless, aluminium and galvanized sheet, where the punch face would otherwise pick up material. The coating temperature stays under 500 °C, so a tempered part keeps its hardness.
Nitriding is a different tool for a different failure. A nitrided layer of 0.05 to 0.12 mm raises face hardness and adds a release layer, and it belongs on draw and form radii where sliding contact rules the wear. A nitrided punch also needs a diffusion zone deeper than the compound layer, or the hard skin cracks away under repeated shock. Never nitride a punch that is already marginally tough on a coin station.
Match the coating to the failure mode. Adhesive pick-up responds to TiCN and to a face polished at Ra 0.1 micron or better. Abrasive wear responds to AlTiN or to a PM substrate. Chipping on a corner is a toughness problem, and the fix is DC53 or a PM grade rather than a harder layer.
Re-coat on a counted schedule. A TiCN layer on a punch running stainless wears through in 150,000 to 400,000 hits, and a half worn coating wears faster than none because the exposed substrate becomes the wear path.
Blanking, Piercing and Forming Duties
Read the duty, not the die, when you pick the grade. A blanking station cuts on the die opening edge, so burr control is set by clearance and the punch carries a compressive and bending load. Piercing reverses the fit and puts the wear on the punch, which is why the punch in a high volume pierce die takes the better steel and the die insert takes the tougher one.
Forming and coining load the tool in a different way. A coin station runs at 800 to 1,500 MPa of contact pressure, and a form radius flexes with every stroke. Those stations want toughness first, which points to DC53 or a PM grade.
Mixed-duty progressive dies are where the three families earn their place together. It is normal to build blanking and piercing punches from D2 or DC53, form and coin inserts from DC53 or PM, and pilots, wear plates and guide bushings from a case hardened or nitrided steel. Record the grade and hardness of every replaceable part on the drawing set, so a spares order matches the original. Grade selection and clearance planning sit inside stamping die manufacturing.
Volume, Index Cost and the Real Economics
Steel price is the smallest part of the decision. Measured against D2 at an index of 1.0, DC53 lands at 1.3 to 1.6 and a PM grade at 3 to 6.
Value the downtime before the steel. One sharpening event on a progressive die costs 6 to 10 hours of press time when you count the pull, the strip, the regrind, the re-set and the first article approval. On a 500,000 piece order that needs six D2 sharpening events against two PM events, the four events you do not run are the whole business case for the PM premium on the punches.
A D2 die is 30 to 40 percent cheaper to build than a PM die on the same part. Below 200,000 pieces a year the D2 die wins on cash, because the sharpening events fit inside planned maintenance windows. That advantage is real on a short program, a prototype tool or a second source die.
Above 500,000 pieces the arithmetic turns. Sharpening downtime, scrap after each grind and the risk of a chipped punch on a hot order all scale with the number of events, not with the price of the steel.
The Decision Table: Tensile, Thickness, Volume and Tolerance
Four inputs decide the grade: sheet tensile strength, thickness, annual volume and the burr or flatness tolerance. Read them together, because a thin AHSS part at high volume sits in a different row than a thick mild steel part at low volume.
| Sheet and tensile | Thickness | Annual volume | Grade and reason |
|---|---|---|---|
| Mild steel under 400 MPa | 0.5 to 3 mm | Under 200,000 pieces | D2 at HRC 58 to 62: lowest index and enough interval for the volume |
| Mild steel under 400 MPa | 0.5 to 3 mm | 200,000 to 1,000,000 pieces | DC53 at HRC 60 to 63: 1.5 to 2 times the toughness and a longer interval |
| Galvanized or coated steel | 0.5 to 2 mm | Above 300,000 pieces | DC53 with TiCN: the coating carries the adhesive wear off the punch face |
| Stainless 304 and 430 | 0.5 to 2 mm | Above 200,000 pieces | PM grade with TiCN or AlTiN at 2 to 4 micron on a polished face |
| AHSS 590 to 780 MPa | 0.8 to 2.5 mm | Above 100,000 pieces | DC53 minimum, PM where the burr limit is tight or the sheet is abrasive |
| AHSS above 980 MPa | 0.8 to 2 mm | Above 100,000 pieces | PM grade at HRC 62 to 64 with AlTiN: the shock load rules this row |
| Burr or flatness tolerance under 0.02 mm | Any | Any volume | PM grade: the uniform structure holds clearance in every direction of the cut |
← swipe to scroll →
Table note: rows are a starting point for a grade decision, not a substitute for a tryout. Confirm the actual tensile strength range, the coating weight and the burr limit on the part print, then run a first article at the selected clearance before the full order is released.
The honest rule is short. Below 200,000 pieces and 400 MPa, use D2. Between 200,000 and 1,000,000 pieces, or on coated and AHSS sheet above 100,000 pieces at any volume, use DC53. Above 1,000,000 pieces, or whenever the burr limit is under 0.02 mm or the sheet is abrasive, use a PM grade.
Selection Errors That Retire a Die Early
Buying on the price index alone. The steel is 5 to 15 percent of a completed die, and the sharpening events it causes dominate the cost of ownership.
Running D2 on AHSS above 800 MPa. The interval falls to 20,000 to 50,000 hits per sharpening, and a chipped punch on a hot order costs more than the grade upgrade. Move that station to DC53 as a minimum and to PM where the burr limit is tight.
Skipping the re-temper after wire EDM. A 1 to 3 micron recast layer on D2 carries micro-cracks, and a first hit under shock opens them into a chip. Bake at 30 to 50 °C below the last temper for 1 to 2 hours and the problem disappears.
Over-specifying hardness. D2 tops out at HRC 62 and a PM grade at HRC 64 for cold-work duty. A drawing that calls for HRC 66 buys chipping at 20,000 hits and a rework cycle that no wear gain can repay.
Ignoring the carbide direction. D2 stringers run along the rolling direction, so a punch profile that crosses the bands at right angles behaves differently from one that runs with them.
Coating a toughness problem. A 2 to 4 micron PVD layer reduces friction and adhesive wear, and it cannot stop a corner that chips because the substrate is too brittle. Fix the substrate first, then coat it.

Log the grade, the hardness, the coating and the hit count at every sharpening in the tool file. After two campaigns the shop has its own interval data, which beats every published table.
D2 vs DC53 vs PM Tool Steel FAQ
Q1. Is DC53 simply a better D2?
It is a modified D2 with about 8 percent chromium instead of 12 percent, and a finer carbide distribution. At the same hardness it gives 1.5 to 2 times the transverse toughness, so it resists chipping better while holding comparable wear resistance. It is not universally better: D2 costs less, grinds with a standard wheel and remains the correct choice on mild steel below 200,000 pieces.
Q2. When does a PM tool steel pay for itself?
Above 1,000,000 pieces, whenever the burr limit is under 0.02 mm, or on high strength sheet above 800 MPa. A PM punch runs 300,000 to 600,000 hits per sharpening on 2 mm mild steel against 80,000 to 150,000 for D2, so the events it removes usually cover its 3 to 6 index premium.
Q3. What hardness should a D2 punching die be?
HRC 58 to 62 for a punch, delivered by a 1 to 2 hour temper at 180 to 230 °C after austenitizing at 1,010 to 1,040 °C. The die insert in the same station usually runs 1 to 2 points harder at HRC 60 to 62, because the opening edge carries the burr and the wear.
Q4. Can I mix grades in one progressive die?
Yes, and most high volume tools do. Blanking and piercing punches from D2 or DC53, form and coin inserts from DC53 or PM, and pilots, wear plates and guide bushings from a case hardened or nitrided steel.
The Bottom Line
A cold-work die steel decision is three numbers held together: hardness from HRC 58 to 64, transverse toughness from 15 to 90 J, and a sharpening interval from 80,000 hits on D2 to 600,000 on PM in mild steel. D2 carries the low volume, low tensile work at the lowest index. DC53 buys 1.5 to 2 times the toughness for a 1.3 to 1.6 index and covers the 200,000 to 1,000,000 piece band. A PM grade holds the tightest burr limits and the abrasive sheet above 1,000,000 pieces.
DieStrike builds stamping dies and precision tooling to IATF 16949 with ±0.005 mm die accuracy and ±0.002 mm on EDM and jig grinding, HRC 62 maximum edge hardness and 120+ machines. Tier-1 references include TE, Amphenol, Luxshare and Dongshan. Standard components ship in 3 to 7 days and complete tool lead times run 2 to 5 weeks, with the grade recommendation and the clearance plan issued before the steel is ordered.
KEEP READING
Related Reading
Mold Nitriding vs PVD Coatings
Where a diffusion layer beats a 3 micron PVD film, and where it cracks under repeated shock.
Read articleArticleHow to Maintain Punch Clearance in Progressive Dies
Clearance drift, entry radius and the hit count that tells you when to pull the die.
Read articleArticle9 Mold Steel Selection Errors
The grade decisions that retire a tool early, from hardness targets to carbide direction.
Read articleServiceStamping Die Manufacturing
IATF 16949 die building with grade selection, HRC 62 max edges and 2 to 5 week lead times.
Read articleNEXT STEP
Ready to Start Your Mold?
Send us your element dimensions or part numbers — our team responds within 24 hours with pricing and lead time.

Written by
Ray ChanMold Buyer's Guide Author · Precision Mold Manufacturing Specialist. Ray helps global importers, distributors and OEMs source factory-direct molds and mold parts.